Working Principle and Features of Sodium Hypochlorite Powder Conveying Equipment
Release time:2026-09-17 14:01:21
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Sodium hypochlorite is a critical chemical used across multiple industrial sectors, including water treatment, disinfection, and bleaching processes. The efficient and safe handling of this powder form is essential for maintaining operational efficiency and ensuring product integrity. This article delves into the working principle and key features of specialized sodium hypochlorite powder conveying equipment, offering insights into how these systems enhance industrial workflows and address the unique challenges associated with transporting this reactive chemical.
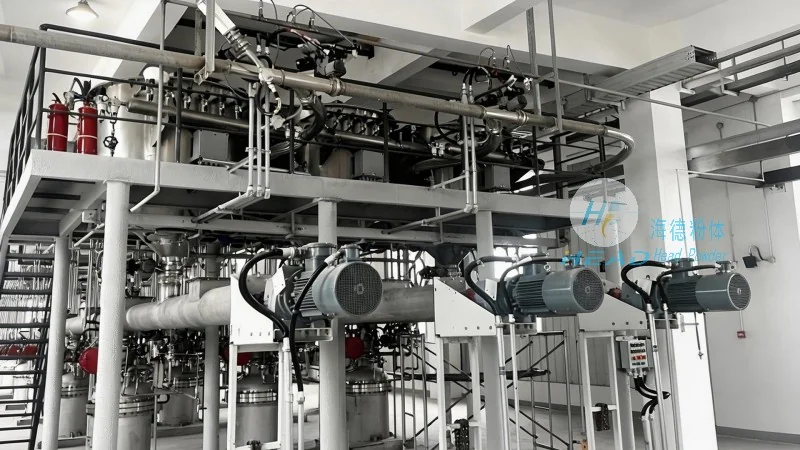
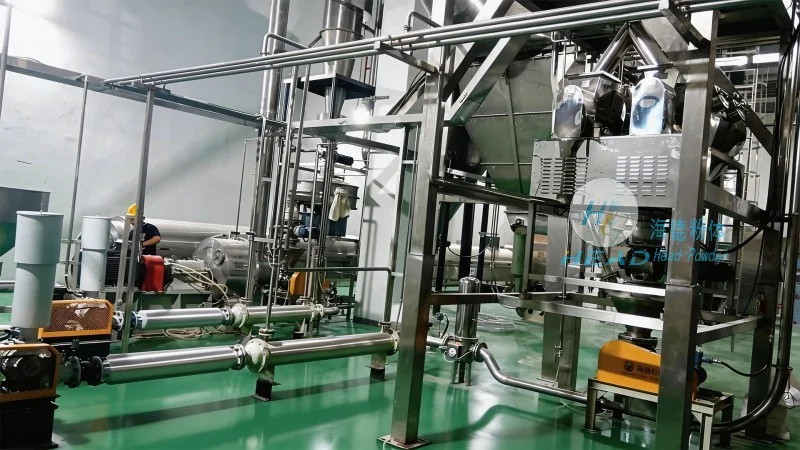
Working Principle of Sodium Hypochlorite Powder Conveying Equipment
The operation of sodium hypochlorite powder conveying equipment is based on mechanical or pneumatic systems engineered to handle the material's properties. Many systems utilize a screw conveyor mechanism, where a rotating helical screw pushes the powder forward through a sealed tube. This design minimizes dust generation and prevents contamination, which is vital given sodium hypochlorite's reactivity and potential health hazards. Other configurations may incorporate airlock valves and pressure vessels to regulate flow and ensure consistent feed rates. The working principle also involves precise control of environmental factors like temperature and humidity within the conveying path, as these variables can affect the stability and effectiveness of the chemical if it were to undergo unintended reactions during transport.
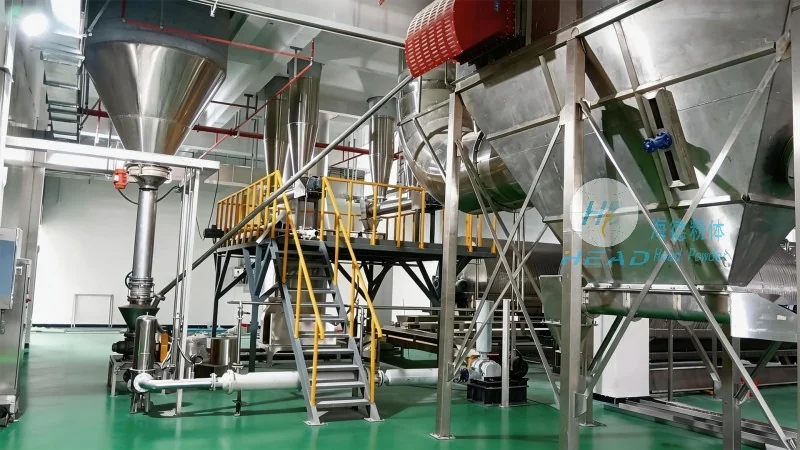
Key Features of Sodium Hypochlorite Powder Conveying Equipment
The equipment designed for sodium hypochlorite powder transport is distinguished by several key attributes that address the material's specific handling requirements. Firstly, it is constructed from corrosion-resistant materials such as stainless steel or specialized alloys to withstand the aggressive nature of sodium hypochlorite and extend service life. This ensures durability and reduces long-term maintenance costs. Secondly, the system incorporates advanced sealing and dust control technologies, including double-flap valves and air filtration units, to maintain a safe working environment and comply with environmental regulations. Thirdly, the equipment is equipped with real-time monitoring and control systems, allowing operators to adjust parameters like speed and pressure dynamically. This enhances operational flexibility and enables quick responses to production changes. Additionally, safety features such as emergency shut-off valves and leak detection sensors are integrated to minimize risks and protect personnel. The design also adheres to industry standards for chemical handling, ensuring compliance with OSHA and local environmental guidelines.
Company Information
HeadPowder, a prominent manufacturer in the industry, specializes in the design and production of high-quality sodium hypochlorite powder conveying equipment. Headquartered in Shandong, China, the company has established a reputation for delivering reliable and efficient solutions tailored to diverse industrial needs. Shandong HeadPowder Engineering Co., Ltd. leverages advanced engineering and manufacturing capabilities to produce equipment that meets rigorous performance standards. The company's commitment to quality and innovation has enabled it to serve clients globally, providing customized solutions that enhance productivity and safety in chemical processing operations.




