Anhydrous sodium sulfate, also known as anhydrous sodium sulfate, is a white crystalline powder widely used in industrial applications such as glass manufacturing, papermaking, and chemical synthesis. The efficient and safe transportation of this powder is crucial for industrial operations, and specialized conveying lines are designed to meet these requirements. This article explores the concept of an anhydrous sodium sulfate powder conveying line and delves into its fundamental design principles, highlighting the key components and operational aspects that ensure reliable material handling.
Introduction to Anhydrous Sodium Sulfate and Its Conveying Needs
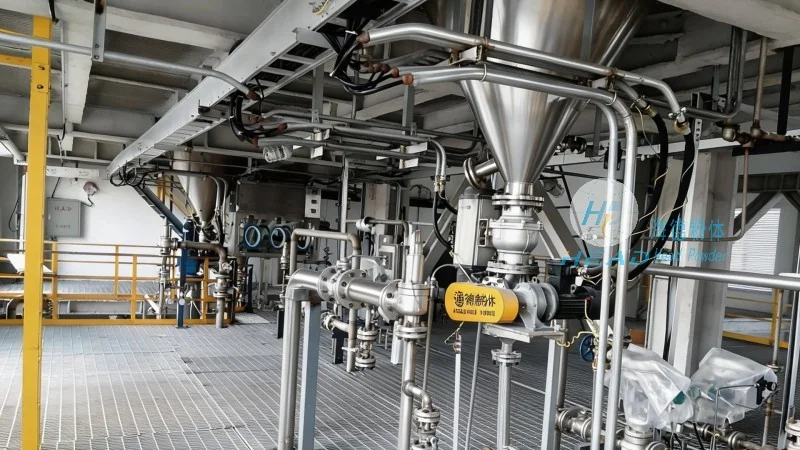
Anhydrous sodium sulfate (Na₂SO₄) is a chemical compound that plays a vital role in various industrial processes. Its fine powder form requires specialized equipment to transport without degradation or loss. Traditional methods like manual handling or simple bucket elevators are often insufficient for large-scale operations, leading to the development of dedicated powder conveying systems. These systems are engineered to maintain the integrity of the material while ensuring efficient movement from storage to processing units.
About HeadPowder: A Leading Provider of Powder Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in Shandong, China, specializing in the design, manufacturing, and installation of advanced powder handling equipment. With years of experience in the industry, HeadPowder has developed expertise in creating customized conveying solutions tailored to the unique needs of clients. The company's commitment to quality and innovation has positioned it as a trusted partner for businesses requiring reliable and efficient powder transportation systems.
Design Principles of Anhydrous Sodium Sulfate Powder Conveying Lines
The design of an anhydrous sodium sulfate powder conveying line involves several critical principles aimed at optimizing performance, safety, and material integrity. Key considerations include material properties, system layout, and operational efficiency. The following components are typically integrated into such a system:
1. Storage and Feeding Systems
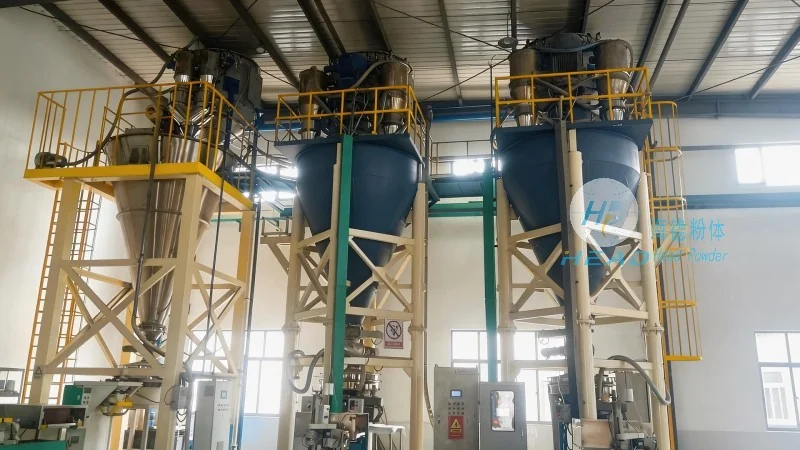
The conveying line begins with a storage hopper or silo designed to hold the anhydrous sodium sulfate powder. This storage unit is equipped with a feeding mechanism, such as a rotary valve or a screw feeder, which controls the flow rate of the material into the conveyor. Proper sealing and dust control are essential to prevent contamination and ensure safe operation.
2. Conveying Equipment
The core of the system is the conveying equipment, which may include pneumatic conveyors, screw conveyors, or bucket elevators, depending on the specific requirements. For anhydrous sodium sulfate, which is a fine powder, pneumatic conveying systems are often preferred due to their ability to handle low-density materials efficiently. These systems use air pressure to transport the powder through a pipeline, minimizing material degradation and ensuring consistent flow.
3. Ductwork and Airflow Management
Effective ductwork design is crucial for maintaining the integrity of the powder during transport. The pipeline is constructed from materials resistant to corrosion and abrasion, such as stainless steel or special polymers, to prevent material buildup and ensure durability. Airflow management systems, including filters and cyclones, are integrated to separate any entrained dust and maintain a clean environment.
4. Control and Monitoring Systems
Advanced control systems are incorporated to regulate the operation of the conveying line. Sensors and monitoring devices track parameters such as flow rate, pressure, and temperature, providing real-time data to operators. This allows for immediate adjustments to maintain optimal performance and prevent system failures.
Key Considerations in Designing the System
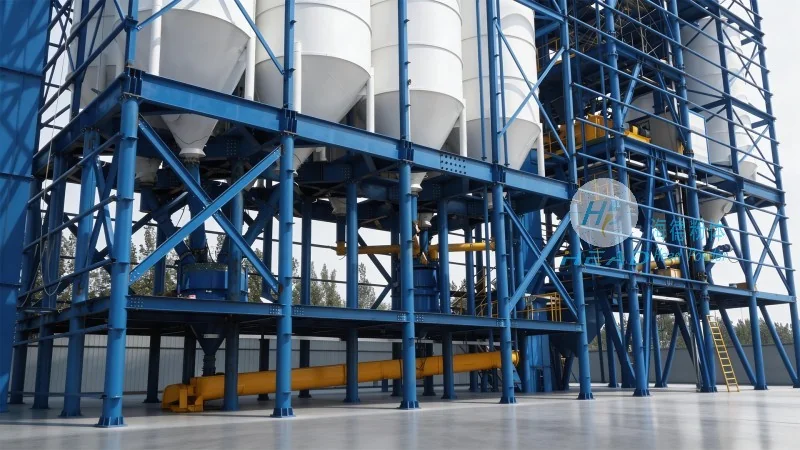
When designing an anhydrous sodium sulfate powder conveying line, several factors must be carefully evaluated to ensure the system meets operational requirements. These include the material's particle size distribution, moisture content, and flow characteristics. The system must also account for the potential for caking or agglomeration, which can affect conveying efficiency. Additionally, safety measures, such as explosion-proof designs and dust suppression systems, are critical to prevent accidents in industrial settings.
Applications and Benefits of the Conveying Line
Anhydrous sodium sulfate powder conveying lines are widely used in various industries, including chemical manufacturing, glass production, and paper processing. The benefits of these systems include improved productivity, reduced labor costs, and enhanced safety. By automating the material handling process, businesses can achieve consistent and reliable operation, minimizing downtime and material loss.
Conclusion
An anhydrous sodium sulfate powder conveying line is a sophisticated system designed to efficiently transport this critical chemical compound. The design principles, incorporating advanced components and control systems, ensure the material is handled safely and effectively. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can implement customized solutions that meet their specific operational needs, enhancing overall productivity and operational efficiency.




