Wood ash powder conveyors are specialized equipment designed for the efficient transport of wood ash, a byproduct of biomass combustion. Understanding the working principle and key features of these systems is crucial for optimizing industrial processes in sectors such as power generation, waste management, and agricultural applications. This article provides a detailed overview of how wood ash powder conveyors operate and the advantages they offer.
The Working Principle of Wood Ash Powder Conveyors
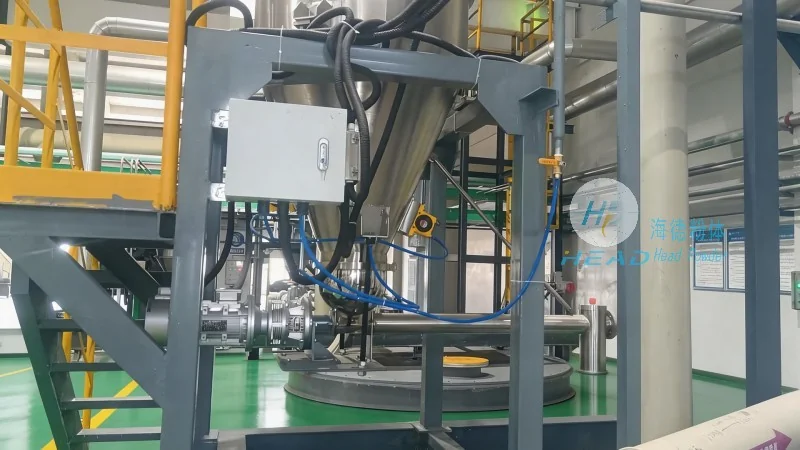
At the core of wood ash powder conveyors is a mechanism that enables the movement of fine, dry particles like wood ash from one location to another. The primary working principle involves the use of air or mechanical forces to transport the material. There are two main types of systems based on this principle: pneumatic conveyors and mechanical conveyors.
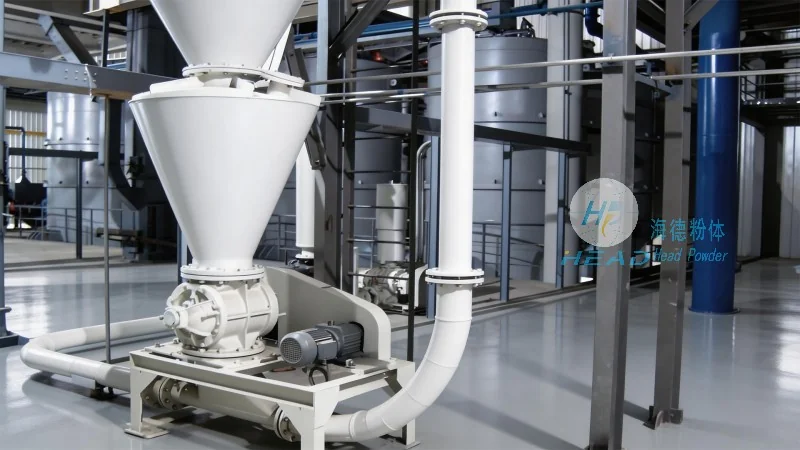
Pneumatic conveyors utilize compressed air to create a flow that carries the wood ash particles through a pipeline. The system typically includes a hopper to store the wood ash, a blower to generate the air pressure, and a receiver where the material is deposited. The air velocity and pipeline design are critical factors that determine the efficiency and capacity of the conveyor. In contrast, mechanical conveyors rely on physical components such as belts, screws, or buckets to move the material. These systems are often preferred for longer distances or when the material is more abrasive.
Key Features of Wood Ash Powder Conveyors
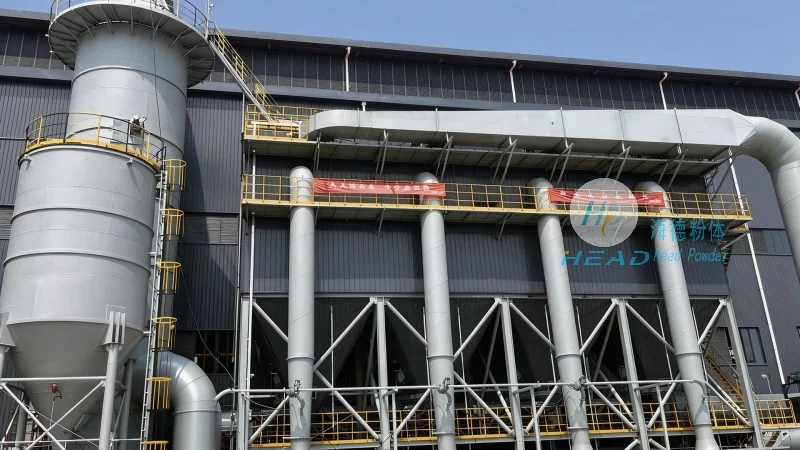
Wood ash powder conveyors are engineered with several features that enhance their performance and adaptability. One of the most notable features is their ability to handle fine, dry powders without clogging or degradation. This is achieved through the use of specialized materials for the conveyor components, such as stainless steel or corrosion-resistant alloys, which prevent material buildup and ensure durability. Another important feature is the system's scalability, allowing it to be customized for different production capacities and operational requirements. This flexibility makes wood ash powder conveyors suitable for both small-scale and large-scale industrial applications.
Efficiency is a critical feature of these conveyors, as they minimize material loss and reduce the need for manual handling. The design of the system, including the hopper and discharge mechanisms, ensures that the wood ash is transferred smoothly and consistently. Additionally, many modern wood ash powder conveyors are equipped with monitoring and control systems that allow for real-time adjustments to maintain optimal performance. This feature enhances operational reliability and reduces downtime.
Applications and Benefits in Industrial Settings
Wood ash powder conveyors find widespread use in various industrial settings due to their effectiveness in handling wood ash. In power plants, these systems are used to transport ash from boilers to storage or disposal sites, improving the overall efficiency of the combustion process. In waste management facilities, they help in the processing and recycling of biomass waste, contributing to sustainable practices. The benefits of using wood ash powder conveyors extend beyond efficiency; they also reduce labor costs associated with manual handling and minimize environmental impact by preventing dust emissions and material spillage.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized powder handling equipment. With a focus on innovation and quality, the company has developed advanced wood ash powder conveyors that meet the demands of modern industrial applications. Headpowder's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the industry. The company's headquarters is located in Shandong, China, where it continues to advance its technology and expand its product offerings to serve global markets.




