For industrial operations that require efficient and clean handling of bulk materials, dust-free bulk bag unloading and powder conveying systems are essential. These systems are designed to handle the challenges of transferring powders and granules from bulk bags without generating dust, ensuring a safe and efficient process. The following sections will explore the working principle and key features of such systems, highlighting their importance in modern industrial applications.
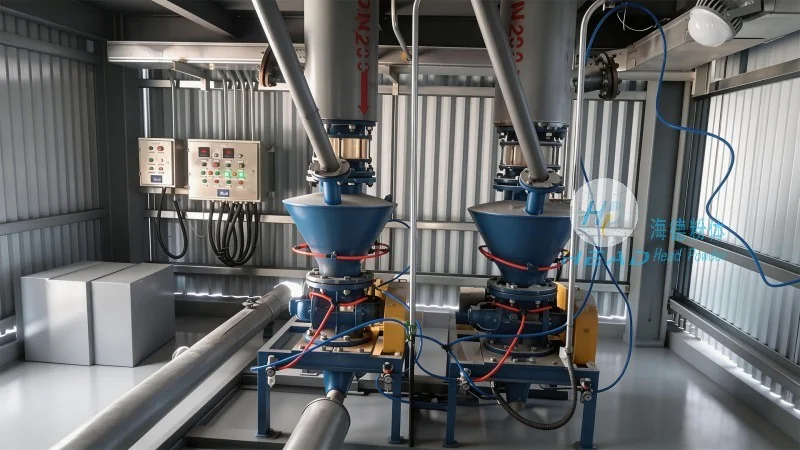
Understanding the Working Principle of Dust-Free Bulk Bag Unloading Systems
The core of a dust-free bulk bag unloading system lies in its ability to open and empty bulk bags while maintaining a sealed environment to prevent dust contamination. The process typically begins with the placement of the bulk bag onto a discharge frame or a dedicated unloader unit. The system then uses a combination of mechanical and pneumatic components to facilitate the unloading process. For instance, a typical setup may include a bag clamp that secures the bag, a discharge spout that connects to the bag's opening, and a conveyor or hopper that collects the material as it is emptied. Pneumatic actuators or motors may be employed to control the movement of the discharge spout and the opening mechanism, ensuring precise control over the flow rate. The system is engineered to minimize the exposure of the material to the air, reducing dust generation and improving safety for operators. By maintaining a closed or semi-closed environment during the unloading process, these systems help maintain the integrity of the material and comply with environmental regulations regarding dust emissions.
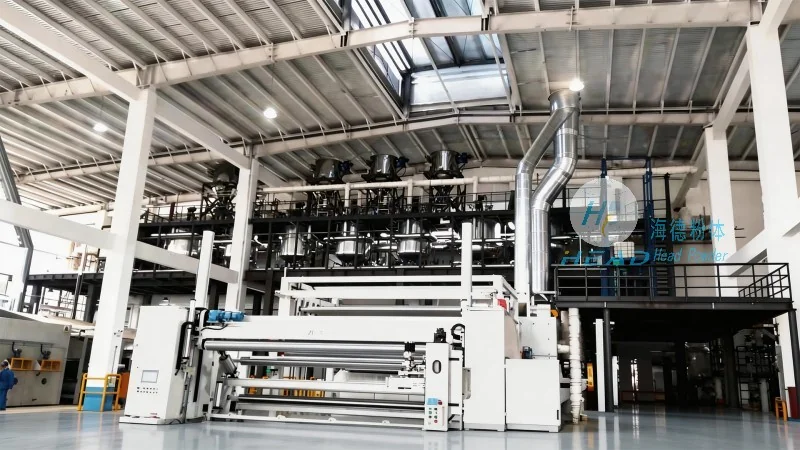
Key Features of Advanced Dust-Free Powder Conveying Solutions
Modern dust-free powder conveying systems incorporate several advanced features that enhance their performance and reliability. One of the primary features is the use of enclosed conveying lines, such as flexible hoses or rigid ducts, which prevent dust from escaping into the environment. These enclosed systems often use positive pressure or negative pressure to control the flow of material, ensuring that the material remains contained within the system. Another important feature is the integration of dust collection and filtration systems. Many advanced units are equipped with built-in filters or connections to external dust collectors, which capture any airborne particles and return them to the conveying line or safely dispose of them. This not only improves air quality but also helps maintain the purity of the conveyed material. Additionally, these systems often include adjustable flow control mechanisms, allowing operators to regulate the speed and volume of material transfer based on specific process requirements. This flexibility is crucial for applications where precise material handling is necessary, such as in pharmaceutical, food, or chemical industries. The design of these systems also emphasizes durability and ease of maintenance, with components that are resistant to corrosion and wear from the conveyed materials. Regular maintenance procedures, such as cleaning and replacing filters, are essential to ensure the system operates efficiently over time.
Benefits of Implementing Dust-Free Bulk Bag Unloading and Powder Conveying Systems
Adopting dust-free bulk bag unloading and powder conveying systems offers numerous benefits for industrial facilities. Firstly, these systems significantly reduce the risk of dust exposure for operators, improving workplace safety and compliance with occupational health regulations. By minimizing dust generation, they also help prevent product contamination, which is critical in industries where material purity is paramount, such as pharmaceuticals or food processing. Additionally, the enclosed design of these systems reduces the environmental impact by preventing dust emissions into the air, contributing to better air quality and compliance with environmental regulations. From an operational perspective, these systems enhance efficiency by allowing for faster and more consistent material transfer compared to traditional methods. The ability to control flow rates and maintain a steady supply of material reduces downtime and improves overall productivity. Furthermore, the use of enclosed conveying lines reduces the need for additional cleaning and housekeeping efforts, as dust is contained within the system rather than spreading throughout the facility. This leads to lower maintenance costs and a cleaner working environment. For companies looking to improve their material handling processes while adhering to safety and environmental standards, dust-free bulk bag unloading and powder conveying systems provide a reliable and effective solution.
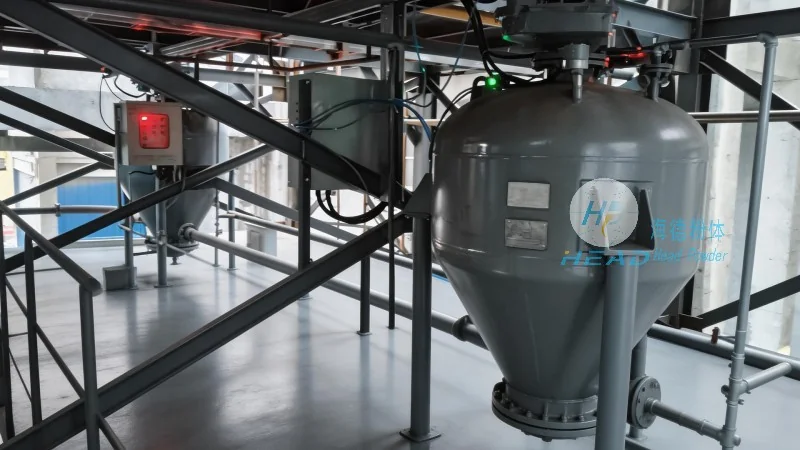
Conclusion and Company Overview
Dust-free bulk bag unloading and powder conveying systems are integral to modern industrial operations, offering a combination of efficiency, safety, and environmental responsibility. The working principle, which focuses on maintaining a sealed environment during material transfer, and the advanced features, such as enclosed lines and integrated filtration, work together to ensure optimal performance. The benefits of implementing these systems extend beyond operational efficiency to include improved safety, reduced environmental impact, and enhanced product quality. As a leader in engineering solutions for bulk material handling, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized dust-free systems tailored to the specific needs of various industries. With a commitment to quality and innovation, the company ensures that its products meet the highest standards of performance and reliability. Based in Shandong, China, HeadPowder has established itself as a trusted partner for businesses seeking to optimize their material handling processes while maintaining compliance with industry regulations. By leveraging advanced technology and expert engineering, HeadPowder continues to deliver solutions that enhance productivity and safety in industrial applications.




