

What is a Magnesium Sulfate Heptahydrate Powder Pneumatic Conveying System? And What Are Its Design
Magnesium sulfate heptahydrate, commonly known as Epsom salt, is a widely used chemical compound in various industrial applications. The efficient handling and transportation of this powder are crucial for maintaining production efficiency and product quality. A pneumatic conveying system specifically designed for magnesium sulfate heptahydrate powder offers a reliable solution to address these challenges. This article explores the concept of a magnesium sulfate heptahydrate powder pneumatic conveying system and delves into its underlying design principles.
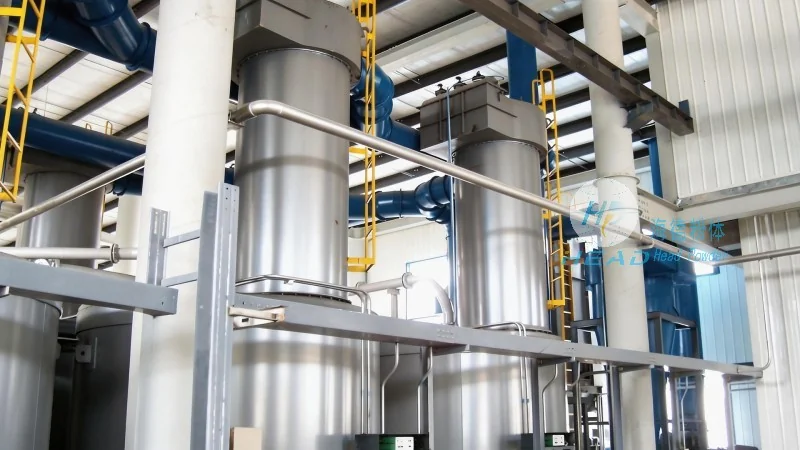
Understanding the Role of Pneumatic Conveying in Powder Handling
Pneumatic conveying systems utilize air or other gases to transport bulk materials like powders through a pipeline. For magnesium sulfate heptahydrate, which is hygroscopic and can be sensitive to moisture and temperature changes, the choice of an appropriate conveying method is vital. Traditional methods such as bucket elevators or belt conveyors may not be suitable due to the risk of material degradation or contamination. Pneumatic conveying, on the other hand, provides a closed system that minimizes exposure to external factors, ensuring the integrity of the powder during transport.
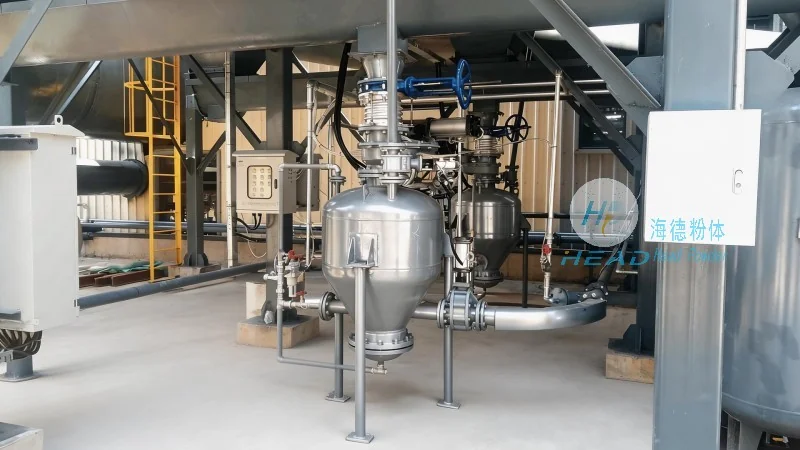
Key Components of a Magnesium Sulfate Heptahydrate Powder Pneumatic Conveying System
The design of a magnesium sulfate heptahydrate powder pneumatic conveying system involves several critical components that work in harmony to achieve efficient material transport. These components include the material feed hopper, which stores and regulates the flow of the powder; the air compressor or blower, which generates the necessary pressure to move the material; the conveying pipeline, which transports the powder and air mixture; and the discharge device, which delivers the material to the target location. Each component is carefully selected and sized to match the specific characteristics of magnesium sulfate heptahydrate, such as its particle size, density, and flowability.
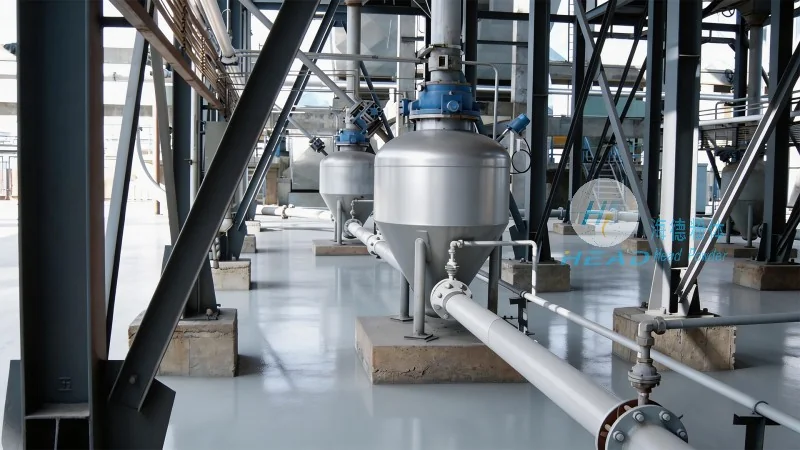
Design Principles for Optimal Performance
The design principles of a magnesium sulfate heptahydrate powder pneumatic conveying system are centered on maximizing efficiency, minimizing energy consumption, and ensuring the stability of the conveyed material. One of the primary design considerations is the selection of the appropriate conveying velocity. The velocity must be high enough to prevent particle deposition or blockage in the pipeline but low enough to avoid excessive wear and tear on the system components. The system also incorporates features like air filtration and moisture control to maintain the quality of the magnesium sulfate heptahydrate powder. Additionally, the design takes into account the need for easy maintenance and cleaning, as the system may need to be periodically flushed to prevent material buildup.
Benefits of Implementing a Specialized Pneumatic Conveying System
Adopting a pneumatic conveying system for magnesium sulfate heptahydrate powder offers numerous benefits for industrial operations. First, it enhances safety by eliminating the need for manual handling of the powder, reducing the risk of dust exposure and related health hazards. Second, it improves process efficiency by providing a continuous and automated material transport solution, which can lead to increased production throughput. Third, it maintains product quality by minimizing exposure to contaminants and environmental factors. Finally, it offers cost savings through reduced labor requirements and lower maintenance costs compared to traditional conveying methods.
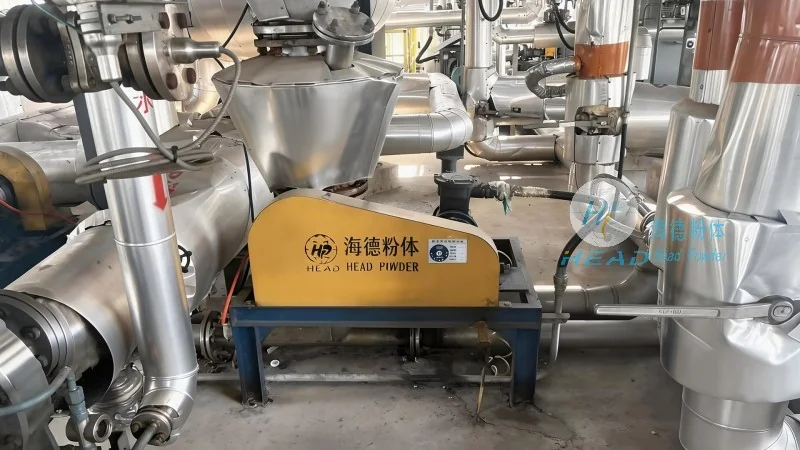
Conclusion and Company Overview
A magnesium sulfate heptahydrate powder pneumatic conveying system is a sophisticated piece of equipment designed to efficiently handle and transport this essential chemical compound. The design principles, which focus on efficiency, safety, and product quality, are crucial for ensuring the system operates optimally. Companies like Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specialize in designing and manufacturing such systems tailored to the specific needs of industrial clients. With a commitment to quality and innovation, HeadPowder offers reliable solutions that enhance the performance of magnesium sulfate heptahydrate powder handling processes. Based in Shandong, China, the company leverages its expertise to deliver customized pneumatic conveying systems that meet the demands of modern industrial applications.