Efficient and reliable material handling is crucial in the coffee processing industry, especially when dealing with dry coffee beans and grounds. Pneumatic conveying systems have emerged as a preferred solution for transporting these products due to their ability to maintain product integrity, ensure hygiene standards, and enhance operational efficiency. This article explores the role of pneumatic conveying in the handling of dry coffee, highlighting its benefits and the technical solutions provided by Shandong HeadPowder Engineering Co., Ltd.
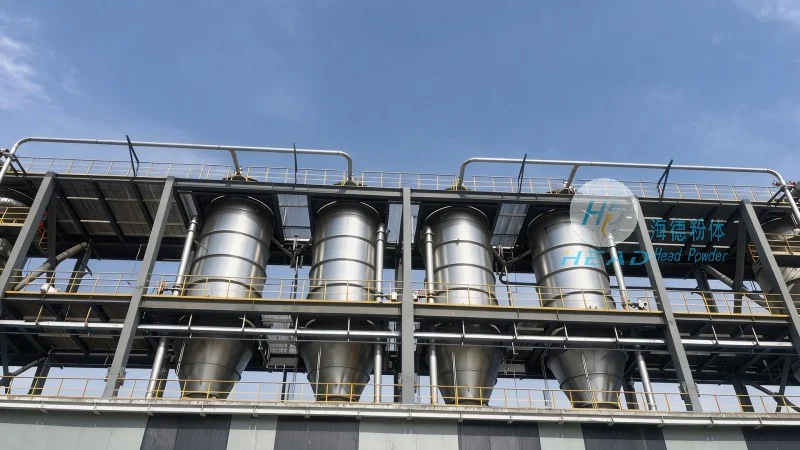
Advantages of Pneumatic Conveying for Dry Coffee
Pneumatic conveying offers several advantages that make it ideal for dry coffee transportation. One of the key benefits is the preservation of product quality. Unlike mechanical systems that may cause abrasion or contamination, pneumatic conveyors use air to move materials, minimizing the risk of damage to the coffee beans or grounds. This is particularly important for specialty coffees where the aroma and flavor profile are critical to the final product.
Another significant advantage is the ability to maintain a clean and hygienic environment. Pneumatic systems are enclosed, preventing dust and contaminants from entering the process. This is essential in food processing industries where compliance with health and safety regulations is mandatory. The enclosed design also helps in controlling odors and preventing cross-contamination between different coffee varieties.
Operational efficiency is another major benefit. Pneumatic conveyors can transport dry coffee over long distances with minimal energy consumption compared to traditional methods like belt conveyors or bucket elevators. They can handle varying flow rates and can be easily integrated into existing production lines, reducing downtime and increasing overall productivity. The flexibility of pneumatic systems allows for easy adjustments to accommodate changes in production volume or product types.
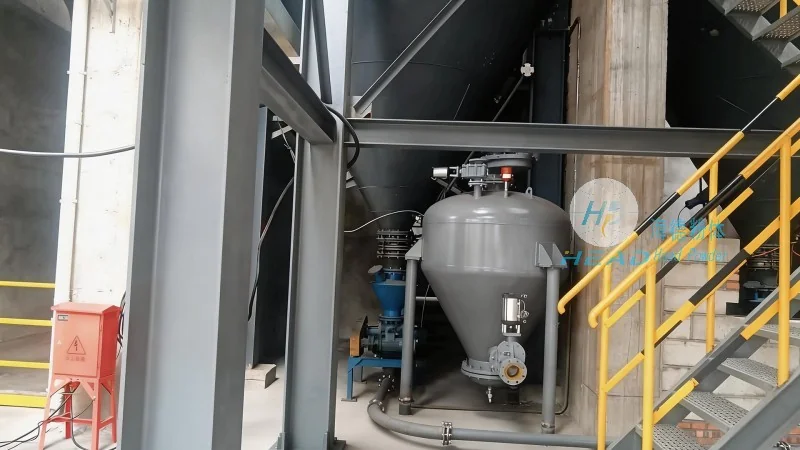
Technical Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing systems tailored to the specific needs of the coffee industry. The company's expertise lies in creating customized pneumatic conveying systems that ensure optimal performance and compliance with industry standards.
HeadPowder's solutions include a range of pneumatic conveying equipment such as positive pressure systems, negative pressure systems, and hybrid systems. These systems are engineered to handle the unique characteristics of dry coffee, including its density, moisture content, and flowability. The company's engineers work closely with clients to assess their specific requirements, from initial material handling challenges to final product delivery, ensuring that the chosen system meets all operational and regulatory requirements.
One of the key features of HeadPowder's systems is their ability to maintain product integrity throughout the conveying process. The company uses high-quality materials and advanced manufacturing techniques to ensure that the equipment is durable and can withstand the demands of continuous operation in a coffee processing facility. The systems are also designed for easy maintenance, with accessible components that allow for quick repairs and minimal downtime.
Applications in Coffee Processing
Pneumatic conveying is widely used in various stages of coffee processing. From the initial reception of raw coffee beans to the final packaging of ground coffee, these systems play a vital role in ensuring smooth and efficient operations. In the reception area, pneumatic conveyors can be used to transport coffee beans from storage silos or trucks into processing facilities, reducing the need for manual handling and associated risks.
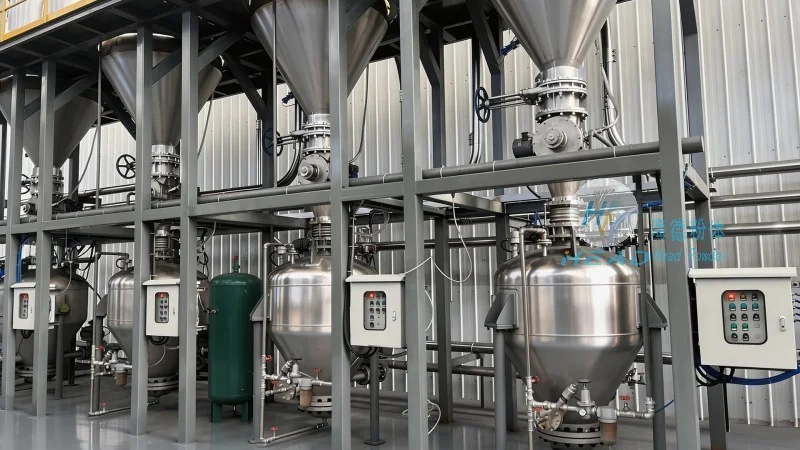
During the roasting process, pneumatic systems can be used to transport roasted beans to cooling and packaging areas. This helps in maintaining consistent temperature and moisture levels, which are crucial for preserving the flavor and aroma of the coffee. In the grinding and packaging stages, pneumatic conveyors are used to move ground coffee from the grinding machines to storage silos or packaging lines, ensuring that the product is handled gently and without contamination.
HeadPowder's systems are also suitable for handling coffee byproducts such as coffee husks and grounds. These materials are often transported using pneumatic conveyors to be used as fuel in coffee processing plants or for other industrial applications. The company's systems are designed to handle these materials efficiently, minimizing the risk of blockages and ensuring consistent flow rates.
Conclusion
Pneumatic conveying has become an indispensable part of modern coffee processing operations, offering significant advantages in terms of product quality, hygiene, and operational efficiency. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive pneumatic conveying solutions tailored to the coffee industry, ensuring that clients can achieve their production goals while maintaining the highest standards of quality and safety. With their expertise and commitment to innovation, HeadPowder continues to be a trusted partner in the coffee processing sector, helping businesses optimize their material handling processes and enhance overall productivity.




