HeadPowder, a leading enterprise in the field of alumina granules and conveying systems, specializes in providing high-quality technical solutions tailored to industrial needs. The company, officially known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China, and has established itself as a trusted provider of advanced material handling technologies for alumina granules.
Technical Parameters of Alumina Granules
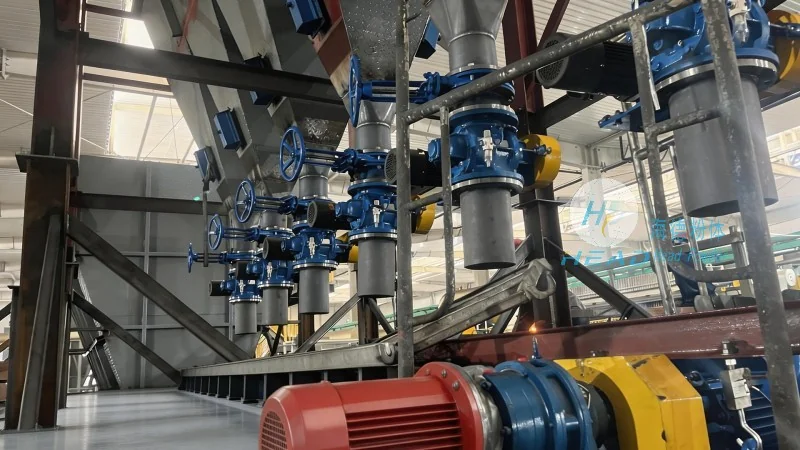
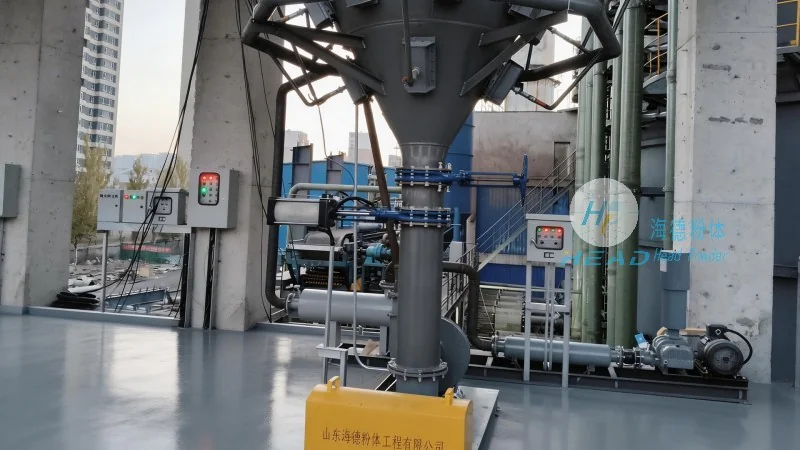
The technical parameters of alumina granules are crucial for ensuring optimal performance in various industrial applications. These parameters include particle size distribution, bulk density, moisture content, and chemical composition. For instance, the particle size distribution directly impacts the flowability and packing density of the material, which are critical factors in the design of conveying systems. HeadPowder's alumina granules are manufactured to meet stringent quality standards, with precise control over particle size to ensure consistent performance across different processes. The bulk density of the granules, typically ranging from 1.0 to 1.6 g/cm³, affects the capacity and efficiency of storage and transport equipment. Moisture content is carefully managed to prevent caking or degradation, which can compromise the material's properties and handling characteristics. Chemical composition, such as the alumina content and impurity levels, is also a key parameter, as it influences the final product's performance in applications like refractory materials, abrasives, and catalysts. HeadPowder employs advanced manufacturing processes, including high-temperature calcination and precise grinding, to achieve uniform particle characteristics and maintain consistent quality in every batch.
The Conveying System Process for Alumina Granules
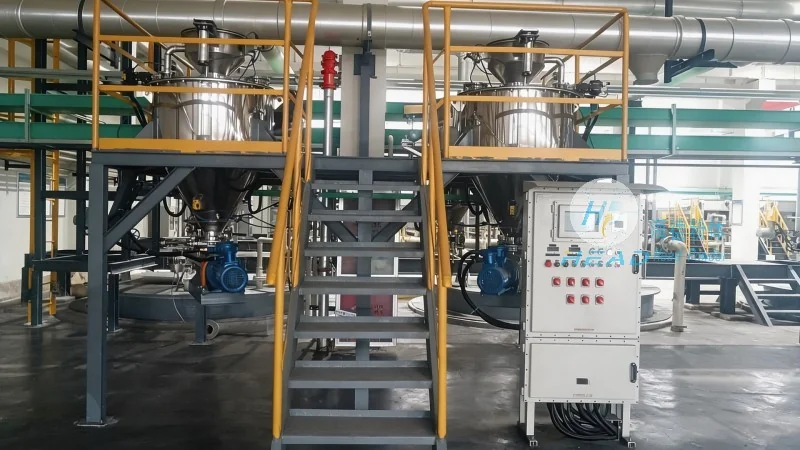
Conveying systems for alumina granules require specialized design to accommodate the material's physical properties and ensure efficient transport. The process typically involves several key components and operational steps. Initially, the alumina granules are stored in bulk storage silos or hoppers, where the material is held under controlled conditions to prevent segregation or degradation. From the storage silo, the granules are transferred to the conveying system via a series of feeders, such as rotary valves or vibratory feeders, which regulate the flow rate and prevent blockages. The conveying system itself may utilize different technologies depending on the application, including pneumatic conveying (air-assisted) or mechanical conveying (belt, screw, or chain conveyors). Pneumatic conveying is particularly effective for handling fine or dusty alumina granules, as it minimizes dust generation and allows for long-distance transport. Mechanical conveyors, on the other hand, are suitable for bulkier granules and provide a more cost-effective solution for shorter distances. The system includes components like pipelines, ducts, and control valves to direct the flow of the material to the desired destination, such as processing units, packaging lines, or storage areas. HeadPowder's conveying systems are engineered to handle the specific characteristics of alumina granules, ensuring minimal degradation, low energy consumption, and high reliability. The design incorporates features like anti-static measures to prevent dust accumulation and corrosion-resistant materials to withstand the chemical properties of the alumina. Additionally, the system is equipped with monitoring and control mechanisms to maintain consistent flow rates and detect any abnormalities, such as blockages or pressure drops, ensuring smooth and uninterrupted operation.
Quality Assurance and Technical Support
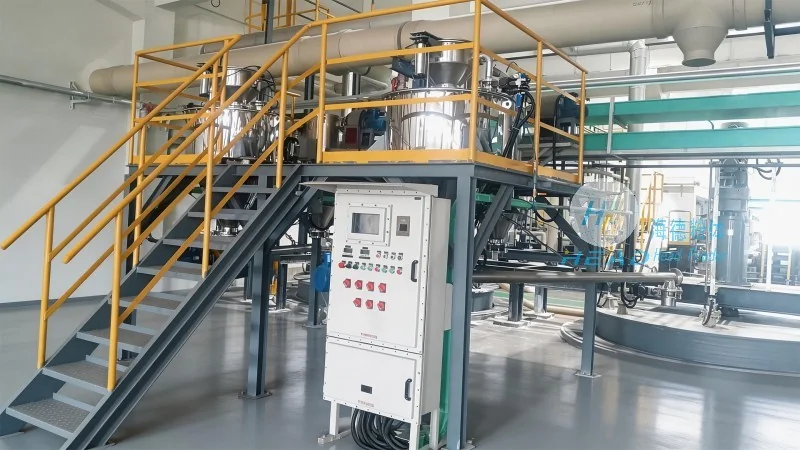
HeadPowder places a strong emphasis on quality assurance throughout the entire process of producing and delivering alumina granules and their conveying systems. The company adheres to international quality standards, such as ISO 9001, to ensure that all products meet the highest industry benchmarks. Each batch of alumina granules undergoes rigorous testing, including particle size analysis, bulk density measurement, moisture content determination, and chemical analysis, to verify compliance with specified parameters. The conveying systems are also subject to comprehensive testing, including performance trials and stress tests, to validate their efficiency and durability. HeadPowder's technical support team provides comprehensive assistance to clients, offering expertise in system design, installation, and maintenance. The team works closely with clients to understand their specific requirements and tailor solutions that address their unique challenges. Whether it's optimizing the conveying system for a new production line or troubleshooting existing issues, the technical support team provides timely and effective solutions. The company also offers training programs for clients' personnel to enhance their understanding of alumina granules and conveying systems, ensuring that they can operate and maintain the equipment efficiently. By combining advanced technology with dedicated customer support, HeadPowder ensures that its clients receive not only high-quality products but also reliable and sustainable solutions for their material handling needs.




