HeadPowder, a leading provider of engineering solutions, specializes in the design and implementation of pneumatic conveying systems tailored for the efficient transport of bulk sand particles. This article explores the application of pneumatic conveying technology in sand particle transport, highlighting the technical advantages and practical benefits offered by such systems.
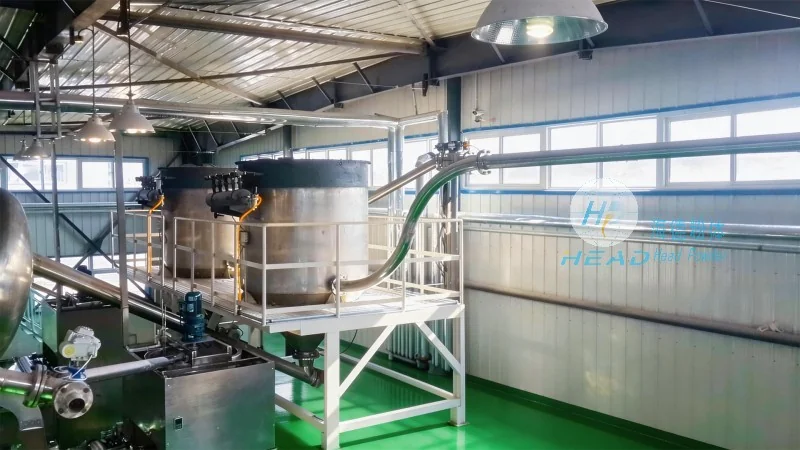
Understanding Pneumatic Conveying Systems
Pneumatic conveying systems utilize air or other gases to transport solid materials like sand particles through a pipeline network. These systems are categorized into two main types: dilute-phase and dense-phase. Dilute-phase systems, which are commonly used for sand transport, involve the suspension of particles in a high-velocity air stream, allowing for long-distance and high-capacity transport. Dense-phase systems, on the other hand, operate at lower velocities, ensuring a more controlled and gentle handling of the material, minimizing degradation and loss.
Key Advantages of Pneumatic Conveying for Sand Particles
When applied to sand particle transport, pneumatic conveying systems offer several distinct advantages over traditional methods such as belt conveyors or bucket elevators. Firstly, they provide a completely enclosed and dust-free environment, which is crucial for maintaining product quality and ensuring workplace safety. This enclosed system also prevents contamination from external sources, which is particularly important for sand used in construction, glass manufacturing, or other industrial applications where purity is paramount.
Secondly, pneumatic conveying systems offer high flexibility in terms of layout and installation. Unlike fixed conveyor systems, they can be easily reconfigured or expanded to accommodate changes in production needs or facility expansions. This adaptability makes them ideal for dynamic industrial environments where operational requirements may evolve over time.
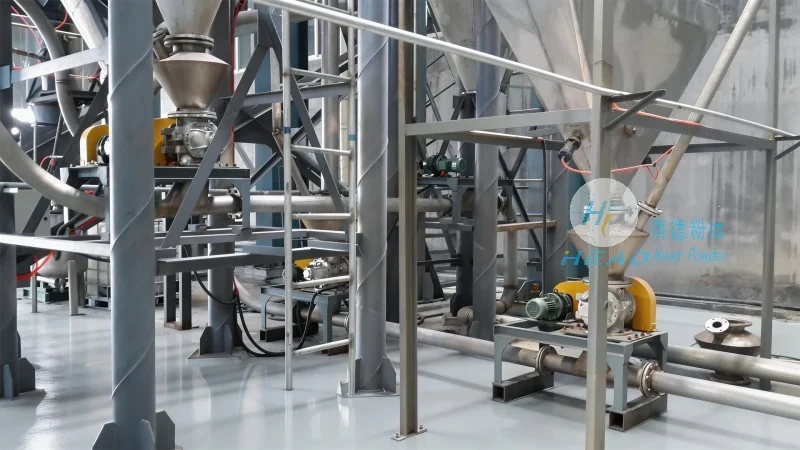
Thirdly, these systems are highly efficient in terms of energy consumption and operational costs. By using air as the conveying medium, they eliminate the need for mechanical components like rollers or chains, reducing maintenance requirements and associated costs. Additionally, the ability to transport sand particles over long distances with minimal energy input makes them economically viable for large-scale operations.
HeadPowder's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, has established itself as a trusted partner in the design and implementation of pneumatic conveying systems for sand particle transport. With years of experience in the industry, the company leverages advanced engineering principles and cutting-edge technology to develop customized solutions that meet the specific needs of each client. HeadPowder's team of experts works closely with clients to assess their operational requirements, material characteristics, and site constraints, ensuring that the final system is optimized for performance, reliability, and cost-effectiveness.
The company's approach to system design emphasizes both functionality and durability. By utilizing high-quality materials and components, HeadPowder ensures that its pneumatic conveying systems can withstand the abrasive nature of sand particles and operate reliably over extended periods. This commitment to quality is reflected in the long service life and low maintenance requirements of their systems, providing clients with a sustainable and cost-efficient solution for bulk sand transport.
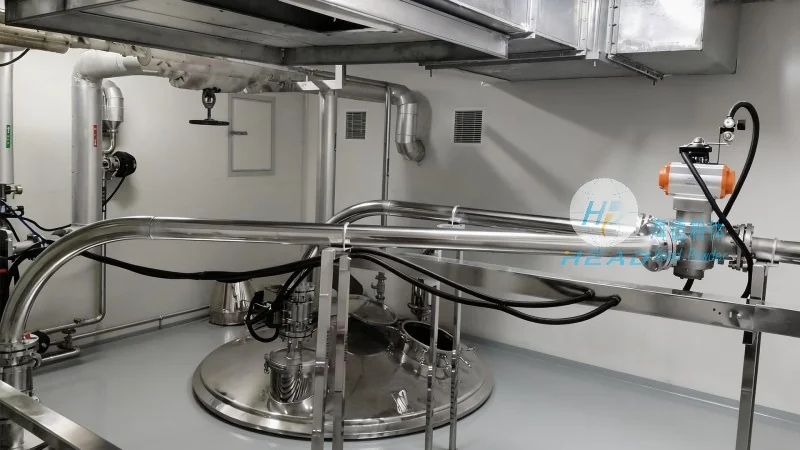
Application Examples and Industry Impact
Pneumatic conveying systems are widely used in various industries that rely on sand particles for their production processes. In the construction industry, these systems are employed to transport sand from storage silos to mixing plants, ensuring a consistent and controlled supply of material for concrete and mortar production. In the glass manufacturing sector, pneumatic conveying is critical for transporting sand and other raw materials to the melting furnaces, where precise control over material flow is essential for maintaining product quality.
In addition to construction and glass, pneumatic conveying is also utilized in the foundry industry for transporting sand molds and cores, and in the mining sector for handling sand and other bulk materials from processing plants to storage or shipping facilities. The versatility of these systems makes them suitable for a wide range of applications, from small-scale operations to large industrial complexes.
Conclusion
For businesses seeking efficient, reliable, and cost-effective solutions for the bulk transport of sand particles, pneumatic conveying systems represent a superior choice. With its enclosed operation, flexibility, and energy efficiency, this technology offers significant advantages over traditional methods. HeadPowder, with its expertise and commitment to quality, continues to provide innovative pneumatic conveying solutions that meet the evolving needs of the industry, ensuring that clients can achieve optimal performance and operational success in their sand particle transport processes.




