For industrial applications requiring safe and efficient material handling, the inert gas circulating pneumatic conveying system stands out as a reliable solution. This article provides an overview of its structure and operational principles, highlighting key components and how they work together to ensure optimal performance.
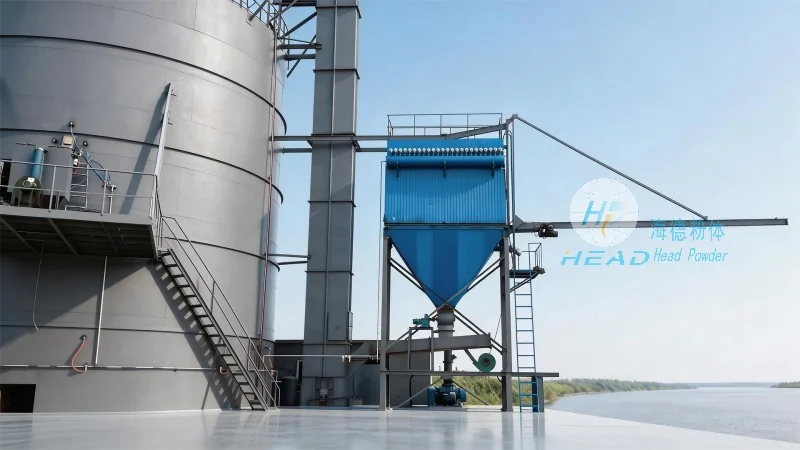
Overview of Inert Gas Circulating Pneumatic Conveying Systems
The inert gas circulating pneumatic conveying system is designed to transport bulk materials through a closed loop using inert gases, typically nitrogen or carbon dioxide, to prevent oxidation or contamination. This method is particularly valuable in industries such as pharmaceuticals, food processing, and chemical manufacturing, where material purity and safety are paramount.
Key Structural Components and Their Functions
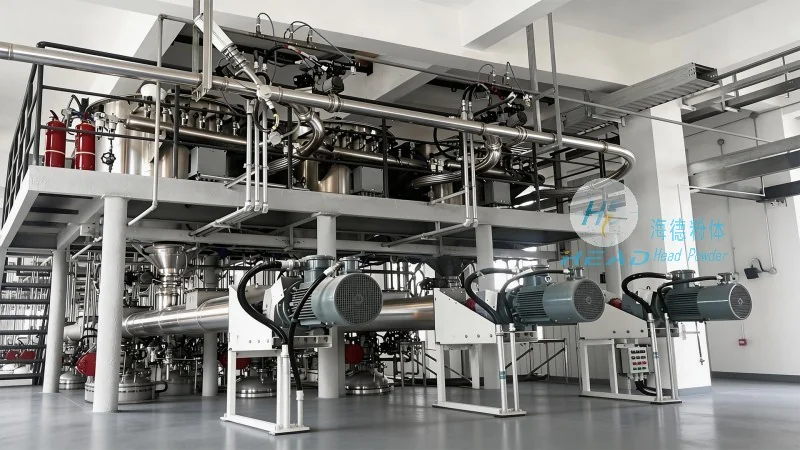
The system comprises several critical components that work in concert to facilitate material transport. These include the material feed hopper, which introduces the bulk material into the system; the gas distributor, responsible for evenly distributing the inert gas; the conveying pipeline, which forms the main transport path; and the material separator, which separates the conveyed material from the gas at the discharge end.
Additionally, the system features a gas circulation unit that recovers and reuses the inert gas, reducing operational costs and environmental impact. This unit typically includes a gas filter to remove particulates and a pressure regulator to maintain consistent gas pressure throughout the system.
Operational Principle: How the System Works
The operational principle of the inert gas circulating pneumatic conveying system is based on the creation of a low-pressure zone within the conveying pipeline. The material feed hopper is connected to the pipeline, and as the inert gas is introduced, it creates a flow that draws the material particles into the gas stream. The gas, carrying the material, moves through the pipeline to the discharge point, where the material is separated from the gas by a separator.
The separated inert gas is then circulated back to the gas distributor, completing the loop. This closed-loop design minimizes gas consumption and ensures a continuous, stable operation. The system can be adjusted to handle various material types and flow rates, making it versatile for different industrial applications.
Advantages of Inert Gas Circulating Pneumatic Conveying
One of the primary advantages of this system is its ability to maintain material purity and prevent contamination. By using inert gases, the system eliminates the risk of oxidation or chemical reactions that could compromise the quality of the conveyed material. Additionally, the closed-loop design reduces energy consumption and operational costs compared to traditional pneumatic conveying systems.
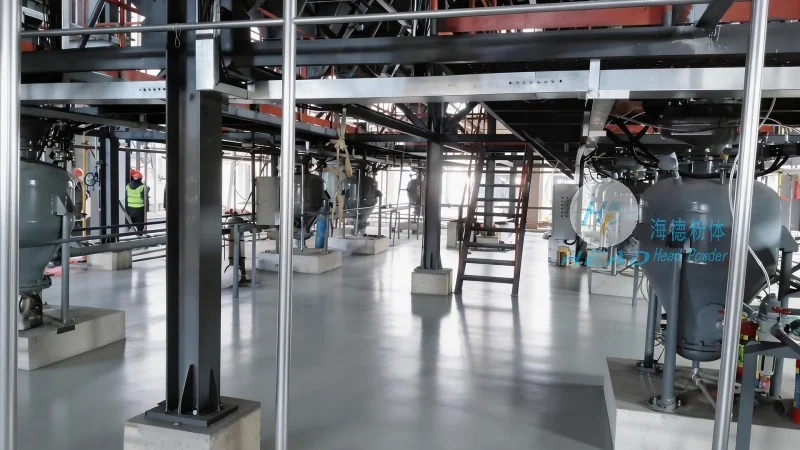
The system also offers enhanced safety features, as the inert gas environment reduces the risk of fire or explosion in environments where flammable materials are handled. This makes it suitable for applications where safety is a top priority. Furthermore, the modular design allows for easy integration into existing production lines and scalability to meet growing material handling demands.
Application Examples and Industry Use Cases
The inert gas circulating pneumatic conveying system is widely used in various industries. In the pharmaceutical industry, it is employed to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements. In food processing, it handles ingredients like powders and granules while maintaining food safety standards. The chemical industry utilizes it for transporting reactive chemicals that require an inert atmosphere to prevent unwanted reactions.
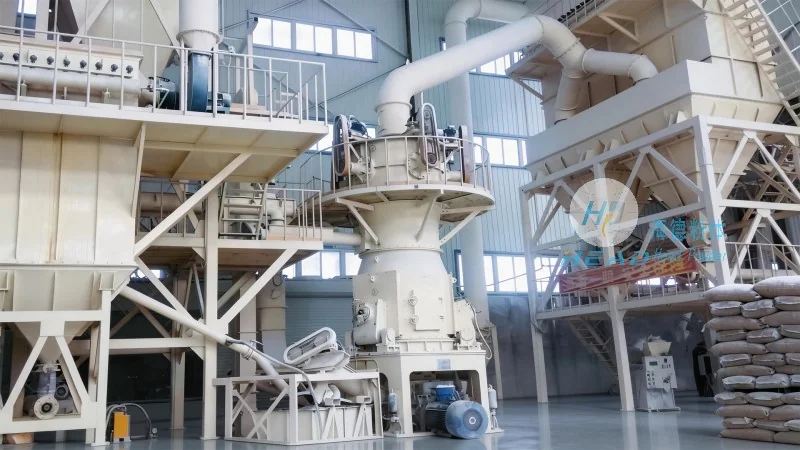
These applications benefit from the system's ability to handle sensitive materials without degradation, ensuring consistent product quality and compliance with industry regulations. The system's flexibility in handling different material characteristics, such as particle size and moisture content, makes it a preferred choice for diverse industrial needs.
Conclusion: The Role of Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality inert gas circulating pneumatic conveying systems. With a focus on innovation and customer satisfaction, the company provides tailored solutions that meet the specific needs of various industries. By leveraging advanced engineering and rigorous quality control, HeadPowder ensures that its systems deliver reliable performance and long-term value to clients.
Whether for new installations or system upgrades, Shandong HeadPowder Engineering Co., Ltd. offers comprehensive support, from initial design and installation to ongoing maintenance and technical assistance. The company's commitment to excellence and customer-centric approach has established it as a trusted partner in the material handling industry, helping businesses achieve efficient, safe, and cost-effective material transport solutions.




