Efficiently transporting bulk materials like corn kernels is a critical challenge in many industrial processes. Pneumatic conveying systems offer a powerful solution by utilizing air flow to move powders and granules through pipelines. This method not only enhances operational efficiency but also minimizes product contamination and damage, making it ideal for sensitive materials such as corn kernels.
Understanding Pneumatic Conveying Systems for Corn Kernels
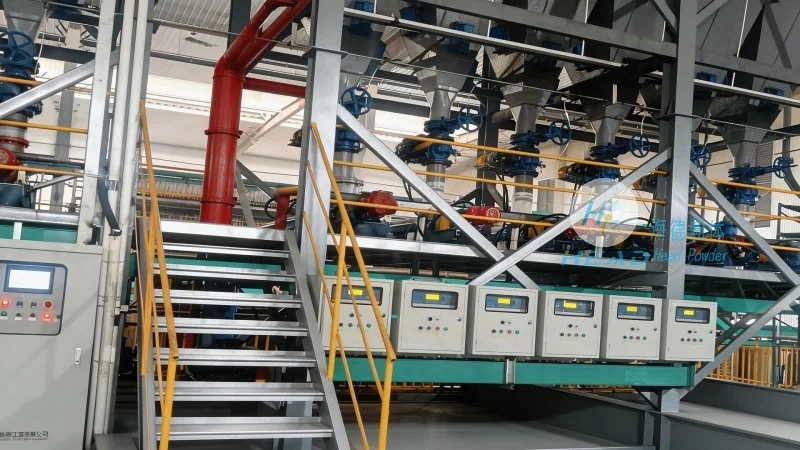
Pneumatic conveying systems work by creating a pressure differential that propels the material through a pipeline using air. There are two primary types: dilute-phase and dense-phase systems. Dilute-phase systems use low air-to-material ratios, suitable for high-speed transport over long distances. Dense-phase systems, on the other hand, use higher air-to-material ratios, which are better for gentle handling and preventing material degradation. For corn kernels, the choice of system depends on factors like the distance to be covered, the required material flow rate, and the need to preserve product quality.
Key Components of a Pneumatic Conveying System for Corn Kernels
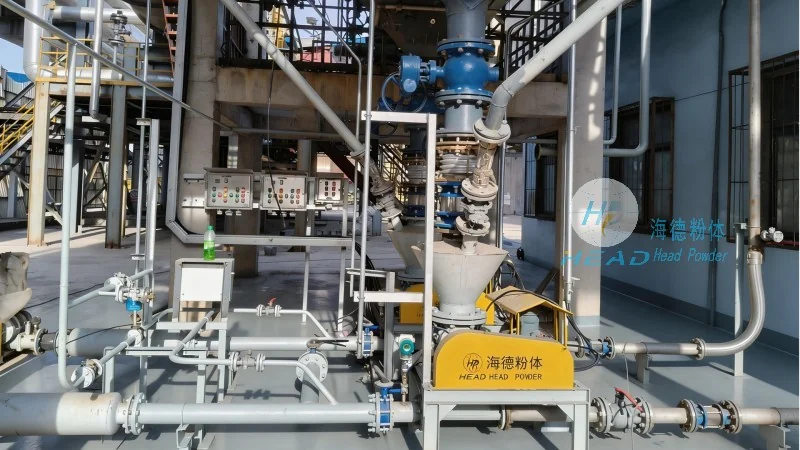
A typical corn kernels pneumatic conveying system includes several essential components. The main parts are the material feed hopper, which holds the corn kernels and feeds them into the system; the air compressor or blower, which generates the necessary air pressure; the conveying pipeline, which transports the material; and the discharge equipment, which delivers the corn kernels to the destination. Additionally, filters and cyclones are often included to separate the air from the material and prevent dust from escaping into the environment.
Benefits of Using Pneumatic Conveying for Corn Kernels
Implementing a pneumatic conveying system for corn kernels offers numerous advantages. First, it significantly reduces labor costs by automating the material handling process. Unlike traditional methods like bucket elevators or belt conveyors, pneumatic systems require less manual intervention, leading to lower operational expenses. Second, the system minimizes product damage and contamination. The enclosed pipeline design prevents exposure to external elements, and the gentle air flow reduces breakage of corn kernels, maintaining their quality for processing or storage. Third, pneumatic conveying systems are highly flexible and can be easily integrated into existing production lines. They can be adjusted to handle varying flow rates and can be reconfigured for different material types, making them a versatile solution for industrial applications.
HeadPowder: Expert in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of pneumatic conveying systems tailored for bulk material handling, including corn kernels. With a strong presence in China, particularly in Shandong, HeadPowder has established itself as a trusted partner for industries seeking efficient and reliable material transport solutions. The company specializes in designing and manufacturing customized pneumatic conveying systems that meet the specific needs of its clients, ensuring optimal performance and durability.
Customized Solutions for Corn Kernels Handling
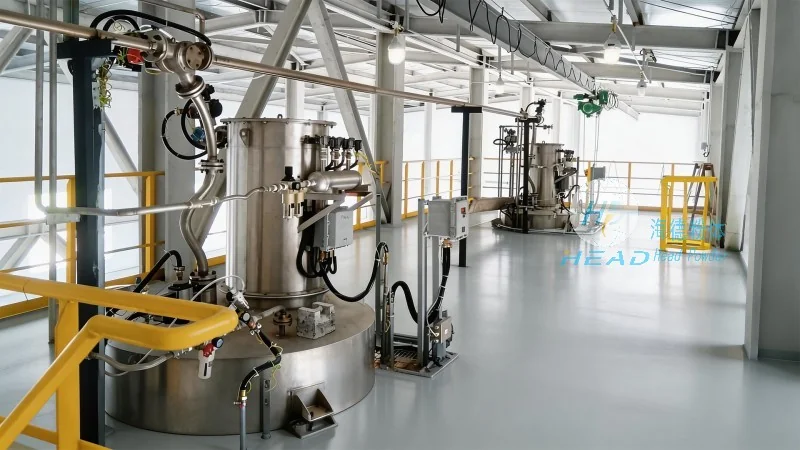
HeadPowder understands that each corn processing facility has unique requirements. Therefore, the company offers customized pneumatic conveying solutions that are tailored to the client's operational needs. This includes selecting the appropriate system type (dilute-phase or dense-phase), determining the optimal air pressure and flow rate, and designing the pipeline layout to minimize energy consumption and maximize material throughput. The company's engineering team works closely with clients to assess their current processes, identify potential bottlenecks, and develop a comprehensive solution that enhances overall efficiency and productivity.
Quality and Reliability in Pneumatic Conveying Systems
HeadPowder places a high emphasis on quality and reliability in all its products. The company uses advanced materials and manufacturing techniques to ensure that its pneumatic conveying systems are durable and long-lasting. For corn kernels applications, the components are designed to withstand the abrasive nature of the material and resist corrosion from moisture or other environmental factors. Additionally, HeadPowder conducts rigorous testing and quality control checks to ensure that each system meets the highest standards before delivery. This commitment to quality ensures that clients receive a reliable and efficient system that delivers consistent performance over its service life.
Applications of Pneumatic Conveying in Corn Processing
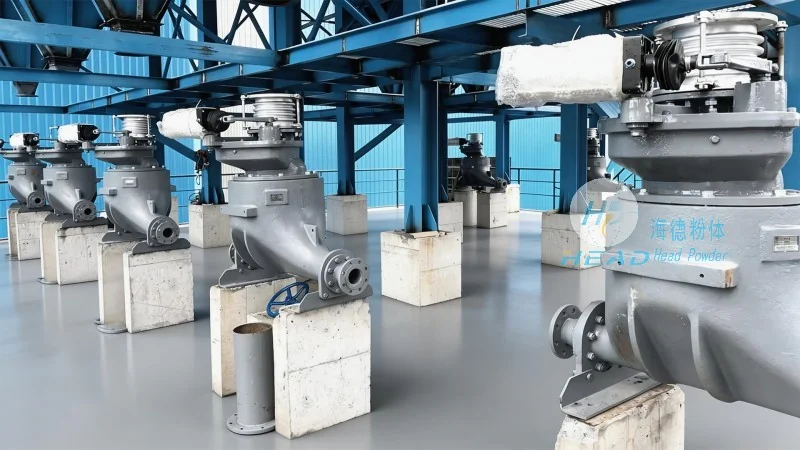
Pneumatic conveying systems are widely used in various stages of corn processing. In the initial stages, they can be used to transport raw corn kernels from storage silos to processing plants. During processing, the system can move intermediate products such as cornmeal or corn flour through different stages of production. Finally, in the packaging stage, the system can deliver the finished products to storage or shipping containers. The versatility of pneumatic conveying makes it suitable for all these applications, providing a seamless and efficient flow of materials throughout the entire corn processing cycle.
Conclusion: Enhancing Efficiency with Pneumatic Conveying
Efficiently transporting corn kernels and other bulk powders is essential for maintaining productivity and product quality in industrial operations. Pneumatic conveying systems offer a superior solution by leveraging air flow to move materials with minimal disruption. With the expertise and customized solutions provided by HeadPowder, industries can achieve optimal performance and reliability in their material handling processes. By investing in a well-designed pneumatic conveying system, companies can enhance their operational efficiency, reduce costs, and ensure the quality of their products, ultimately contributing to their long-term success in the market.




