HeadPowder, a leading enterprise in the field of material handling solutions, specializes in providing advanced pneumatic conveying equipment tailored for various industrial applications. One of their core products is the magnesium oxide powder material pneumatic conveying machine, designed to efficiently transport fine powders like magnesium oxide with precision and reliability. This equipment is engineered to meet the demanding requirements of modern industrial processes, ensuring smooth and safe material handling operations.
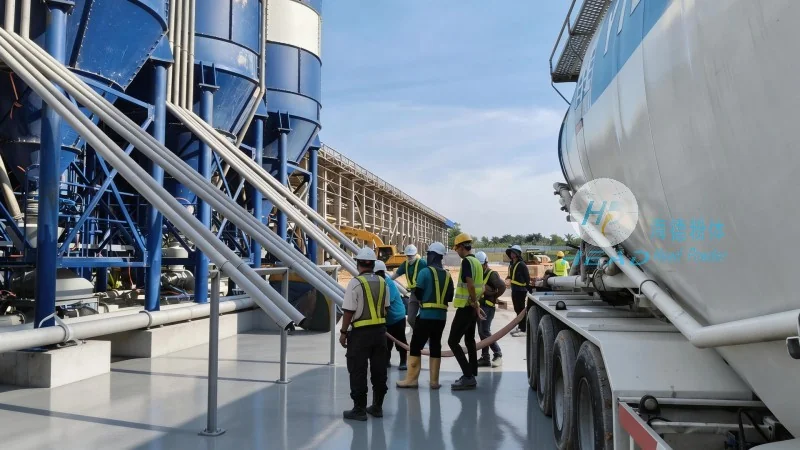
System Components and Their Roles
The magnesium oxide powder pneumatic conveying machine typically consists of several key components that work in tandem to achieve efficient material transport. The primary components include a feeding system, a conveying pipeline network, a separation and collection unit, and an air filtration system. The feeding system is responsible for introducing the magnesium oxide powder into the system, often using a hopper or a rotary valve to control the flow rate. The conveying pipeline, usually made of stainless steel or other corrosion-resistant materials, ensures the safe and efficient movement of the powder particles. The separation unit, such as a cyclone separator or a bag filter, separates the powder from the air stream, directing the powder to the collection bin while allowing the air to be filtered and discharged. The air filtration system is crucial for maintaining air quality and complying with environmental regulations.
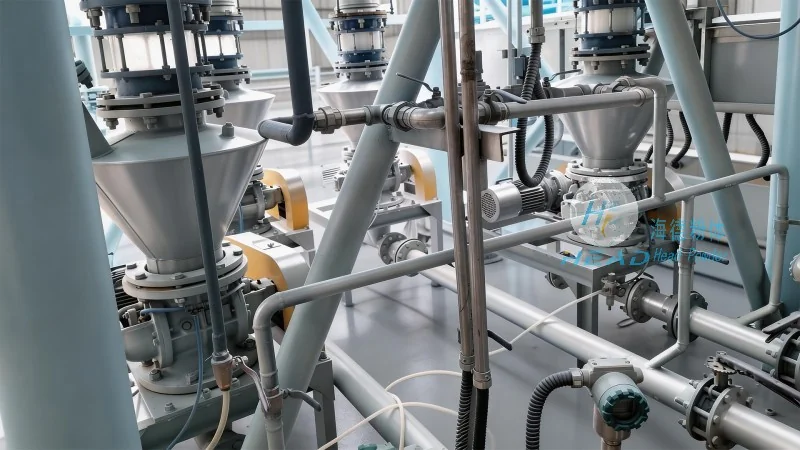
Operation Process: Step-by-Step Workflow
The operation of the magnesium oxide powder pneumatic conveying machine follows a systematic workflow that ensures consistent and reliable performance. The process begins with the loading of magnesium oxide powder into the feeding hopper. A rotary valve or a screw feeder then controls the discharge of the powder into the conveying pipeline. Simultaneously, a high-pressure air source, such as a blower or a compressor, generates the air flow that propels the powder particles through the pipeline. As the powder-air mixture travels through the pipeline, it reaches the separation unit where the powder is separated from the air. The separated powder is collected in a designated bin, while the air passes through a filter to remove any residual dust particles before being released into the environment. This step-by-step process minimizes downtime and maximizes the efficiency of material transport, making it an ideal solution for continuous production lines.
Working Principle: How the System Transports Materials
The working principle of the magnesium oxide powder pneumatic conveying machine is based on the principles of fluid dynamics and particle motion. The system operates by creating a pressure differential between the feeding point and the discharge point. The high-pressure air generates a flow velocity that is sufficient to lift and transport the fine powder particles. The air flow acts as a carrier, carrying the powder particles along the pipeline. The design of the pipeline, including bends and fittings, is optimized to minimize pressure loss and maintain the stability of the powder-air mixture. The separation unit uses centrifugal force to separate the heavier powder particles from the lighter air stream. The efficiency of the separation process is critical to the overall performance of the system, as it determines the purity of the collected powder and the effectiveness of the air filtration. By understanding and optimizing these principles, HeadPowder ensures that their pneumatic conveying machines deliver consistent performance and meet the specific needs of their clients.
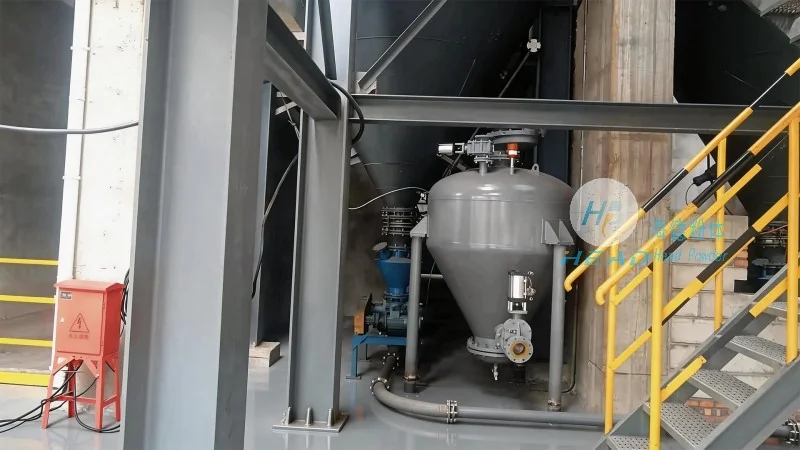
Advantages and Applications in Industrial Settings
The magnesium oxide powder pneumatic conveying machine offers several advantages that make it a preferred choice for industrial applications. One of the key benefits is the ability to transport fine powders without the need for mechanical components like belts or chains, which reduces the risk of contamination and wear. The system is also highly flexible, allowing for changes in the conveying route or capacity without major modifications. Additionally, the enclosed design minimizes dust emissions, improving workplace safety and compliance with environmental regulations. HeadPowder's equipment is widely used in industries such as chemical manufacturing, pharmaceuticals, and food processing, where the handling of sensitive powders requires precision and reliability. The company's commitment to quality and innovation ensures that their pneumatic conveying machines are tailored to meet the unique requirements of each application, providing long-term value and efficiency for their clients.




