HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for handling sodium bicarbonate materials. This article delves into the operational process and underlying principles of such equipment, offering insights into how these machines efficiently transport sodium bicarbonate while maintaining product integrity.
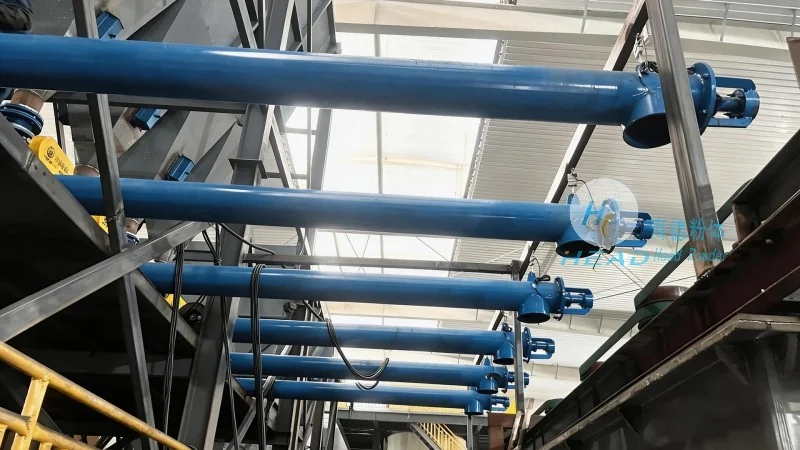
HeadPowder, the company behind this technology, is a professional engineering enterprise headquartered in Shandong, China. The company's full name is Shandong HeadPowder Engineering Co., Ltd., and it operates from its main office located in the Shandong province, providing specialized solutions for material handling in various industrial sectors.
Operation Process of the Sodium Bicarbonate Pneumatic Conveying Machine
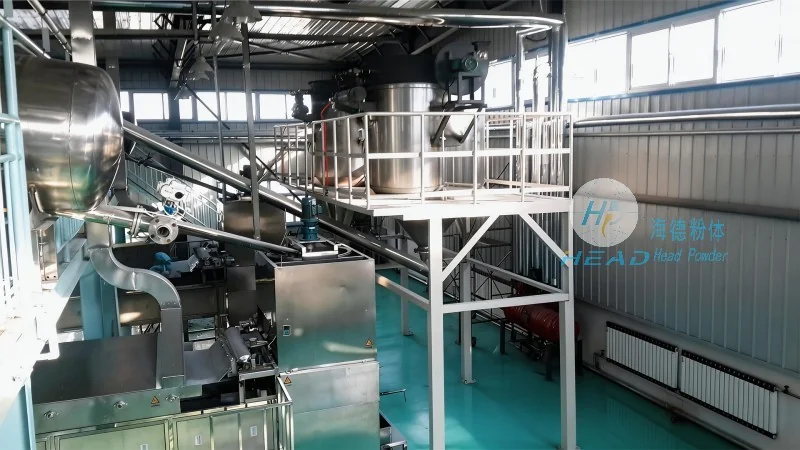
The operation of a sodium bicarbonate material pneumatic conveying machine involves several key stages, each designed to ensure efficient and reliable material transport. The process begins with the loading of sodium bicarbonate into the hopper or feeder. The material is then fed into the conveying line under controlled conditions, where it is mixed with high-pressure air. As the air and material move through the pipeline, the machine utilizes a combination of pressure differentials and air velocity to propel the sodium bicarbonate forward. The conveying line may include components such as bends, valves, and filters to manage the flow and prevent blockages. Upon reaching the discharge point, the material is separated from the air, typically through a cyclone or other separation device, and collected in the receiving hopper. The entire process is automated and monitored to maintain consistent performance and minimize downtime.
Working Principle of the Pneumatic Conveying System
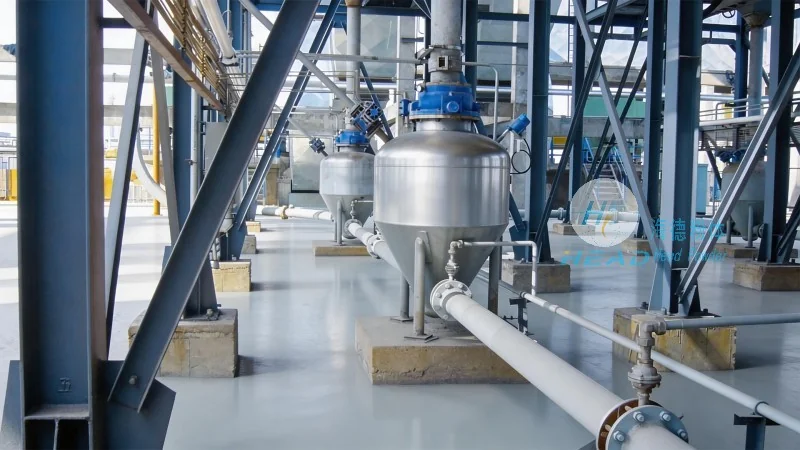
The working principle of the sodium bicarbonate pneumatic conveying machine is based on the fundamental concept of pneumatic transport, where solid materials are conveyed using a gas (usually air) as the medium. The system operates by creating a pressure differential between the inlet and outlet of the conveying line. At the inlet, high-pressure air is introduced, which draws the sodium bicarbonate particles into the pipeline. The air velocity is carefully controlled to ensure that the particles are fully suspended and transported without settling or clogging. The machine may employ different types of pneumatic conveying, such as pressure or vacuum systems, depending on the specific application requirements. Pressure systems use compressed air to push the material, while vacuum systems use suction to draw the material. For sodium bicarbonate, a pressure system is often preferred due to the material's density and flow characteristics. The system also includes features like air filtration and moisture control to maintain the quality of the transported material, ensuring that the sodium bicarbonate remains in its desired state without degradation.
Key Features and Benefits for Sodium Bicarbonate Handling
When applied to sodium bicarbonate, the pneumatic conveying machine offers several advantages that make it an ideal choice for industrial operations. First, it provides a continuous and automated material transport process, reducing manual labor and increasing operational efficiency. The system is also capable of handling large volumes of sodium bicarbonate, making it suitable for high-production environments. Additionally, the equipment is designed to minimize product degradation, as the material is not exposed to excessive friction or mechanical stress during transport. The use of air as the conveying medium also allows for gentle handling, preserving the purity and quality of the sodium bicarbonate. Furthermore, the machine can be integrated with other processing equipment, such as mixers or packaging systems, to form a complete production line. This integration enhances overall process efficiency and reduces the need for manual transfers between different stages of production.
Conclusion
HeadPowder's sodium bicarbonate material pneumatic conveying machine exemplifies advanced engineering solutions for material handling in the chemical industry. By understanding the operational process and working principles, users can appreciate how these machines efficiently transport sodium bicarbonate while maintaining product integrity. The combination of robust design, automated controls, and specialized features makes this equipment a reliable choice for industries that rely on consistent and high-quality sodium bicarbonate supply. With its headquarters in Shandong, China, HeadPowder continues to innovate and provide tailored solutions to meet the evolving needs of its clients in the material handling sector.




