Red mud, a byproduct of bauxite processing in the aluminum industry, poses significant challenges in handling and transportation due to its high moisture content and abrasive nature. The red mud powder conveying system equipment is a specialized solution designed to address these challenges efficiently. This equipment is crucial for industries dealing with red mud, as it ensures safe, reliable, and cost-effective transportation of this material from processing sites to disposal or reuse locations.
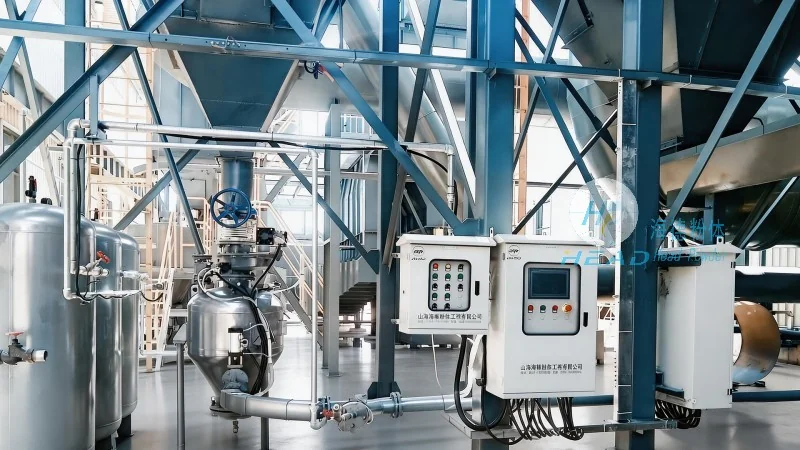
Understanding the Red Mud Powder Conveying System Equipment
The red mud powder conveying system equipment is engineered to handle the unique properties of red mud, which includes high moisture levels, fine particle size, and abrasive characteristics. These properties make traditional conveying methods less effective and can lead to equipment wear and operational inefficiencies. The system typically comprises components such as feeders, conveyors, and control systems, all designed to work in harmony to ensure smooth and continuous material transport. The equipment is tailored to meet the specific requirements of red mud, including its density, flowability, and potential for caking or agglomeration.
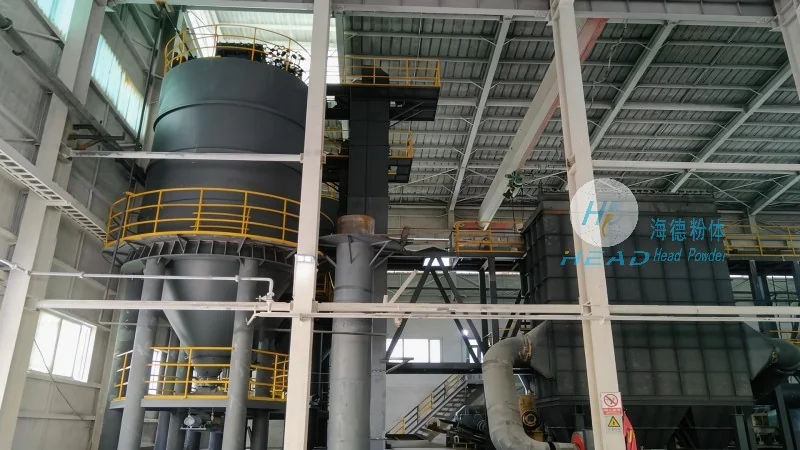
Design Principles of the Red Mud Powder Conveying System
The design of the red mud powder conveying system equipment follows several key principles aimed at optimizing performance and durability. First, the system is designed to minimize material degradation and loss during transport, which is critical for maintaining the quality of red mud for potential reuse or disposal. Second, the equipment is built to withstand the abrasive nature of red mud, using materials such as high-strength alloys and wear-resistant coatings to extend service life. Third, the system incorporates advanced control technologies to ensure precise flow control and prevent blockages or overloading. Additionally, the design prioritizes energy efficiency, reducing operational costs while maintaining high throughput rates. The integration of these principles results in a robust and reliable system that can handle the demanding conditions associated with red mud transport.
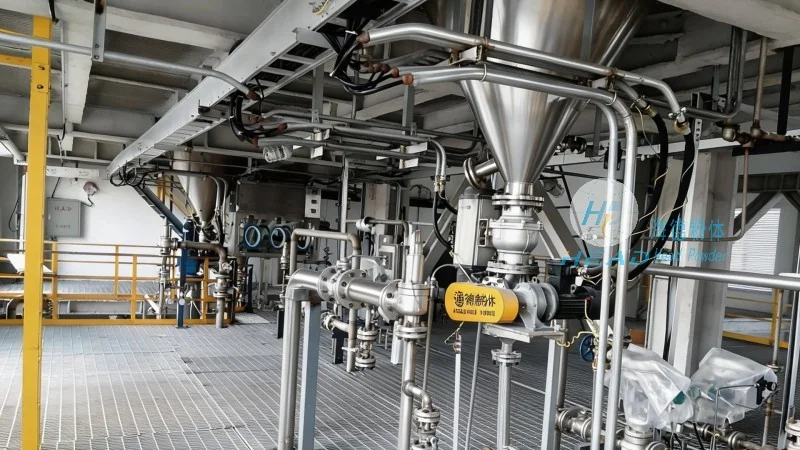
About Shandong HeadPowder Engineering Co., Ltd.
Headpowder, the manufacturer of the red mud powder conveying system equipment, is a leading company in the field of powder handling and material transport solutions. With its headquarters in Shandong, China, Headpowder has established itself as a trusted provider of industrial equipment tailored to the needs of various industries, including aluminum processing, mining, and waste management. The company specializes in designing and manufacturing customized conveying systems that address the unique challenges of different materials, ensuring optimal performance and longevity. Headpowder's commitment to quality and innovation has earned it a reputation for delivering reliable and efficient solutions to its clients worldwide. The company's team of experts works closely with clients to understand their specific requirements and develop tailored solutions that meet their operational needs and budget constraints.
Key Features and Benefits of the Red Mud Powder Conveying System
The red mud powder conveying system equipment from Headpowder offers several key features and benefits that make it an ideal choice for red mud transport applications. One of the primary advantages is its ability to handle high moisture content and fine particles without clogging or degradation. The system's design includes advanced feeding mechanisms that ensure consistent material flow, reducing the risk of blockages and downtime. Another key feature is the use of wear-resistant components, which extend the equipment's service life and reduce maintenance costs. The system also incorporates energy-efficient motors and control systems, contributing to lower operational expenses. Furthermore, the equipment is designed for easy maintenance and cleaning, with accessible components that simplify routine checks and repairs. The combination of these features results in a system that is not only effective in transporting red mud but also cost-effective and reliable over the long term.
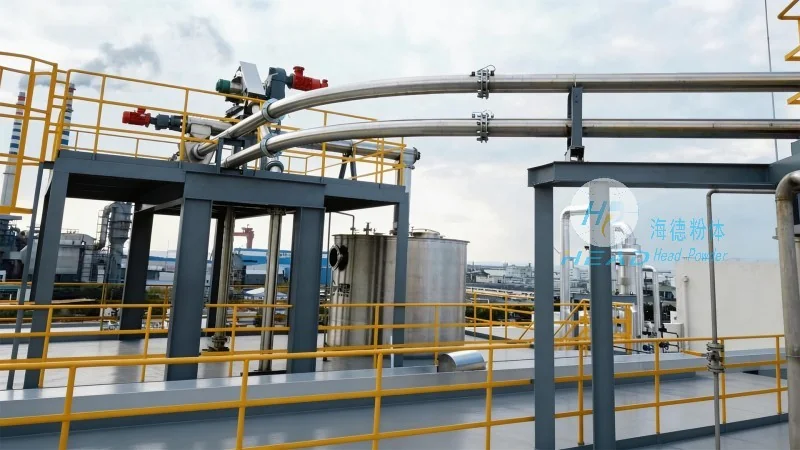
Applications and Use Cases
The red mud powder conveying system equipment is widely used in various applications within the aluminum industry and related sectors. In aluminum processing plants, the system is used to transport red mud from the digestion and washing stages to storage or disposal sites. The equipment ensures that the red mud is moved efficiently and safely, minimizing the risk of environmental contamination and operational disruptions. Additionally, the system can be used in mining operations where red mud is a byproduct of bauxite extraction. In waste management facilities, the equipment helps in the transport of red mud for recycling or disposal, contributing to sustainable waste management practices. The versatility of the system makes it suitable for a range of applications, from small-scale operations to large industrial plants, providing a reliable solution for red mud handling needs.




