HeadPowder, a leading provider in the field of material handling solutions, specializes in the design and implementation of efficient pneumatic conveying systems for the cereal industry. This article delves into the operation process and working principles of such systems, highlighting how they enhance productivity and maintain product integrity in cereal processing operations.
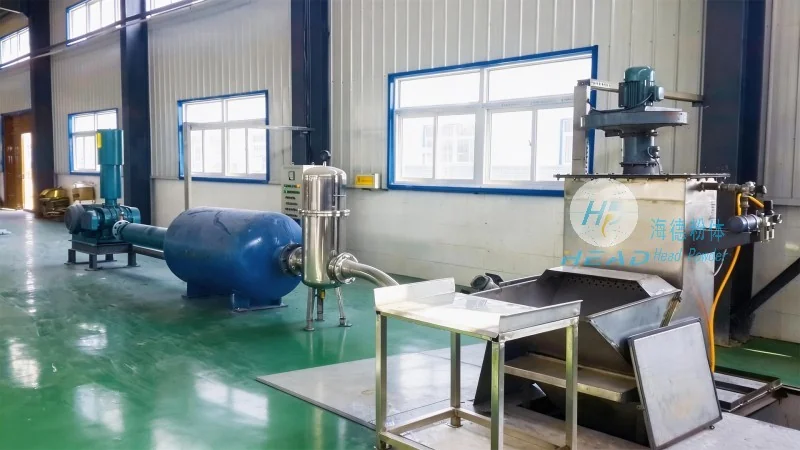
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable pneumatic conveying solutions tailored to the unique demands of the cereal sector. Our expertise spans the entire lifecycle of system design, from initial consultation to installation and ongoing maintenance, ensuring that clients receive comprehensive support throughout their operational journey.
The Pneumatic Conveying Process: A Step-by-Step Overview
Pneumatic conveying of cereals involves the transport of bulk materials through a pipeline using pressurized or vacuum air. The process begins with the material being introduced into the system, typically from a hopper or storage silo. As air is introduced into the pipeline, it creates a flow that propels the cereal particles forward. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing the risk of product contamination. The system operates by maintaining a consistent air pressure or vacuum level, which ensures smooth and continuous movement of the material.
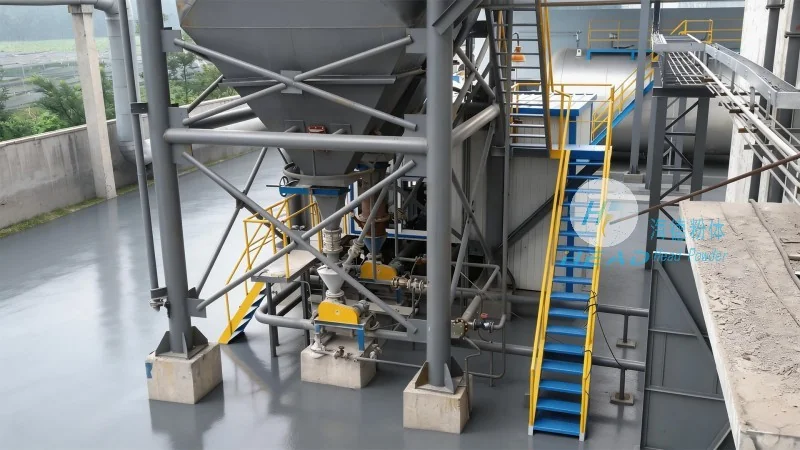
Working Principle: How Pneumatic Conveying Systems Function
The core working principle of pneumatic conveying systems for cereals revolves around the interaction between air and the material particles. In a pressurized system, air is forced into the pipeline at a high pressure, creating a stream that carries the cereal grains. The air velocity is carefully controlled to ensure that the particles remain suspended and move without settling or clogging the line. Conversely, in a vacuum system, air is drawn out of the pipeline, creating a negative pressure that pulls the material from the source to the destination. Both methods rely on the principle of fluid dynamics, where the air acts as a carrier medium, transporting the product efficiently and safely.
Key Components and Their Roles in the System
Effective pneumatic conveying of cereals relies on several critical components, each playing a vital role in the overall operation. These include the hopper or feeder, which controls the flow of material into the system; the pipeline network, which forms the path for transport; the air compressor or vacuum pump, which generates the necessary pressure or vacuum; and the control valves and regulators, which manage the air flow and pressure levels. Additionally, filters and cyclones are used to separate the air from the material, ensuring that the system remains clean and free from dust or debris. Each component is designed to work in harmony, optimizing the performance and efficiency of the entire conveying process.
Benefits of Pneumatic Conveying for Cereal Processing
Implementing pneumatic conveying systems in cereal processing offers numerous advantages. Firstly, it significantly improves operational efficiency by reducing downtime associated with mechanical handling equipment. The absence of moving parts minimizes maintenance needs, leading to lower operational costs over time. Secondly, the system maintains the quality and integrity of the cereal product, as it avoids contact with metal or other materials that could introduce contaminants. This is particularly important for high-value cereals, where product purity is a key selling point. Thirdly, pneumatic conveying allows for flexible and scalable solutions, enabling businesses to adapt to changing production volumes and operational requirements without significant modifications to the system. The technology also enhances safety in the workplace by eliminating the need for manual handling of bulk materials, reducing the risk of accidents and injuries.
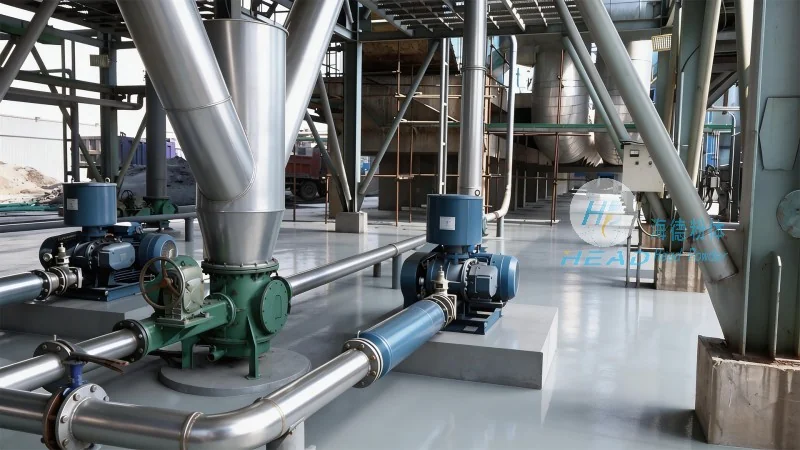
Application Examples in the Cereal Industry
Pneumatic conveying systems are widely used in various stages of cereal processing. For instance, in the production of breakfast cereals, these systems efficiently transport raw grains from storage silos to processing lines, where they are cleaned, sorted, and prepared for further processing. In the packaging stage, pneumatic conveying is used to move finished products from the production line to packaging machines, ensuring a smooth and continuous flow of goods. Additionally, in the storage and distribution of cereals, these systems facilitate the transfer of bulk materials between warehouses and distribution centers, optimizing logistics and reducing handling time. The versatility of pneumatic conveying makes it suitable for a wide range of cereal products, including wheat, oats, corn, and other grains, making it an indispensable tool in modern cereal processing operations.
Conclusion: The Future of Cereal Handling with Pneumatic Conveying
As the cereal industry continues to evolve, the demand for efficient and reliable material handling solutions remains high. Pneumatic conveying systems, with their proven performance and adaptability, offer a sustainable and effective solution for transporting cereals. By understanding the operation process and working principles of these systems, businesses can make informed decisions about implementing or upgrading their material handling infrastructure. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can leverage advanced pneumatic conveying technology to enhance their operational efficiency, maintain product quality, and achieve long-term success in the competitive cereal market.




