HeadPowder, a leading provider of industrial conveying solutions, specializes in advanced pneumatic conveying systems tailored for the efficient handling of bulk materials. This article explores the fundamental principles behind a potassium sulfate pneumatic conveying system, alongside the key operational characteristics that define its effectiveness in various industrial applications. The company, Shandong HeadPowder Engineering Co., Ltd., is based in Shandong, China, and has a strong reputation for delivering reliable and efficient material handling solutions.
Introduction to Potassium Sulfate and Pneumatic Conveying
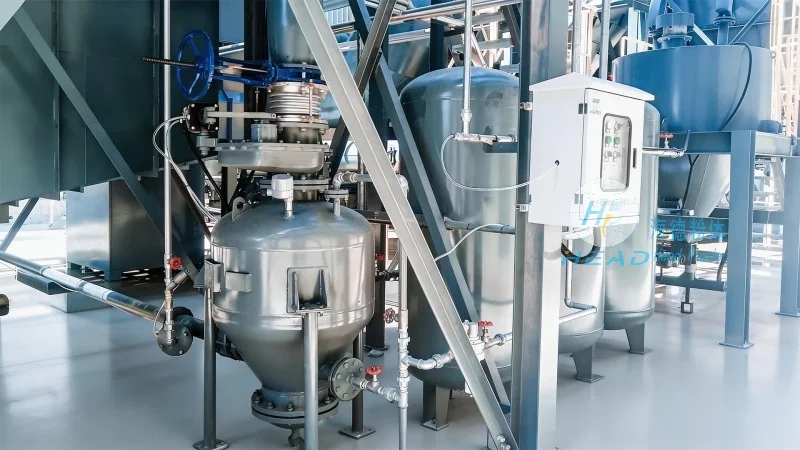
Potassium sulfate, a vital fertilizer and industrial chemical, demands robust and efficient transport methods to maintain its quality and ensure smooth processing. Pneumatic conveying systems offer a versatile and effective solution for moving bulk solids like potassium sulfate, as they eliminate the need for mechanical components that could cause wear, contamination, or material degradation. The system’s design is specifically optimized for the unique properties of potassium sulfate, including its particle size distribution, density, and flow characteristics, ensuring a consistent and reliable conveying process.
Core Principles of Pneumatic Conveying Technology
The operation of a potassium sulfate pneumatic conveying system is grounded in the principle of using compressed air to create a pressure differential that propels material through a pipeline. The system typically comprises several key components: a storage hopper, a feeder to regulate material flow, a conveying line, and a receiver for discharged material. Compressed air is introduced at the inlet of the pipeline, generating a flow that carries the potassium sulfate particles forward. This process can be classified into dilute phase and dense phase conveying, each offering distinct advantages based on the material’s properties and the required conveying distance. Dilute phase systems use higher air velocities and lower material concentrations, suitable for short to medium distances, while dense phase systems employ lower air velocities and higher material concentrations, ideal for longer distances and more delicate materials.
Key Operational Characteristics and Performance Factors
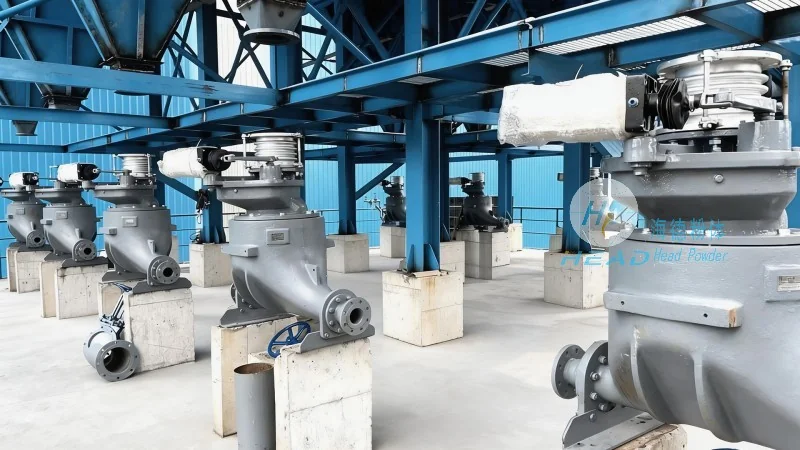
Several operational characteristics are critical to the effectiveness of a potassium sulfate pneumatic conveying system. Firstly, the system’s ability to handle varying particle sizes and moisture content is paramount. Potassium sulfate particles can range from fine powders to coarse granules, and the system must be designed to prevent blockages and maintain uniform flow. The pressure and air flow rate are precisely calibrated to achieve an optimal conveying velocity, preventing material degradation or segregation. Energy efficiency is another key consideration, as pneumatic conveying can be more energy-intensive than other methods. However, modern systems incorporate energy-saving features such as variable speed drives, optimized air flow management, and efficient compressor designs to minimize operational costs. Additionally, the system’s reliability and low maintenance requirements are important factors, as they reduce downtime and operational expenses for industrial facilities.
Workplace Scenarios and Application Examples
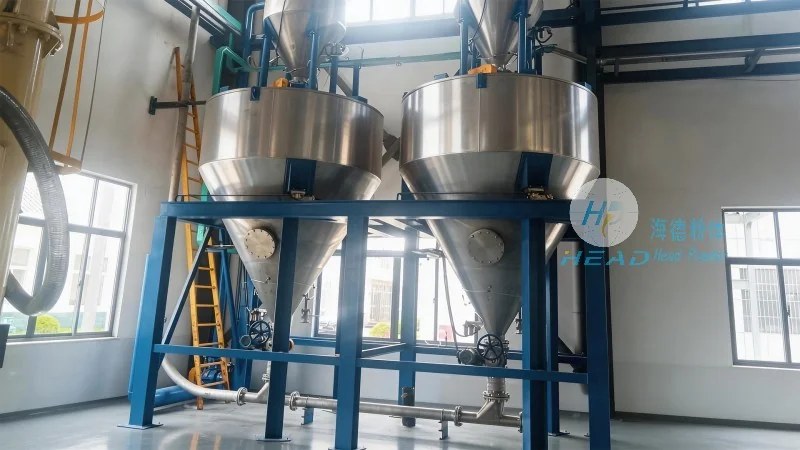
The potassium sulfate pneumatic conveying system is widely utilized in diverse industrial and agricultural settings. In fertilizer production facilities, the system efficiently transports raw potassium sulfate from storage silos to processing units, ensuring a continuous and uninterrupted supply of material for manufacturing. This is crucial for maintaining production schedules and meeting market demands. In large-scale agricultural operations, the system is employed to distribute potassium sulfate as a fertilizer, enabling precise and uniform application across fields. This helps optimize crop yields and improve soil health. Furthermore, in chemical processing plants, the system can transport potassium sulfate to reactors or storage tanks, facilitating its integration into downstream chemical processes. The system’s adaptability to different operational environments, from indoor processing facilities to outdoor storage and distribution sites, highlights its versatility and reliability. Whether used in a manufacturing plant, a farm, or a chemical processing facility, the system’s ability to handle bulk materials efficiently makes it an essential component of modern industrial operations.
Conclusion and Company Expertise
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, has established itself as a trusted leader in the design and implementation of pneumatic conveying systems for potassium sulfate and other bulk materials. The company’s expertise in system engineering, material handling, and process optimization ensures that clients receive customized solutions tailored to their specific operational needs. By leveraging advanced pneumatic conveying principles and incorporating modern technological advancements, HeadPowder delivers systems that enhance productivity, reduce maintenance costs, and improve overall material handling efficiency. The potassium sulfate pneumatic conveying system exemplifies the company’s commitment to providing high-quality, reliable solutions that meet the demands of the industrial sector. With a focus on innovation and customer satisfaction, HeadPowder continues to be a key player in the material handling industry, delivering solutions that drive operational success.




