HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for the dairy industry. This article delves into the fundamental principles of these systems and highlights the key operational characteristics that define their effectiveness in handling powdered milk products.
Principles of Pneumatic Conveying for Powdered Milk
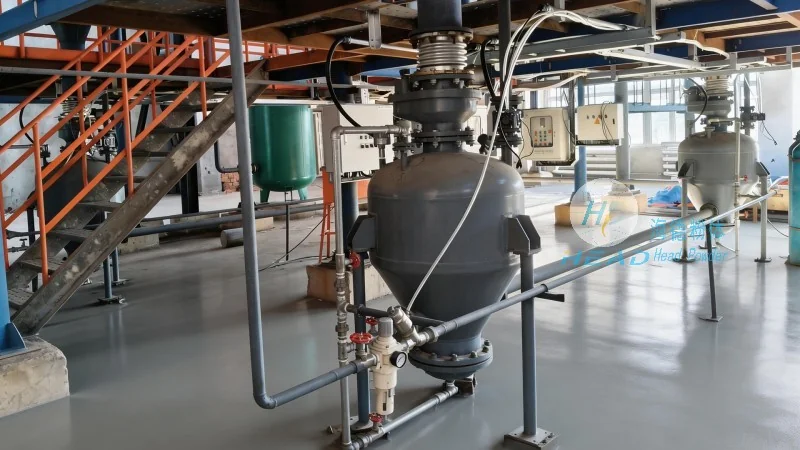
The core principle of pneumatic conveying systems involves the use of air or gas to transport bulk materials, such as powdered milk, through a pipeline. Unlike traditional mechanical conveying methods, which rely on belts, screws, or buckets, pneumatic systems utilize pressure differentials or vacuum to move the material. In the case of powdered milk, this method is particularly advantageous due to the material's fine particle size and sensitivity to moisture and contamination. The system typically consists of a hopper, a feeder, a conveying line, and a receiver. The hopper stores the powdered milk, while the feeder controls the flow rate into the conveying line. Air is introduced into the line, either by a blower or a vacuum pump, creating a flow that carries the powder particles. The design of the system, including the type of air flow (positive or negative pressure) and the pipeline configuration, is critical to ensuring efficient and gentle handling of the product.
Key Operational Characteristics in Working Scenarios
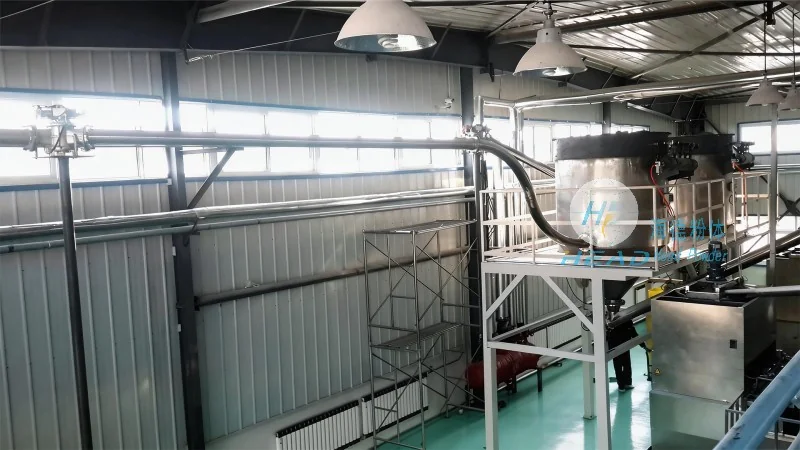
The operational characteristics of a powdered milk pneumatic conveying system are tailored to meet the specific demands of different industrial settings. These characteristics include: efficiency in material transfer, minimal product degradation, and adaptability to varying production volumes. In a typical dairy processing plant, the system may be used to transport powdered milk from storage silos to packaging lines, or to move it between different processing stages. The ability to handle large volumes quickly and with minimal human intervention is a significant advantage. Additionally, the system's ability to maintain product integrity is crucial, as powdered milk is sensitive to temperature changes and mechanical stress. The design often incorporates features like temperature-controlled conveying lines and gentle agitation to prevent agglomeration and ensure the powder remains in a free-flowing state. In scenarios where space is limited, the system's compact design and flexible pipeline layout allow for easy integration into existing plant layouts. The operational flexibility also allows for the integration of multiple conveying lines, enabling the system to handle different product types or to switch between storage and processing areas as needed.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted provider of customized powder handling solutions, including pneumatic conveying systems for the dairy industry. With a focus on innovation and quality, HeadPowder designs systems that meet the stringent requirements of modern dairy processing, ensuring high efficiency, product safety, and operational reliability. The company's expertise lies in understanding the unique challenges of handling powdered milk, such as its hygroscopic nature and the need for sterile processing environments. By leveraging advanced engineering and material science, HeadPowder develops systems that not only enhance productivity but also contribute to the overall quality and safety of the final product.




