

Working Principle and Features of Camellia Seed Pneumatic Conveying Equipment
Camellia seed pneumatic conveying equipment is a specialized system designed for the efficient handling and transportation of camellia seeds. This equipment plays a crucial role in the processing industry, particularly in facilities that deal with the extraction of oil from camellia seeds. Understanding its working principle and key features is essential for optimizing operational efficiency and ensuring the quality of the final product.
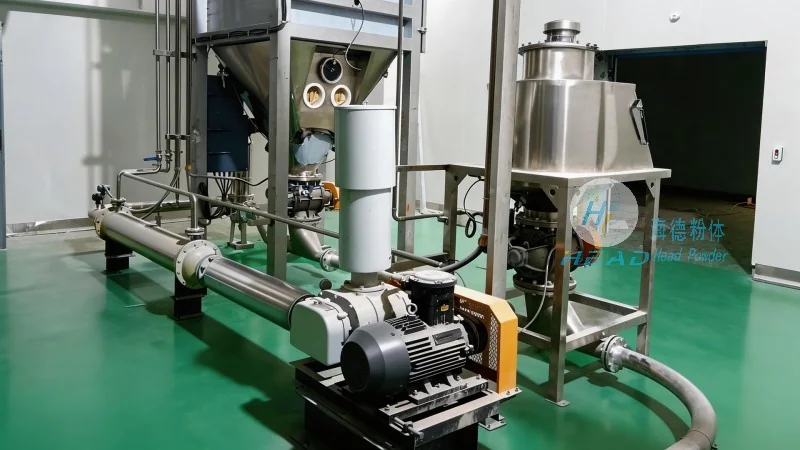
Working Principle of Camellia Seed Pneumatic Conveying Equipment
The core of the camellia seed pneumatic conveying system lies in its ability to transport materials using air pressure. The system typically consists of a hopper, a conveyor line, a fan or blower, and a collection tank. When the camellia seeds are fed into the hopper, the fan generates a flow of air that pulls the seeds along the conveyor line. The air flow creates a negative pressure in the system, which draws the seeds from the hopper and transports them to the collection point. This process eliminates the need for mechanical components like belts or chains, reducing friction and wear. The air velocity is carefully controlled to ensure that the seeds are conveyed without damage, maintaining their integrity for subsequent processing steps such as oil extraction.
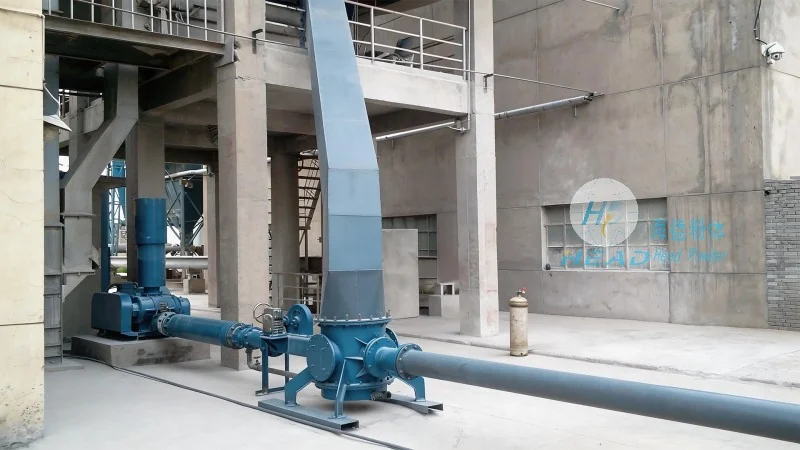
Key Features of Camellia Seed Pneumatic Conveying Equipment
Several notable features distinguish camellia seed pneumatic conveying equipment from other types of material handling systems. First, it offers a high degree of flexibility in terms of layout and installation. The system can be configured to follow the existing workflow in a processing plant, adapting to different spatial constraints. Second, it provides excellent dust control. By using enclosed pipelines and a sealed system, the equipment minimizes the release of dust particles, which is beneficial for maintaining a clean and safe working environment. Third, it ensures minimal product contamination. The air used in the system is filtered, and the conveyor lines are designed to prevent cross-contamination between different batches of camellia seeds. Fourth, it offers energy efficiency. Modern pneumatic conveying systems utilize high-efficiency fans and optimized air flow, reducing energy consumption compared to traditional mechanical conveyors. Additionally, the system is easy to clean and maintain, with removable components that can be sanitized regularly to prevent the buildup of residues or microbial growth.
Operational Advantages and Applications
Implementing camellia seed pneumatic conveying equipment brings several operational advantages. The primary benefit is the reduction in labor costs, as the system automates the material transport process, minimizing the need for manual handling. This also enhances workplace safety by eliminating the risks associated with manual lifting and moving of heavy seed batches. Another advantage is the improved product quality. By preventing mechanical damage and maintaining a controlled environment, the equipment ensures that the camellia seeds retain their natural properties, leading to higher yields of oil and better quality byproducts. The system is particularly suitable for large-scale processing facilities where high throughput is required. It can handle large volumes of seeds continuously, supporting the high production demands of the oil extraction industry. Furthermore, the system's adaptability allows it to be integrated with other processing equipment, such as oil presses or solvent extraction units, creating a seamless production line.
Conclusion and Company Information
Camellia seed pneumatic conveying equipment is a sophisticated solution for the efficient and safe handling of camellia seeds. Its working principle, based on air pressure and enclosed transport, combined with its key features like flexibility, dust control, and energy efficiency, makes it an ideal choice for modern processing facilities. By leveraging this technology, companies can enhance their operational performance, improve product quality, and ensure a safe working environment. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of the camellia seed processing industry. With a focus on innovation and customer satisfaction, the company offers reliable equipment that meets the demands of today's competitive market. HeadPowder's commitment to quality and technical expertise ensures that clients receive systems that are not only efficient but also durable and easy to maintain. Based in Shandong, China, the company leverages its local resources and industry knowledge to deliver solutions that help businesses optimize their operations and achieve their production goals.