For industrial applications that require precise and efficient material handling, the metering bin pump stands out as a critical piece of equipment. This specialized system is designed to handle bulk materials with high accuracy, making it indispensable in sectors such as cement production, chemical processing, and mining. Understanding the functionality and design principles of this equipment is essential for optimizing operational efficiency and ensuring consistent performance in material transport.
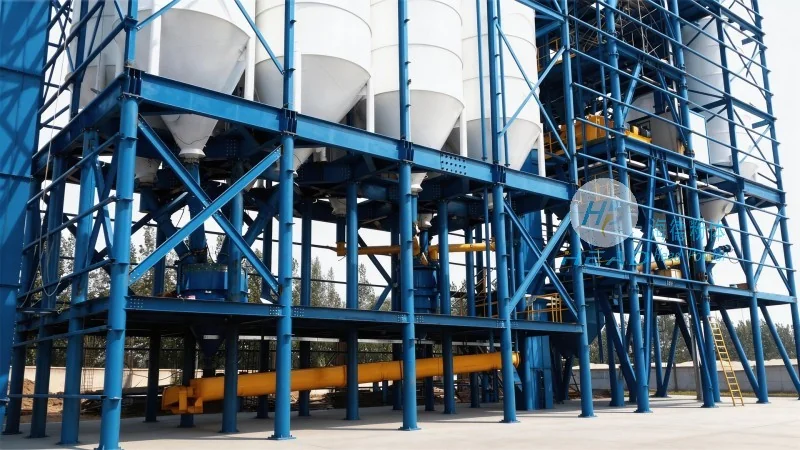
Introduction to Metering Bin Pump Material Handling Equipment
The metering bin pump, often referred to as a bin pump or a metering system, is a type of positive displacement pump that operates by using a hopper to store and feed material into a pump chamber. Unlike traditional conveyor systems, this equipment provides precise control over the flow rate of bulk materials, allowing for accurate dosing and delivery. The core components of a metering bin pump typically include a hopper, a rotary valve or feeder, a pump chamber, and a discharge mechanism. Each component works in tandem to ensure that materials are transferred in a controlled manner, minimizing waste and maximizing productivity.
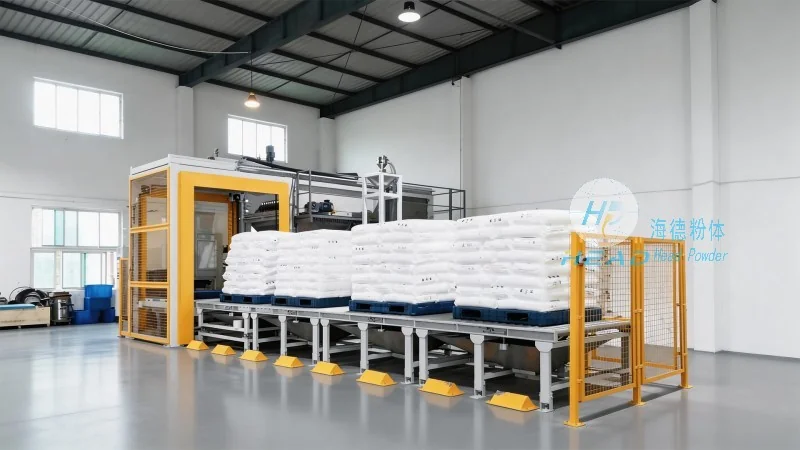
Key Design Principles of Metering Bin Pump Systems
The design of a metering bin pump is centered on several fundamental principles that ensure its effectiveness and reliability. First, the system is engineered to maintain a consistent pressure within the pump chamber, which is crucial for achieving uniform material flow. This is achieved through the use of a pressure relief valve and a check valve that prevent backflow and maintain steady pressure. Second, the equipment incorporates a variable speed drive that allows operators to adjust the pump speed according to the required flow rate. This flexibility is vital for handling different material types and varying production demands. Third, the design emphasizes durability and low maintenance, featuring robust materials such as stainless steel and high-quality seals that can withstand harsh operating conditions. Additionally, the system includes a level sensor and a control panel that enable real-time monitoring and adjustment of the material level in the hopper, ensuring optimal performance.
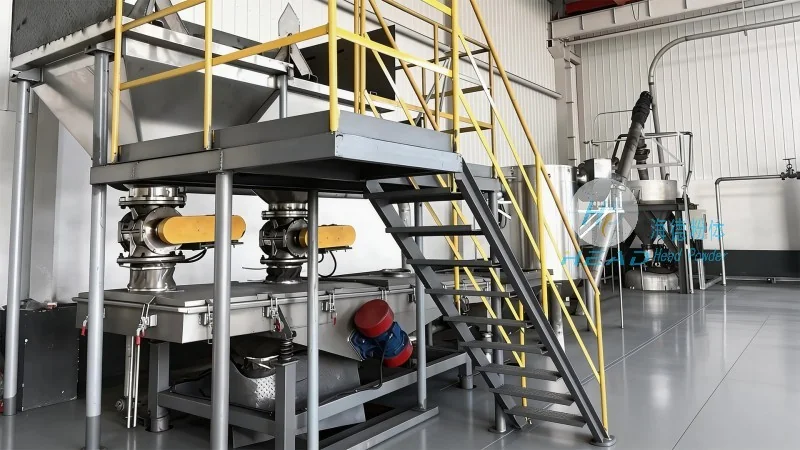
How the Metering Bin Pump Works: A Step-by-Step Overview
The operation of a metering bin pump involves a series of coordinated actions that facilitate the transfer of bulk materials. The process begins with the material being fed into the hopper from a storage silo or bin. As the material accumulates, a level sensor detects the rising level and signals the control system to activate the pump. The feeder, which may be a rotary valve or a screw conveyor, then begins to discharge material into the pump chamber. The pump chamber is equipped with a rotating impeller or plunger that moves the material forward under pressure. As the impeller rotates, it creates a vacuum in the chamber, drawing more material from the hopper. The material is then forced through a discharge line to the destination point, such as a mixer or a storage tank. The entire process is controlled by a programmable logic controller (PLC) that adjusts the pump speed and feeder rate to maintain the desired flow rate. This closed-loop control system ensures that the material is delivered at a consistent rate, regardless of variations in the material's bulk density or the system's load.
Benefits of Using Metering Bin Pump Equipment in Industrial Applications
Implementing a metering bin pump in industrial settings offers numerous advantages that enhance operational efficiency and product quality. One of the primary benefits is the ability to achieve precise material dosing, which is critical in processes that require exact quantities of raw materials, such as in the production of cement or chemical compounds. This precision reduces material waste and minimizes the need for reprocessing, leading to cost savings. Another key advantage is the improved safety and reliability of the system. By eliminating manual handling of bulk materials, the metering bin pump reduces the risk of accidents and exposure to hazardous substances. The automated control system also minimizes human error, ensuring consistent performance over time. Furthermore, the equipment's ability to handle a wide range of materials, from fine powders to coarse granules, makes it versatile for various industrial applications. The low maintenance requirements of the system, combined with its long service life, contribute to overall cost-effectiveness. In summary, the metering bin pump is a valuable asset for industries seeking to optimize material handling while maintaining high standards of accuracy and safety.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of advanced material handling equipment, including metering bin pumps. With its headquarters located in Shandong, China, the company has established itself as a trusted provider of high-quality industrial solutions. HeadPowder specializes in designing and manufacturing equipment that meets the stringent requirements of modern industrial applications, ensuring durability, efficiency, and reliability. The company's commitment to innovation and customer satisfaction has earned it a reputation for excellence in the industry. By leveraging advanced engineering techniques and rigorous quality control processes, HeadPowder delivers products that enhance operational performance and contribute to the success of its clients. Whether for new installations or equipment upgrades, HeadPowder offers tailored solutions that address the specific needs of each customer, providing comprehensive support from design to installation and maintenance.




