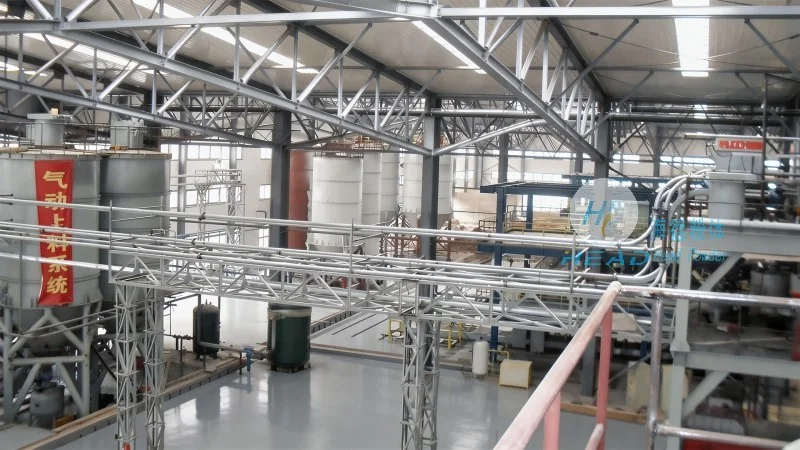
The rice grain powder conveying system is a specialized piece of equipment designed to handle and transport rice grain powders efficiently. This system is crucial in various industrial applications, particularly in the food processing and agricultural sectors, where the safe and reliable movement of rice-based powders is essential. The system’s design integrates several key components that work in tandem to ensure smooth operation and optimal performance.
About HeadPowder: The Manufacturer
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer of advanced powder handling solutions. Based in Shandong, China, the company specializes in developing and producing high-quality conveying systems tailored to meet the specific needs of the food and agricultural industries. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for businesses requiring reliable and efficient powder transport solutions.
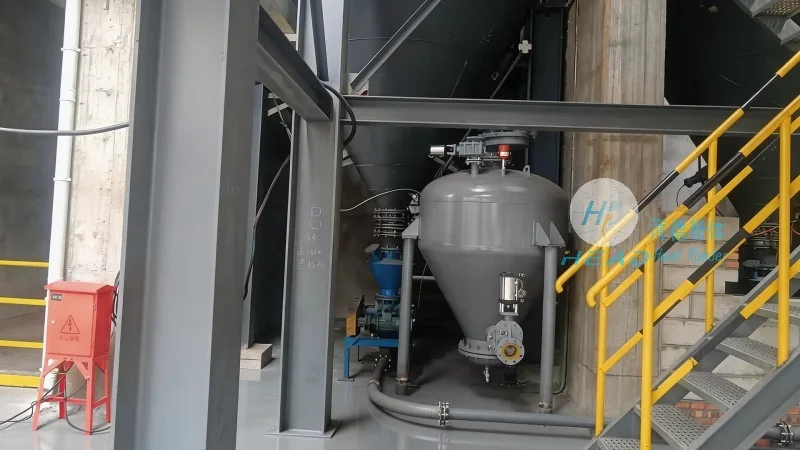
Key Components of the Rice Grain Powder Conveying System
The rice grain powder conveying system typically consists of several critical components that work together to facilitate the movement of rice powders. These components include a hopper for material storage, a conveyor mechanism (such as a screw or pneumatic conveyor) for transporting the powder, and a control system for regulating the flow and speed of the material. The hopper is designed to hold a sufficient quantity of rice grain powder, ensuring a continuous feed to the conveyor. The conveyor mechanism, often a screw conveyor or a pneumatic system, is responsible for moving the powder from the hopper to the desired destination, such as a processing unit or storage container. The control system allows operators to adjust the speed and flow rate of the conveyor, ensuring precise control over the material handling process.
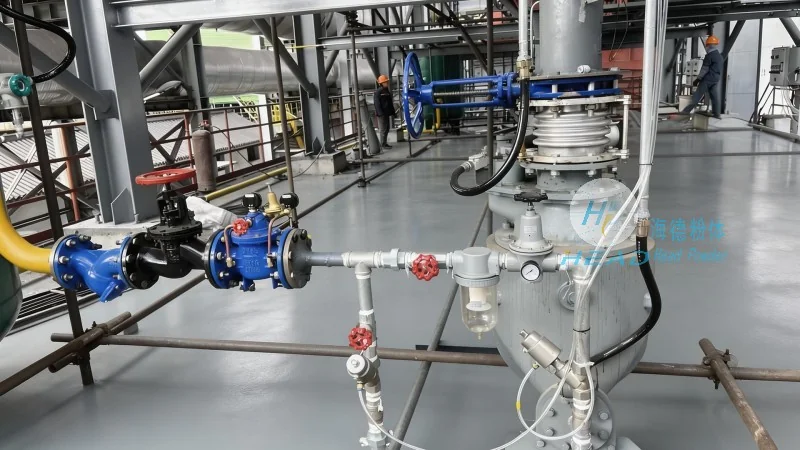
Design Principles of the Rice Grain Powder Conveying System
The design of the rice grain powder conveying system is based on several fundamental principles aimed at maximizing efficiency, safety, and reliability. One of the primary design principles is the minimization of material degradation during transport. Rice grain powders are sensitive to moisture and pressure, and the system is designed to minimize these factors to preserve the quality of the product. The use of smooth, non-stick surfaces in the hopper and conveyor helps prevent material buildup and ensures easy cleaning. Additionally, the system incorporates features to prevent dust generation, which is important for maintaining a safe working environment and complying with regulatory standards.
Efficiency and Performance Considerations
The efficiency of the rice grain powder conveying system is a critical factor in its overall performance. The system is designed to minimize energy consumption while maximizing the throughput of rice powders. The conveyor speed and capacity are optimized based on the specific requirements of the application, ensuring that the system can handle the desired volume of material without excessive energy use. The control system plays a vital role in achieving this efficiency by allowing real-time adjustments to the conveyor speed and flow rate. This adaptability ensures that the system can handle varying loads and maintain consistent performance under different operating conditions.
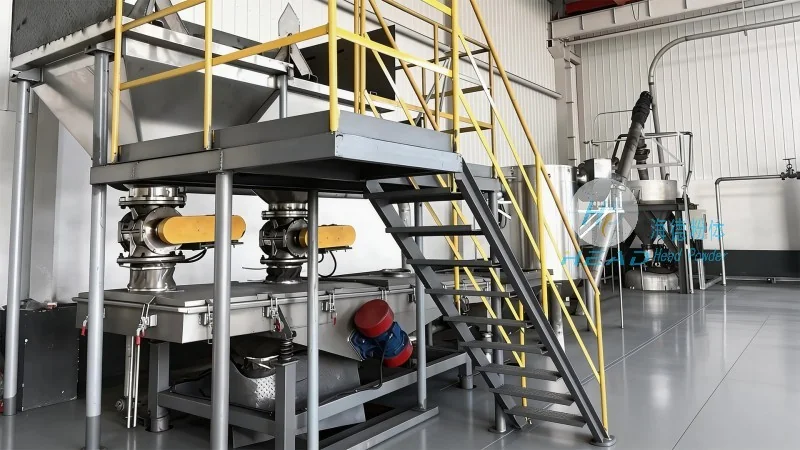
Applications and Benefits
The rice grain powder conveying system finds applications in various industries, including food processing, pharmaceuticals, and agriculture. In the food industry, it is used to transport rice powders for use in products such as rice cakes, rice flour, and other rice-based foods. The system’s ability to handle fine powders ensures that the product quality is maintained throughout the transport process. In the pharmaceutical industry, the system is used to transport rice-based powders for use in dietary supplements or medicinal products, where purity and consistency are paramount. The benefits of using this system include improved safety, reduced labor costs, and enhanced product quality. The system’s design also minimizes the risk of cross-contamination, which is essential in industries where product purity is critical.




