For industries dealing with gravel and powder materials, efficient material handling is crucial. A gravel powder conveying system equipment is a specialized solution designed to transport these materials from one location to another with precision and reliability. This equipment is essential for optimizing workflow and ensuring consistent material flow in various industrial applications.
Understanding the Gravel Powder Conveying System Equipment
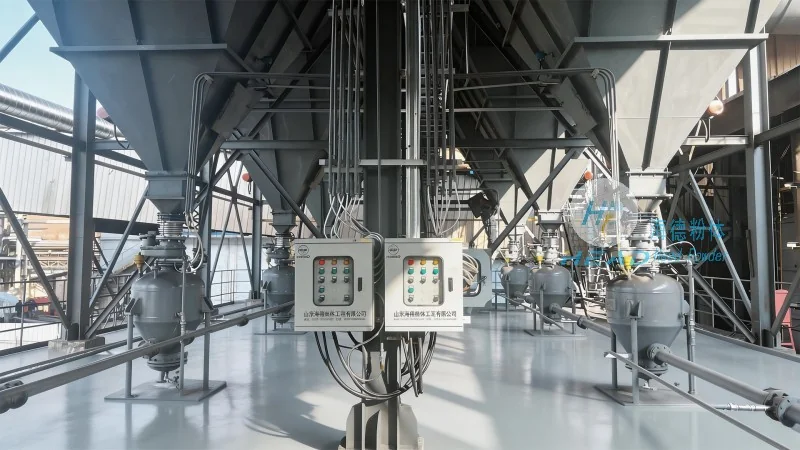
The gravel powder conveying system equipment, often referred to as a bulk material handling system, is engineered to handle the transportation of granular and powdery substances like gravel, sand, and other similar materials. These systems are designed to meet the specific needs of different industries, including construction, mining, and manufacturing, by providing a reliable and efficient means of moving bulk materials.
Key Components and Design Principles
The design of a gravel powder conveying system equipment is based on several fundamental principles to ensure optimal performance. Key components typically include a hopper for material storage, a conveyor mechanism (such as a screw conveyor or belt conveyor), and a control system for regulating the flow. The system is engineered to handle the physical properties of gravel and powder, including particle size, density, and moisture content, to prevent blockages and ensure smooth operation.
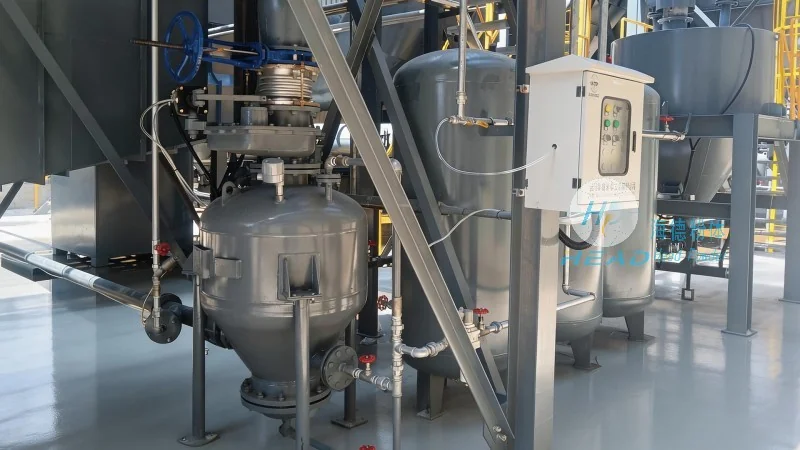
One of the critical design principles is the use of appropriate materials for the construction of the conveying components. This includes using corrosion-resistant materials for parts that come into contact with the materials being transported, ensuring durability and longevity. Additionally, the system incorporates features like adjustable speed controls and variable feed mechanisms to adapt to different material loads and processing requirements.
How the System Works: A Step-by-Step Overview
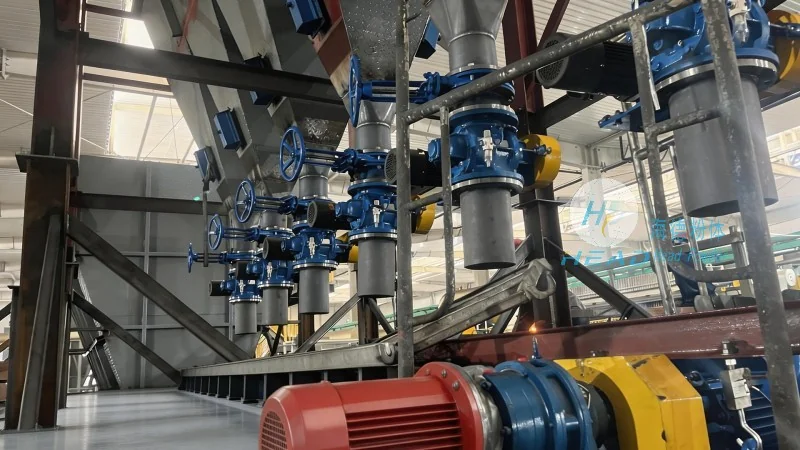
The operation of a gravel powder conveying system equipment involves several steps to ensure efficient material transfer. First, the material is fed into the hopper from a storage silo or other source. The hopper then feeds the material into the conveyor mechanism, which transports it to the discharge point. The control system monitors the flow rate and adjusts the conveyor speed as needed to maintain a consistent output. This process ensures that the material is moved in a controlled manner, minimizing waste and maximizing productivity.
Applications and Benefits in Industrial Settings
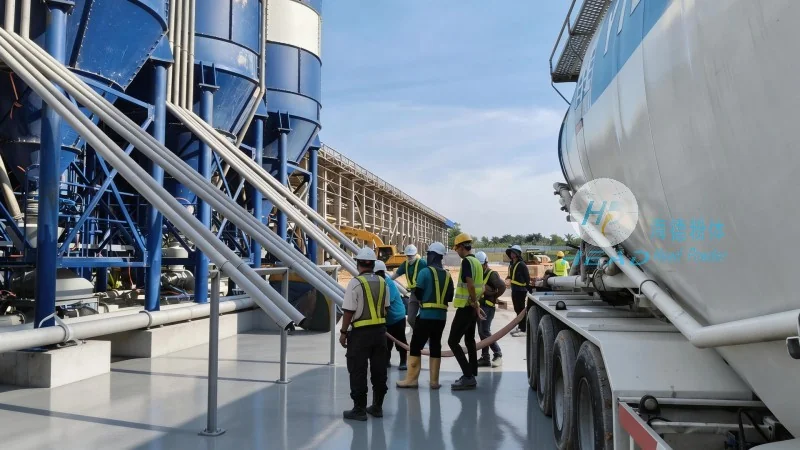
Gravel powder conveying systems are widely used in various industrial settings due to their versatility and efficiency. In construction projects, these systems are used to transport gravel and sand to different parts of the site, facilitating the building process. In mining operations, they help in the transport of ore and other materials from the extraction site to processing facilities. The benefits of using such systems include increased productivity, reduced labor costs, and improved safety by minimizing manual handling of bulk materials.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of gravel powder conveying system equipment. With a focus on innovation and quality, the company has established itself as a trusted provider of bulk material handling solutions. HeadPowder's products are designed to meet the highest industry standards, ensuring reliability and durability in demanding environments. The company's headquarters is located in Shandong, China, where it continues to develop and refine its equipment to meet the evolving needs of its clients.




