For those working in the mining industry, understanding the technology behind powder handling systems is crucial. A mine powder conveying system equipment is a specialized setup designed to transport bulk powders efficiently and safely within mining operations. This equipment is essential for moving materials like ore, rock dust, and other fine particles from one location to another, supporting various stages of mining processes from extraction to processing.
Understanding the Core Components of Mine Powder Conveying Systems
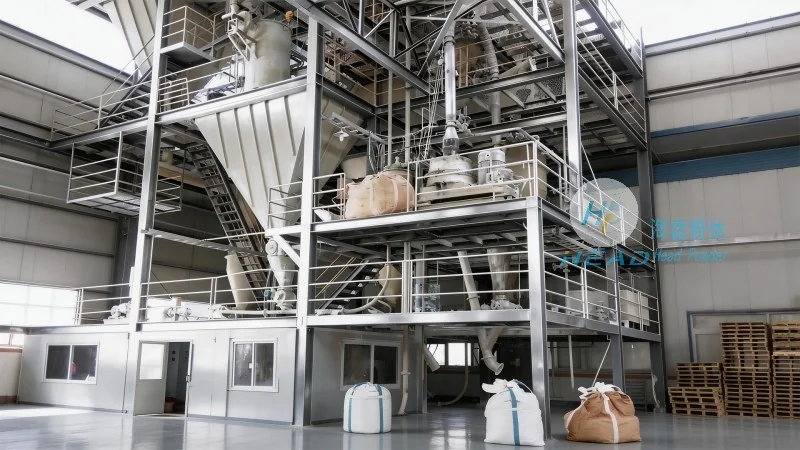
The heart of any mine powder conveying system lies in its components, each playing a vital role in the overall operation. Key elements typically include a feeding mechanism to introduce the material into the system, a conveyor or transport medium (such as a belt, pipeline, or pneumatic system), and a control system to regulate the flow and speed. The feeding mechanism ensures consistent material input, preventing blockages or uneven flow. The conveyor itself can vary in type—gravity-based systems use the material's weight to move it, while mechanical systems rely on motors and pulleys. Pneumatic systems, on the other hand, use compressed air to push or pull the powder through pipes, offering flexibility in layout and reduced risk of dust exposure.
Design Principles Behind Efficient Mine Powder Conveying
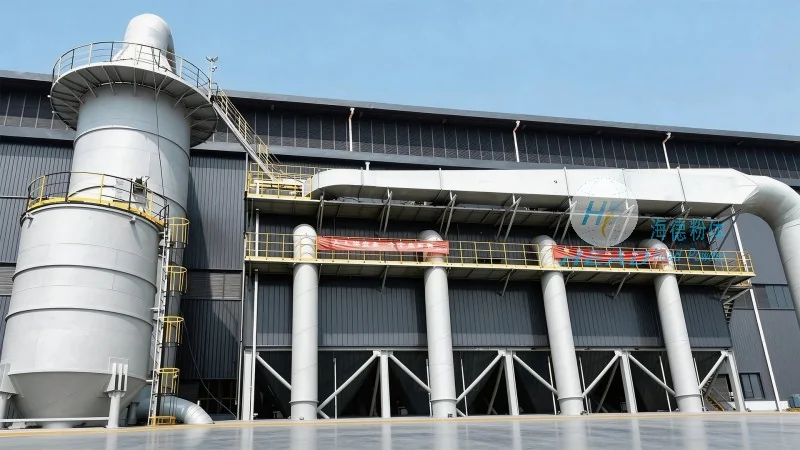
The design of a mine powder conveying system is guided by several critical principles aimed at maximizing efficiency, safety, and durability. One primary principle is the minimization of material degradation during transport. This involves selecting appropriate materials for the conveyor components—such as food-grade or corrosion-resistant materials—to prevent contamination or wear from abrasive powders. Another key principle is the prevention of dust generation and explosion risks, which are significant hazards in mining environments. Designers incorporate dust suppression systems, explosion-proof components, and proper ventilation to mitigate these risks. Additionally, the system must be designed for scalability and adaptability, allowing it to handle varying material types and quantities as mining operations evolve.
How Shandong HeadPowder Engineering Co., Ltd. Enhances Mine Powder Conveying Solutions
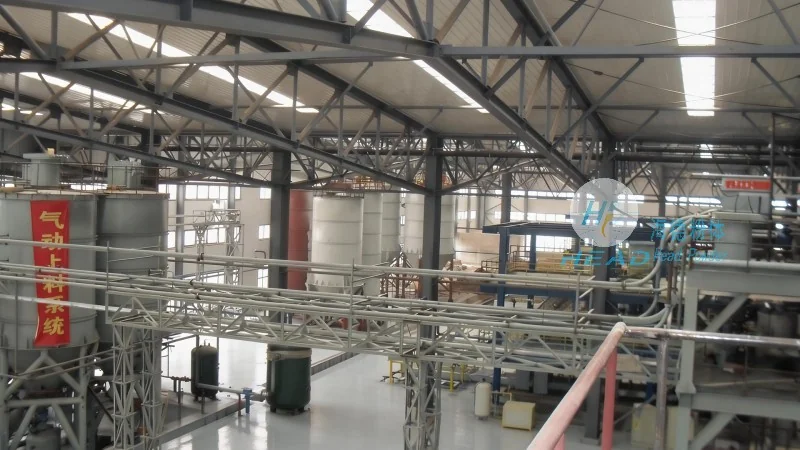
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in developing tailored solutions for mine powder conveying systems. With a strong presence in China, the company leverages years of industry experience to address the unique challenges faced by mining operations. Their approach focuses on integrating advanced technology with practical engineering solutions, ensuring that each system is optimized for the specific needs of the client. By collaborating closely with clients, HeadPowder engineers assess operational requirements, material characteristics, and site constraints to design systems that meet both performance and safety standards. The company’s commitment to quality and innovation has made it a trusted partner for mining companies seeking reliable and efficient powder handling solutions.
Key Considerations for Implementing Mine Powder Conveying Systems
When implementing a mine powder conveying system, several factors must be carefully considered to ensure optimal performance and longevity. First, the type of material being transported is critical. Different powders have varying properties—such as density, moisture content, and particle size—which influence the choice of conveyor type and design. For example, cohesive or sticky powders may require specialized feeding mechanisms to prevent agglomeration, while lightweight powders might need higher airflow in pneumatic systems. Second, the layout of the mining site and the distance between source and destination points impact system design. Horizontal and vertical transport requirements dictate the use of inclines, elevators, or vertical conveyors. Third, regulatory compliance and safety standards must be adhered to, as mining operations are subject to strict environmental and occupational health regulations. HeadPowder’s expertise in these areas helps clients navigate these considerations effectively, ensuring that their systems not only meet operational needs but also comply with industry standards.
Conclusion: The Importance of Advanced Mine Powder Conveying Systems
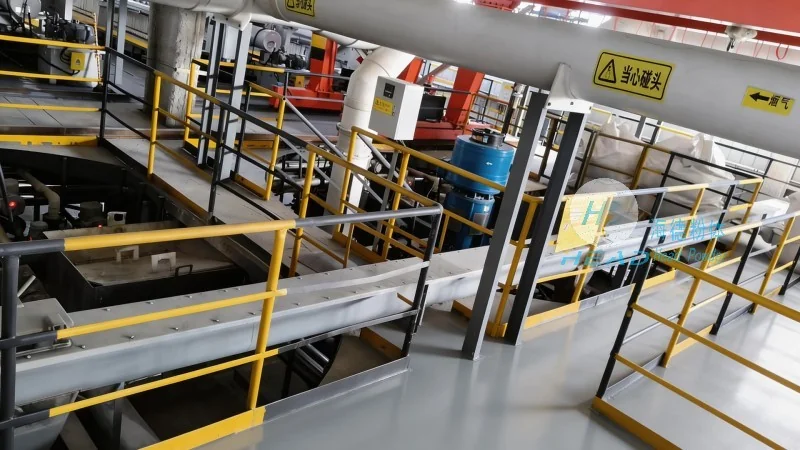
In conclusion, mine powder conveying system equipment is a vital component of modern mining operations, enabling efficient material handling while maintaining safety and environmental standards. The design principles behind these systems—focused on efficiency, durability, and safety—ensure they can withstand the demanding conditions of mining environments. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in advancing this technology by providing customized solutions that address the unique challenges of each mining project. As mining operations continue to evolve, the importance of reliable and effective powder conveying systems will only grow, making them an indispensable part of the industry's future.




