What is a Dry Powder Bulk Material Conveyor? And What Are Its Design Principles?
Release time:2026-09-15 17:01:20
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
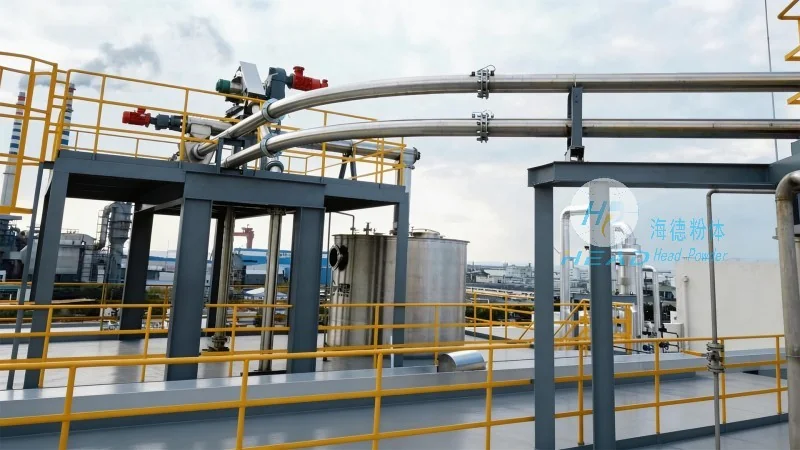
When it comes to handling dry powders and bulk materials in industrial settings, the dry powder bulk material conveyor is a critical piece of equipment. These systems are designed to transport dry materials such as powders, granules, and other bulk solids efficiently and reliably. Understanding the functionality and design principles of such conveyors is essential for optimizing material handling processes in various industries.
Understanding the Core Function of Dry Powder Conveyors
The primary function of a dry powder bulk material conveyor is to transport dry materials from one location to another within a processing facility. These conveyors are engineered to handle a wide range of dry powders, including chemicals, food products, pharmaceuticals, and industrial minerals. The ability to move these materials without degradation or contamination is a key advantage of dry powder conveyors.
Key Design Principles of Dry Powder Bulk Material Conveyors
The design principles of dry powder bulk material conveyors revolve around several critical factors. First, the system must ensure minimal material degradation during transport. This is achieved through the use of low-friction components and gentle material handling mechanisms. Second, the conveyor must maintain material integrity and prevent segregation or agglomeration. This is often accomplished through the use of enclosed or semi-enclosed designs that control airflow and material flow.
Technical Specifications and Operational Features
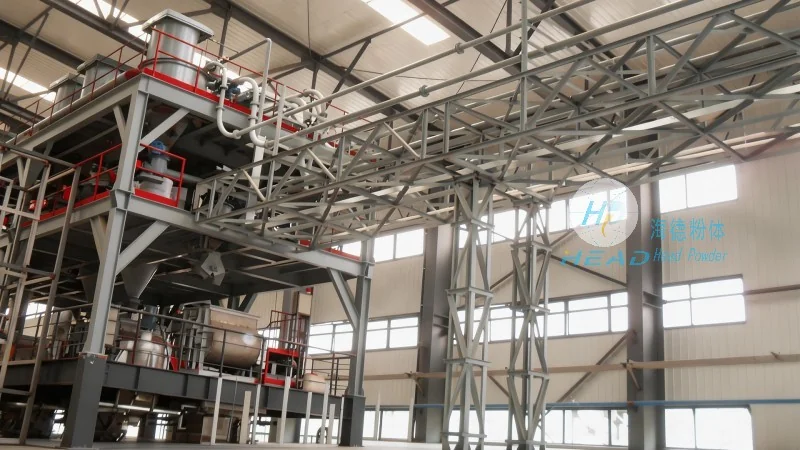
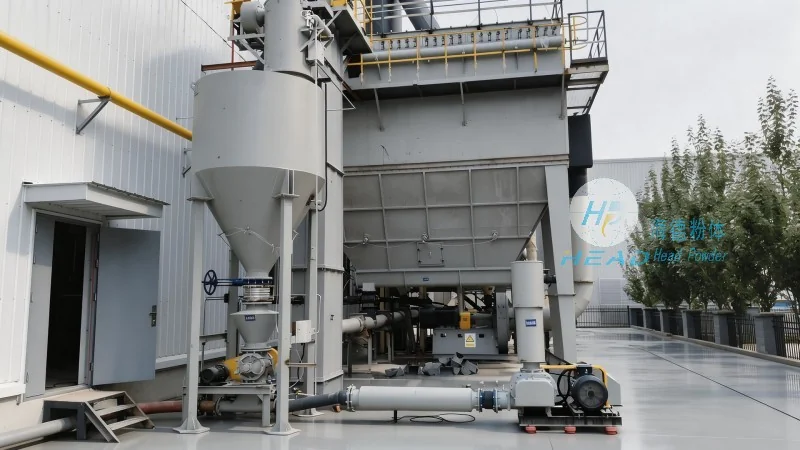
Technical specifications of dry powder conveyors vary based on the specific application and material being handled. Common features include adjustable speed controls, variable flow rates, and the ability to handle different particle sizes and densities. Many models also incorporate features such as dust collection systems and material discharge mechanisms that ensure safe and efficient operation. Operational features may include automated start-up and shutdown sequences, as well as monitoring systems for material levels and system performance.
Applications and Industry Use Cases
Dry powder bulk material conveyors are widely used across multiple industries. In the chemical industry, they are used to transport raw materials and finished products. In the food and pharmaceutical sectors, these conveyors are essential for maintaining product purity and preventing contamination. The mining and mineral processing industries also rely on dry powder conveyors to transport raw ores and processed materials. Additionally, in the agricultural sector, these systems are used to handle fertilizers and other dry agricultural products.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of dry powder bulk material conveyors and related equipment. With a focus on innovation and quality, the company has established itself as a trusted provider of industrial material handling solutions. HeadPowder's products are designed to meet the specific needs of various industries, ensuring efficient and reliable material transport. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research and development center.




