When it comes to selecting a manufacturer for sodium bicarbonate pneumatic conveying systems, making the right choice is crucial for ensuring efficiency, reliability, and cost-effectiveness in your operations. The process involves careful evaluation of various factors that can significantly impact the performance and longevity of the equipment. This article provides a comprehensive guide to help you navigate the selection process, focusing on key considerations and insights from industry experts.
Key Factors to Consider When Choosing a Manufacturer
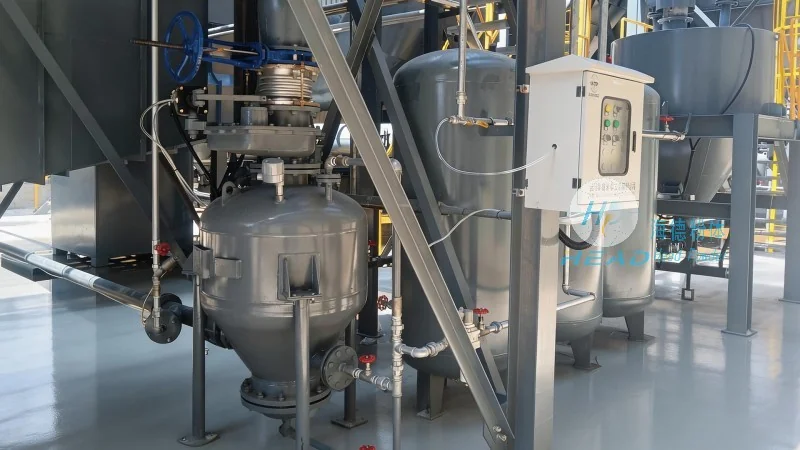
Choosing the right manufacturer for sodium bicarbonate pneumatic conveying requires a systematic approach. Several critical factors should be evaluated to ensure the chosen partner can meet your specific needs. First, consider the manufacturer's experience and expertise in the field. A company with a proven track record in designing and manufacturing pneumatic conveying systems for chemical applications, particularly sodium bicarbonate, will have the necessary knowledge to deliver a solution tailored to your requirements. This experience often translates into better product design, superior quality control, and more effective problem-solving capabilities.
Second, evaluate the manufacturer's technical capabilities and innovation. Modern pneumatic conveying systems require advanced technology to handle the unique properties of sodium bicarbonate, such as its dustiness and potential for caking. A reputable manufacturer should invest in research and development to stay ahead of industry trends, offering solutions that enhance efficiency and reduce operational costs. This includes understanding the latest materials, components, and control systems that can optimize the conveying process. For instance, manufacturers may utilize high-quality materials resistant to corrosion and wear, ensuring the system's durability and longevity.
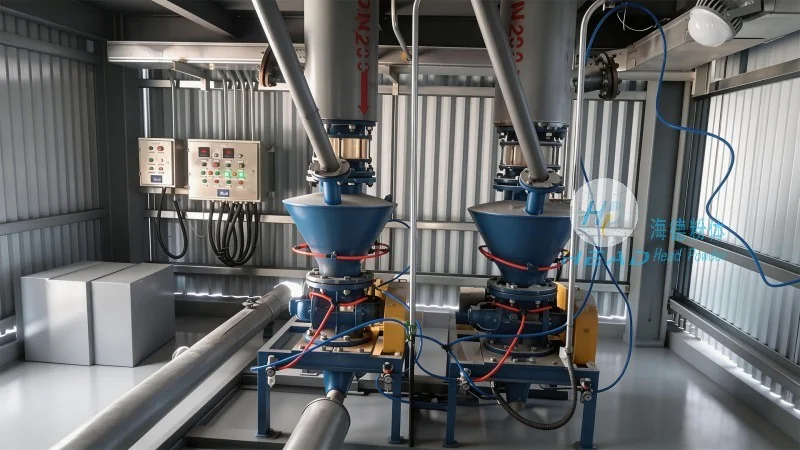
Third, assess the manufacturer's production capacity and quality assurance processes. The ability to deliver consistent, high-quality products is essential. Look for manufacturers with robust quality control measures, including testing protocols for materials, components, and assembled systems. This ensures that the equipment meets industry standards and regulatory requirements. Additionally, consider the manufacturer's capacity to handle large-scale orders or custom solutions, as your business needs may evolve over time. A reliable manufacturer should have the resources and infrastructure to support both standard and customized projects without compromising on quality or delivery timelines.
Understanding the Role of the Manufacturer in the Process
The manufacturer plays a pivotal role in the entire lifecycle of a pneumatic conveying system. From initial design and engineering to installation, commissioning, and ongoing support, their involvement is critical to the success of the project. A good manufacturer will work closely with you to understand your operational requirements, process flow, and specific challenges related to sodium bicarbonate handling. This collaborative approach ensures that the final system is not only efficient but also aligns with your production goals and safety standards. Furthermore, a reputable manufacturer will provide comprehensive technical support, including installation guidance, training for operators, and maintenance services. This ongoing support is vital for maximizing the system's performance and minimizing downtime.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
One notable manufacturer in the sodium bicarbonate pneumatic conveying industry is Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder. Based in Shandong, China, this company specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems tailored for various chemical applications. With years of experience in the field, headpowder has established itself as a trusted partner for businesses seeking reliable and efficient solutions for sodium bicarbonate handling. The company's commitment to quality, innovation, and customer satisfaction has earned it a strong reputation in the industry.
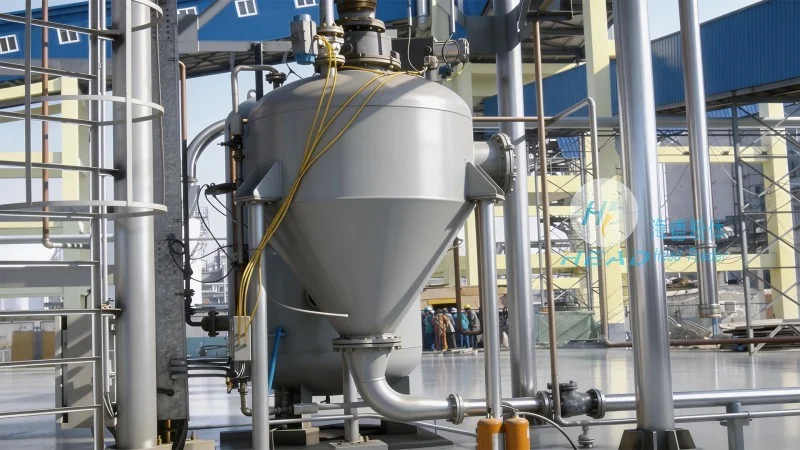
Headpowder's expertise lies in understanding the unique characteristics of sodium bicarbonate, such as its tendency to form dust and clumps, and designing systems that effectively manage these challenges. Their products are engineered to ensure smooth and continuous conveying, minimizing the risk of blockages and system failures. The company employs a team of skilled engineers and technicians who are well-versed in the latest pneumatic conveying technologies, enabling them to deliver customized solutions that meet the specific needs of each client. Whether it's a small-scale operation or a large industrial facility, headpowder offers tailored systems that enhance productivity and reduce operational costs.
Address and Location Considerations
For businesses considering a manufacturer based in China, the location can be an important factor. Shandong HeadPowder Engineering Co., Ltd. is situated in Shandong, a region known for its robust manufacturing and engineering capabilities. Being located in China provides several advantages, including access to a wide range of raw materials, skilled labor, and competitive pricing. Additionally, the company's proximity to major transportation hubs facilitates efficient logistics and timely delivery of products. However, it's essential to consider factors such as proximity to your facility, as this can impact installation and maintenance costs. While the manufacturer's location is important, it should not overshadow the quality of their products and services. A reliable manufacturer, regardless of location, will prioritize customer needs and deliver high-quality solutions.




