Ammonium sulfate, a widely used industrial chemical, often requires efficient and reliable transportation methods for its handling and distribution. Pneumatic conveying systems have emerged as a preferred solution for moving this material, offering advantages such as reduced dust generation, improved safety, and enhanced process control. This article explores the types, key features, and diverse applications of ammonium sulfate pneumatic conveying, providing insights into how these systems optimize material handling in various industrial settings.
Types of Ammonium Sulfate Pneumatic Conveying Systems
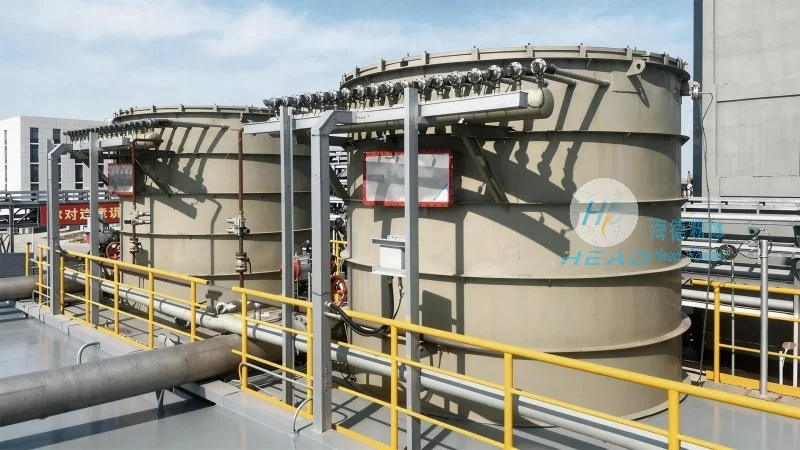
There are primarily two main categories of pneumatic conveying systems used for ammonium sulfate: dilute-phase and dense-phase systems. Each type offers distinct characteristics suited to different operational requirements.
Dilute-phase pneumatic conveying involves the transport of material in a low concentration of solid particles suspended in air. This method is suitable for long-distance and high-capacity applications, where the material is moved at relatively high velocities. The system typically uses positive pressure to push the material through the pipeline, making it efficient for continuous operations. Dense-phase pneumatic conveying, on the other hand, transports material in a higher concentration of solid particles, often with air or gas used to create a plug flow. This approach is ideal for handling materials that are sensitive to high velocities or for applications requiring precise control over the material's flow rate. The choice between dilute-phase and dense-phase systems depends on factors like the material's properties, the distance to be covered, and the desired flow rate.
Key Features of Ammonium Sulfate Pneumatic Conveying
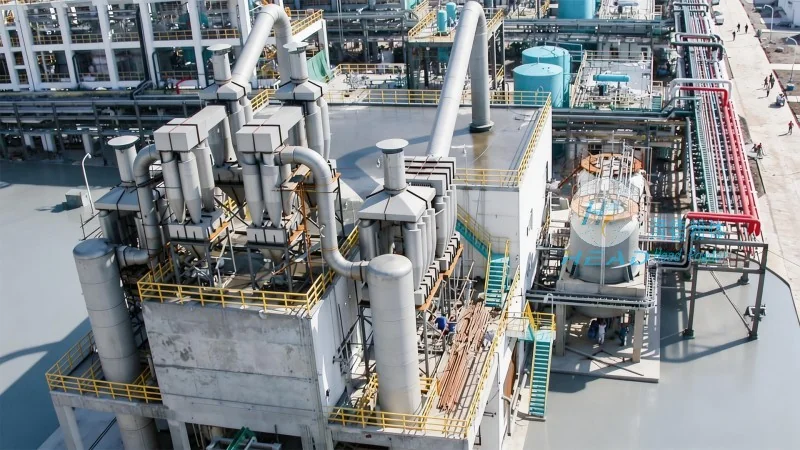
Several key features make ammonium sulfate pneumatic conveying an attractive option for industrial applications. First, the system minimizes dust exposure, which is crucial for maintaining a safe working environment and complying with environmental regulations. Ammonium sulfate is a fine powder, and traditional handling methods can generate significant dust, posing health risks and contamination issues. Pneumatic conveying reduces this risk by containing the material within a sealed system, preventing dust from escaping into the air. Second, the technology offers high efficiency in material transport, with the ability to handle large volumes of material over long distances with minimal energy consumption compared to other methods like belt conveyors or bucket elevators. Third, the system provides excellent control over the material's flow, allowing for precise dosing and batching, which is essential in processes where accurate material measurement is critical. Additionally, pneumatic conveying systems are relatively compact and can be easily integrated into existing industrial setups, reducing installation costs and space requirements.
Applications of Ammonium Sulfate Pneumatic Conveying
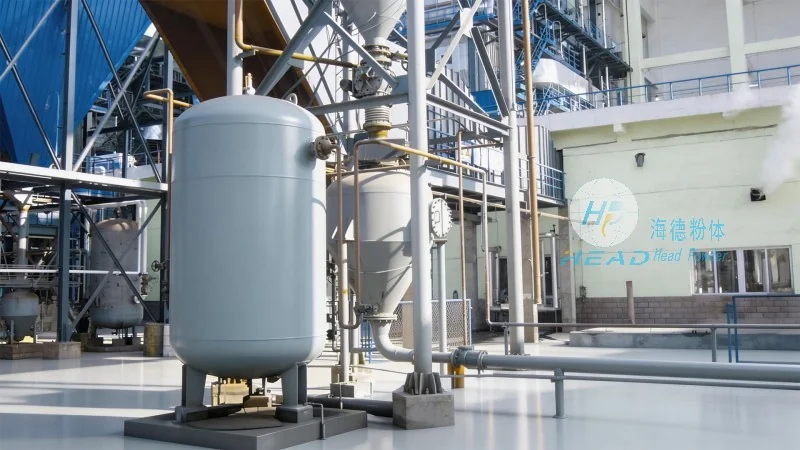
Ammonium sulfate pneumatic conveying systems find applications across various industries, primarily in chemical manufacturing, agriculture, and food processing. In chemical plants, these systems are used to transport ammonium sulfate from storage silos to processing units, ensuring a continuous supply of raw material for production. The systems are also employed in fertilizer manufacturing, where ammonium sulfate is a key component in nitrogen-based fertilizers. The ability to handle large volumes and maintain consistent flow rates is vital in this sector, as it directly impacts the efficiency of fertilizer production. In the agricultural industry, pneumatic conveying is used to transport ammonium sulfate from storage facilities to agricultural fields or to processing plants that convert it into other agricultural products. The system's ability to handle bulk materials efficiently supports the large-scale operations typical of agriculture. Furthermore, in the food processing industry, ammonium sulfate is used as a food additive, and pneumatic conveying ensures that the material is handled hygienically and safely, adhering to strict food safety regulations. The systems are designed to prevent contamination and maintain the purity of the material, which is essential for food applications.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for material handling and processing. With a focus on innovative and efficient systems, HeadPowder specializes in designing and manufacturing pneumatic conveying equipment tailored to the needs of various industries. The company's expertise lies in understanding the unique challenges of handling materials like ammonium sulfate, ensuring that their systems are robust, reliable, and compliant with industry standards. HeadPowder's commitment to quality and customer satisfaction has established it as a trusted partner in the industry, offering customized solutions that enhance operational efficiency and safety. Based in Shandong, China, HeadPowder leverages its local expertise and resources to deliver high-quality products and services to clients worldwide.




