Quartz stone powder conveying systems are vital in industrial operations that manage fine particulate materials. These systems are engineered to efficiently transport quartz stone powders from one location to another, ensuring consistent flow and minimizing material loss. The core of such systems lies in their ability to handle the unique properties of quartz stone, including its high hardness, chemical inertness, and fine particle size. Understanding the underlying principles is essential for optimizing material handling across various industrial applications.
Working Principle of Powder Conveying Equipment
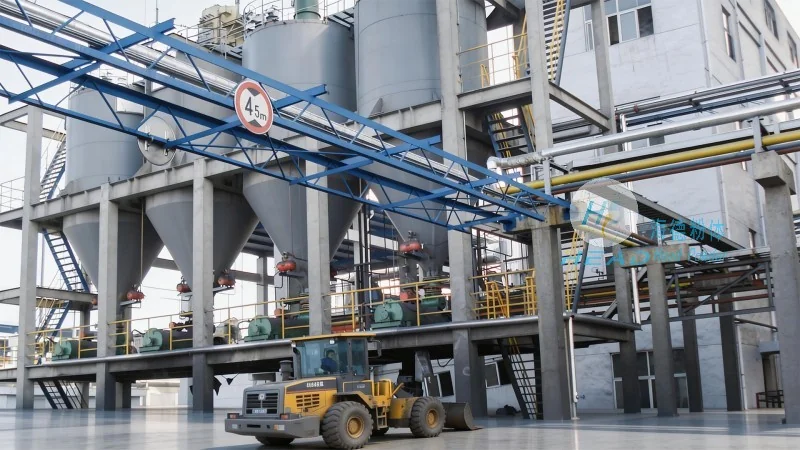
The working principle of quartz stone powder conveying systems typically involves several key components and mechanisms. A common approach is pneumatic conveying, where compressed air or other gases move the powder through a pipeline. This method is particularly effective for fine powders like quartz stone, as it reduces friction and minimizes material degradation. Alternatively, mechanical conveying methods such as screw conveyors, belt conveyors, or bucket elevators may be used, depending on the specific application requirements. The choice of method depends on factors like particle size distribution, moisture content, and the distance over which the material needs to be transported.
Key Components and Their Functions
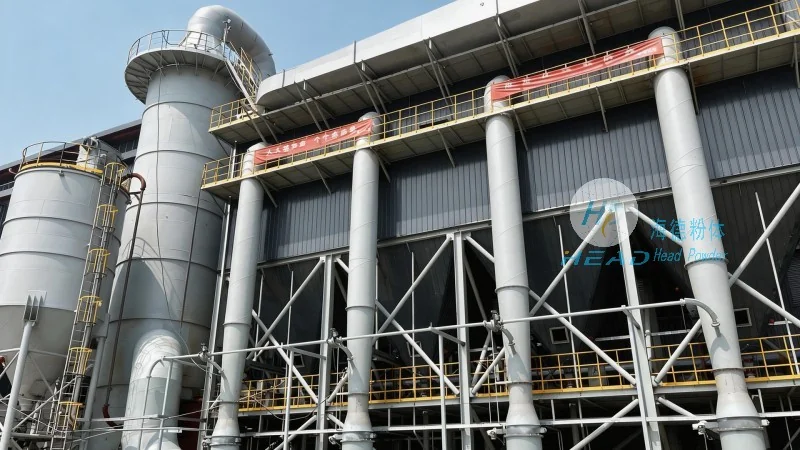
Quartz stone powder conveying systems consist of critical components that work together to ensure smooth operation. These include a hopper for material storage, a feeder to control flow rate, a conveying line (pneumatic or mechanical), and a receiver for discharged material. The hopper is designed to hold sufficient quartz stone powder, often with a conical or rectangular shape to facilitate uniform discharge. The feeder, which may be a rotary valve or screw feeder, regulates material entering the conveying line, preventing overloading and ensuring consistent flow. The conveying line is made of materials resistant to quartz stone's abrasiveness, such as stainless steel or special alloys, to minimize wear. The receiver, typically a container or silo, collects the conveyed powder and may include a dust collection system to maintain air quality and prevent environmental contamination.
Working Scene Characteristics and Applications
The working scene characteristics of quartz stone powder conveying systems vary based on industrial applications. For example, in quartz-based product manufacturing like countertops or tiles, the system must handle large volumes of fine powder with precision, maintaining uniform particle size and preventing agglomeration to ensure final product quality. In the chemical industry, where quartz stone serves as a filler or catalyst support, the system must ensure powder is free from contaminants and has consistent moisture content, critical for final product performance. In mining and processing, the system may need to handle larger particles or higher volumes, requiring robust components and higher power input. Dust control measures are also essential due to the hazardous nature of inhaled quartz stone powders, necessitating proper ventilation and filtration for workplace safety.
Advantages and Practical Considerations
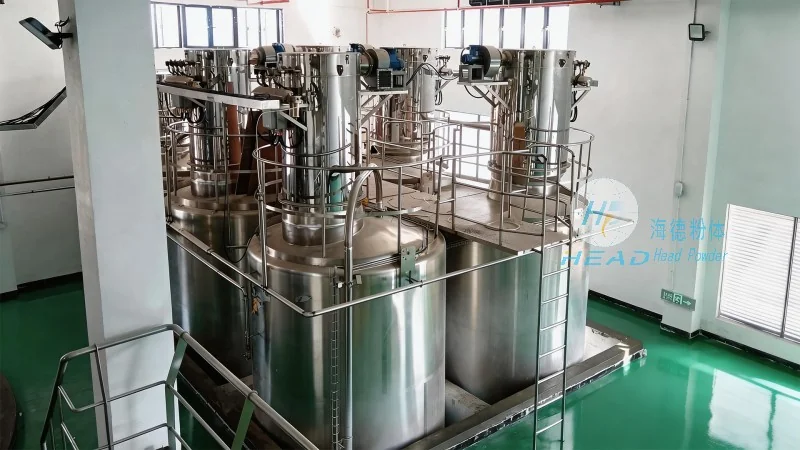
Implementing quartz stone powder conveying systems offers significant advantages in industrial settings. These include efficient fine powder handling without manual labor, reducing labor costs and enhancing workplace safety. The systems minimize material loss and contamination, leading to higher product quality and less waste. Customization for space and operational needs provides flexibility. However, considerations include the abrasive nature of quartz stone causing component wear, requiring regular maintenance and part replacement. Dust explosion risks may demand explosion-proof components and proper ventilation. Installation and maintenance costs are also factors to weigh. Overall, the advantages make these systems a valuable investment for industries reliant on consistent, efficient fine particulate material handling.




