HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing efficient and reliable solutions for stone material conveying. This article explores the fundamental principles behind stone material conveying systems and highlights the key characteristics of their working environments.
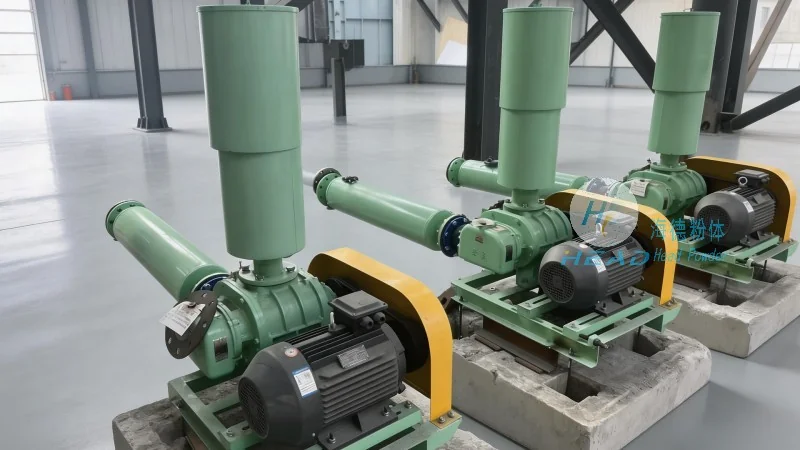
Understanding the Core Principles of Stone Material Conveying
Stone material conveying systems are designed to transport aggregates, such as gravel, crushed stone, and sand, from one location to another with precision and efficiency. The primary principles involve mechanical force, gravity, and controlled movement to ensure the material is moved without damage or loss. These systems typically utilize components like conveyor belts, rollers, and hoppers to facilitate the flow of materials. The design of the system is tailored to the specific properties of the stone, including its size, weight, and abrasiveness, to optimize performance and longevity.
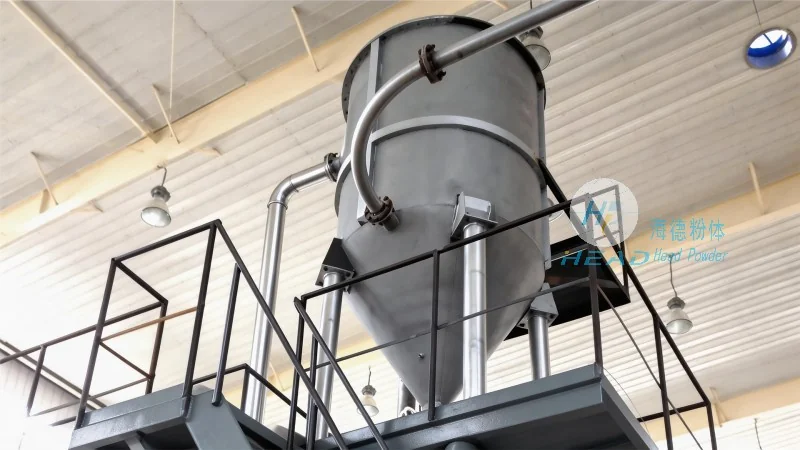
Key Working Scene Characteristics of Stone Material Conveying
The working environments for stone material conveying are diverse and often demanding. These scenes are typically found in construction sites, mining operations, and industrial processing facilities. The characteristics of these environments include high-volume material handling, exposure to harsh weather conditions, and the need for continuous operation. In construction sites, the system must be able to handle varying sizes of aggregates and adapt to changing work conditions. In mining operations, the conveying system must be robust enough to withstand heavy loads and abrasive materials. Industrial processing facilities require precise control over the material flow to ensure consistent quality in the final products.
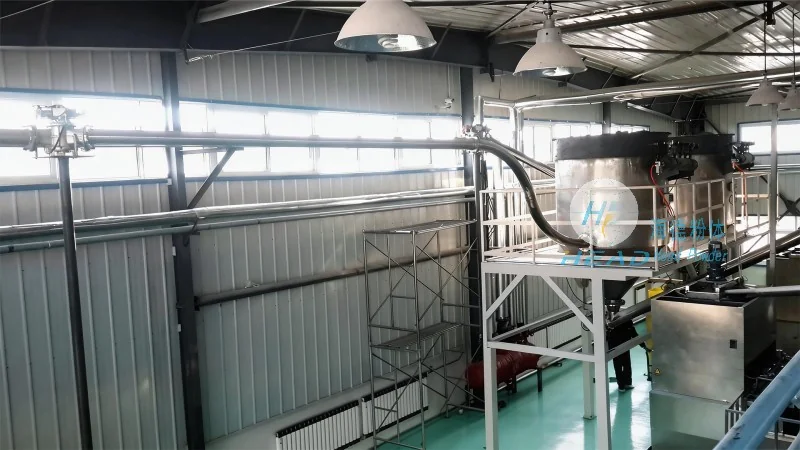
HeadPowder's Expertise in Stone Material Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. leverages advanced engineering and manufacturing techniques to develop customized stone material conveying solutions. The company's products are designed to meet the specific needs of different industries, ensuring optimal performance and durability. By understanding the unique challenges of each working scene, HeadPowder provides tailored systems that enhance productivity and reduce operational costs. The company's commitment to quality and innovation has made it a trusted partner for businesses in the stone and construction sectors.
Applications and Benefits of Stone Material Conveying Systems
Stone material conveying systems are widely used in various applications, including road construction, building projects, and industrial manufacturing. The benefits of these systems include increased efficiency in material handling, reduced labor costs, and improved safety in the workplace. By automating the transportation of aggregates, businesses can streamline their operations and focus on other critical tasks. The systems also help in maintaining consistent material quality, which is essential for high-standard construction projects. HeadPowder's solutions are designed to deliver these benefits while ensuring compliance with industry standards and regulations.
Conclusion: The Importance of Effective Stone Material Conveying
In conclusion, stone material conveying systems play a crucial role in modern construction and industrial operations. The principles and characteristics of these systems are essential for achieving efficient and reliable material handling. HeadPowder, with its expertise and commitment to quality, offers top-tier solutions that meet the diverse needs of its clients. By investing in advanced stone material conveying systems, businesses can enhance their productivity, reduce costs, and ensure the success of their projects. The working scenes and applications of these systems highlight their importance in various industries, making them an indispensable part of modern infrastructure development.




