Intermittent powder pneumatic conveying equipment is a specialized system designed for the efficient and reliable transport of bulk powders through pneumatic means. This technology plays a crucial role in various industrial applications where the safe and controlled movement of dry materials is essential. The equipment operates by using compressed air to create a flow that propels the powder from a source to a destination, ensuring minimal product degradation and contamination.
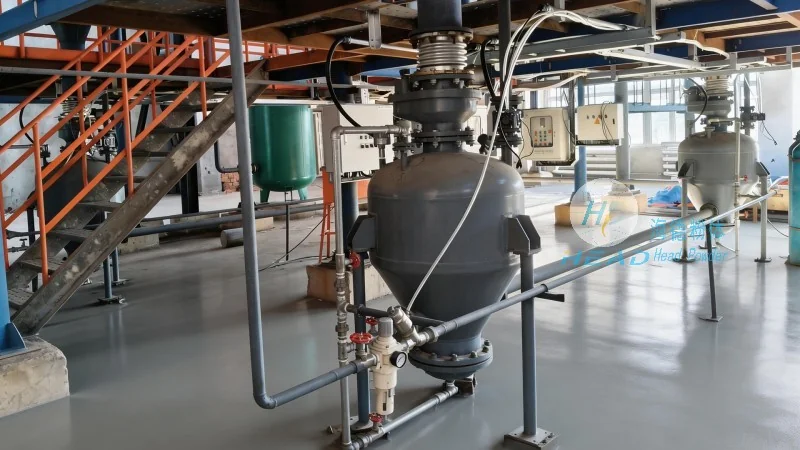
Basic Principle of Intermittent Powder Pneumatic Conveying
The core principle of this equipment involves the intermittent release of powder into a conveying line under controlled conditions. Unlike continuous systems, the intermittent method allows for precise control over the quantity and timing of material discharge. This approach helps in managing issues such as clogging, pressure fluctuations, and material segregation, which are common in continuous pneumatic conveying. The system typically includes a hopper or feeder that holds the powder, a venturi or other air injection device that creates the conveying air flow, and a receiver or discharge point where the material is deposited.
Key Components and Their Functions
Several critical components make up an intermittent powder pneumatic conveying system. The hopper or feeder is responsible for storing and metering the powder, ensuring a consistent feed rate. The venturi or air injection device generates the necessary air pressure and velocity to move the powder particles. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the powder and air mixture. The receiver or discharge unit collects the material at the end of the line, and sometimes includes a dust collection system to maintain air quality and prevent environmental contamination.
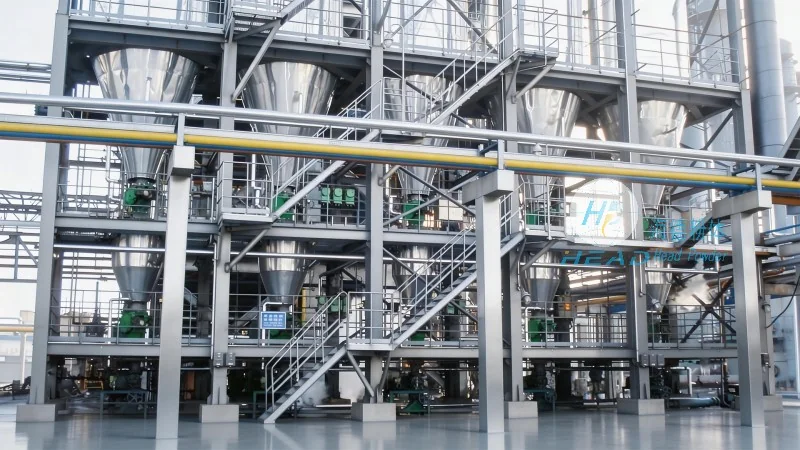
Working Scene Characteristics and Application Scenarios
The working scene characteristics of intermittent powder pneumatic conveying equipment are tailored to specific industrial needs, offering advantages in various operational environments. One of the primary characteristics is its ability to handle a wide range of powder types, from fine powders to bulkier granules, with minimal degradation. This makes it suitable for applications in pharmaceuticals, food processing, and chemical manufacturing where product quality is paramount. Another key characteristic is the system's adaptability to different distances and layouts, allowing for flexible installation in factories or plants. The intermittent operation also provides better control over the conveying process, reducing the risk of overpressurization or underpressurization, which can affect material flow and equipment longevity.
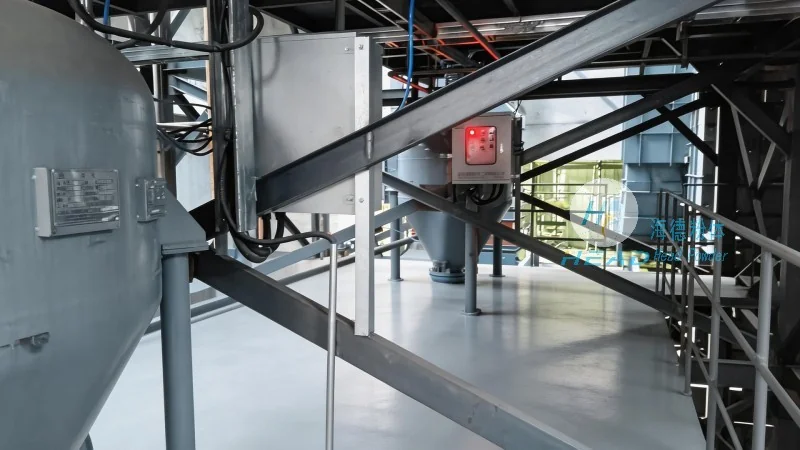
Advantages in Specific Industrial Environments
In industrial settings, the intermittent powder pneumatic conveying equipment offers several advantages that enhance operational efficiency and product safety. For instance, in pharmaceutical manufacturing, the system's ability to maintain sterile conditions and prevent cross-contamination is critical. The equipment's design allows for easy cleaning and maintenance, ensuring compliance with regulatory standards. In food processing, the use of stainless steel components and air filtration systems helps in meeting hygiene requirements. Additionally, the system's energy efficiency, as it only operates when material is being conveyed, reduces operational costs compared to continuous systems that run continuously.
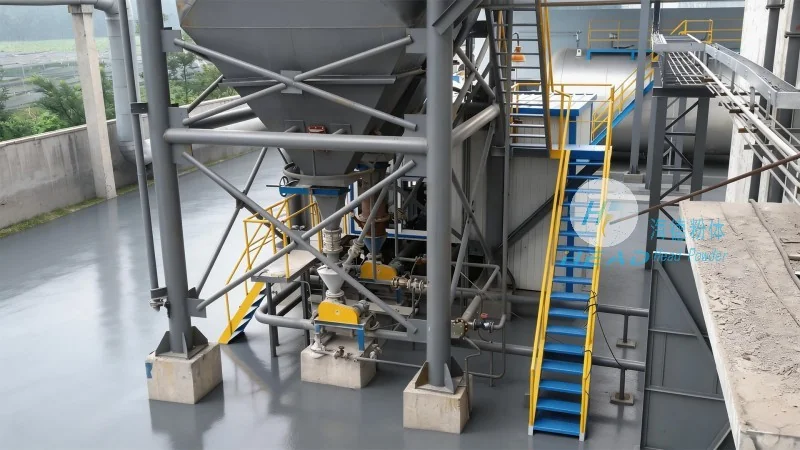
Operational Considerations and Best Practices
When operating intermittent powder pneumatic conveying equipment, several considerations are essential to ensure optimal performance and longevity. Proper maintenance, such as regular cleaning of the hopper, venturi, and conveying line, is crucial to prevent clogging and maintain air flow efficiency. Monitoring air pressure and flow rates is also important to detect any issues early and adjust the system as needed. Additionally, selecting the appropriate air velocity and powder feed rate is vital to prevent material degradation and ensure smooth conveying. Following manufacturer guidelines for material compatibility and system sizing is another best practice to maximize the equipment's effectiveness and safety.
Conclusion: The Role of Intermittent Powder Pneumatic Conveying in Modern Industry
Intermittent powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. represents a reliable solution for the transport of bulk powders in various industrial applications. By understanding its principles, components, and working scene characteristics, industries can leverage this technology to improve operational efficiency, maintain product quality, and ensure compliance with safety and regulatory standards. The equipment's adaptability and control features make it a valuable asset in sectors such as pharmaceuticals, food processing, and chemicals, where the handling of dry materials requires precision and reliability.




