HeadPowder, a leading provider in the field of dust-free powder pneumatic conveying systems, specializes in delivering advanced solutions that ensure efficient, clean, and reliable material handling. Based in Shandong, China, the company has established itself as a trusted partner for industries requiring precise and contamination-free powder transport. This article explores the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in modern industrial applications.
Understanding the Core Principles of Dust-Free Pneumatic Conveying
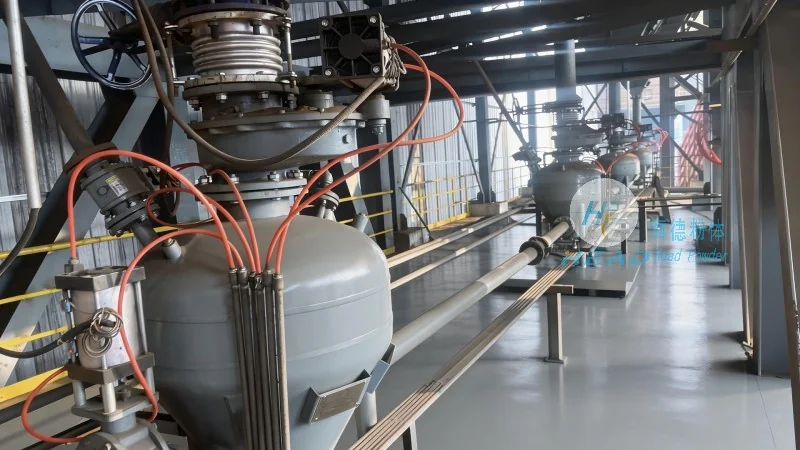
The fundamental principle of dust-free powder pneumatic conveying systems is the use of compressed air or gas to transport dry powders through a closed pipeline system. Unlike traditional mechanical conveying methods, which often involve direct contact with equipment and potential contamination, pneumatic systems operate by suspending particles in a flowing air stream. This suspension mechanism allows for a clean and efficient transfer of powders, minimizing the risk of dust accumulation and cross-contamination. The system typically consists of a blower, a hopper for material storage, a pipeline network, and a discharge point. The compressed air is introduced at the inlet, creating a pressure differential that propels the powder particles through the system. Key to the "dust-free" aspect is the sealed design of the pipeline and the use of filtration at the discharge point to capture any residual particles, ensuring that the environment remains clean and compliant with industry standards.
Key Working Scene Characteristics and Applications
HeadPowder's dust-free pneumatic conveying systems are designed to meet the diverse needs of various industries, each with unique requirements for material handling. The following working scene characteristics illustrate the versatility and effectiveness of these systems:
1. Pharmaceutical and Food Industries: In sectors where product purity and hygiene are paramount, such as pharmaceutical manufacturing and food processing, the dust-free design of the system is critical. The sealed pipeline prevents contamination from external sources, and the filtration at the discharge point ensures that no particles escape into the environment. This is essential for maintaining product quality and adhering to stringent regulatory standards. The system's ability to handle sensitive powders without agglomerating or degrading makes it ideal for applications like drug formulation, where consistency and purity are non-negotiable.
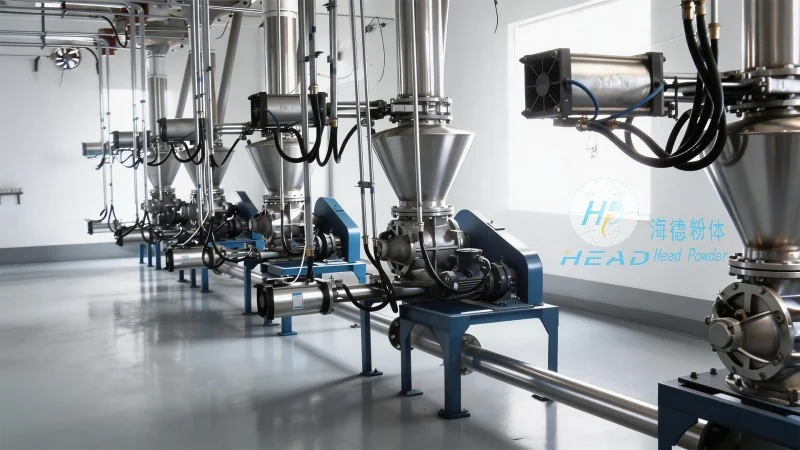
2. Chemical and Petrochemical Industries: For handling hazardous or reactive powders, the dust-free pneumatic conveying system offers enhanced safety. The enclosed system prevents dust explosions and ensures that the material is contained within the pipeline. The use of appropriate materials for the pipeline and components (such as stainless steel or specialized coatings) further reduces the risk of corrosion or chemical reactions. This is particularly important in petrochemical plants where the handling of powders like catalysts or additives requires both efficiency and safety.
3. Mineral Processing and Mining: In the mining and mineral processing sector, large volumes of bulk powders need to be transported over long distances. The pneumatic conveying system provides a high-capacity solution that is more efficient than traditional belt or bucket elevators. The ability to handle abrasive materials without causing wear and tear on the equipment is a significant advantage. Additionally, the system's ability to operate in harsh environments, with robust construction and minimal maintenance requirements, makes it suitable for mining operations where reliability is crucial.
4. Coating and Powder Coating Industries: The need for consistent and uniform powder distribution in coating processes drives the use of dust-free pneumatic conveying. The system ensures that the powder is delivered to the coating line with minimal variation in particle size and moisture content. This leads to improved coating quality and reduced waste. The sealed design also prevents the powder from being exposed to air, which can affect its properties and shelf life. HeadPowder's systems are often customized to handle specific coating powders, such as epoxy or polyester, ensuring optimal performance in the coating process.
Advantages and Technical Features
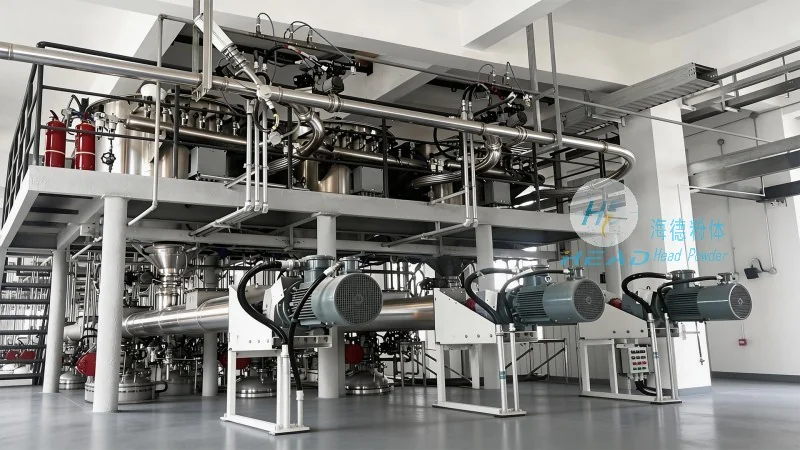
HeadPowder's dust-free pneumatic conveying systems offer several advantages that make them a preferred choice for industries requiring precise material handling. These include:
- High Efficiency and Capacity: The system can handle large volumes of powder at high speeds, reducing processing time and increasing overall productivity. The use of compressed air allows for rapid transport, making it suitable for time-sensitive applications.
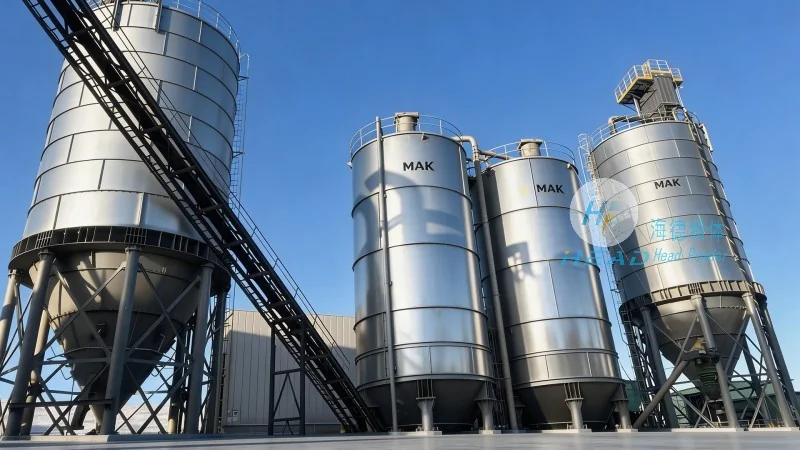
- Minimal Maintenance: The sealed design and lack of moving parts in the pipeline reduce the need for frequent maintenance. This leads to lower operational costs and less downtime for the system.
- Clean and Safe Operation: The dust-free design eliminates the risk of dust explosions and cross-contamination, ensuring a safe working environment. The filtration system at the discharge point captures any residual particles, maintaining air quality and compliance with environmental regulations.
- Customization and Flexibility: HeadPowder offers customized solutions tailored to the specific needs of each client. This includes adjustments to the pipeline layout, material handling capacity, and control systems to meet the unique requirements of different industries and applications.




