Micro silica powder, also known as fumed silica, is a high-purity, fine-grained material widely used in various industrial applications such as construction, rubber, and electronics. The efficient and reliable transportation of this delicate powder is crucial for maintaining product quality and operational efficiency. Pneumatic conveying systems have emerged as a preferred solution for handling micro silica powder due to their ability to minimize dust generation and ensure safe, clean transport. This article provides an in-depth exploration of the working principle and key features of micro silica powder pneumatic conveying equipment, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
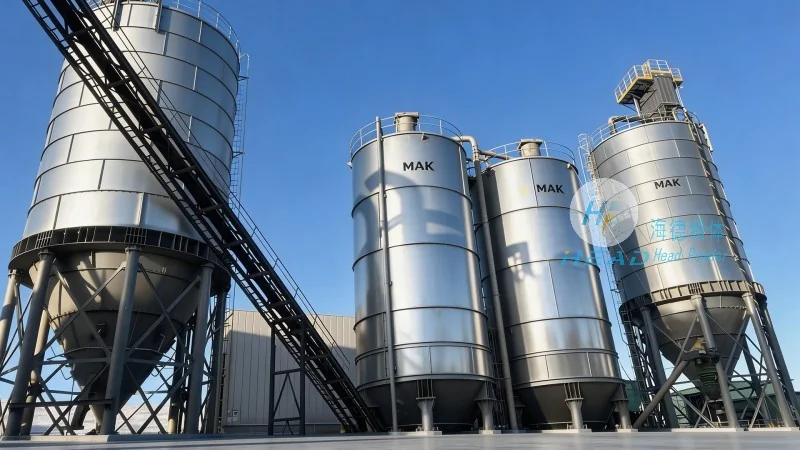
Introduction to Micro Silica Powder Pneumatic Conveying Systems
Micro silica powder is characterized by its extremely fine particle size, typically ranging from 0.01 to 100 microns, and high surface area. These properties make it highly susceptible to agglomeration and dust formation during handling. Traditional methods like bucket elevators or belt conveyors often result in significant dust emissions and product degradation. Pneumatic conveying systems, on the other hand, utilize air to transport the powder through a sealed pipeline system, offering a dust-free and hygienic solution. The equipment is designed to handle the unique challenges posed by micro silica powder, ensuring minimal loss and maximum product integrity.
Working Principle of the Pneumatic Conveying Equipment
The core working principle of a micro silica powder pneumatic conveying system involves the use of compressed air or vacuum to create a flow that moves the powder particles through a network of pipes. There are two primary modes of operation: suction (or vacuum) conveying and pressure (or positive) conveying. In suction conveying, a vacuum is created at the material inlet to draw the powder into the system. The powder is then mixed with air and transported to the discharge point. In pressure conveying, compressed air is used to push the powder through the pipeline from a storage silo or hopper. Both methods rely on the interaction between the air flow and the powder particles to achieve efficient transport.
Key components of the system include the material feed hopper, which holds the micro silica powder; the air supply unit (either a vacuum pump or a compressed air compressor); the conveying line (typically made of stainless steel or other corrosion-resistant materials to prevent contamination); and the separation and filtration system. The separation unit, often a cyclone or a bag filter, separates the powder from the air stream, allowing the powder to be collected in a receiving container while the air is either recycled or discharged. This closed-loop system minimizes environmental impact and ensures compliance with industrial hygiene standards.
Key Features and Advantages of Micro Silica Powder Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of micro silica powder applications. The equipment offered by HeadPowder is distinguished by several key features that enhance performance and reliability:
1. **High Efficiency and Low Loss**: The sealed pipeline design and optimized air-powder ratio ensure that the majority of the micro silica powder is transported without significant loss. This is critical for maintaining product yield and reducing material waste.
2. **Dust-Free Operation**: Unlike traditional bulk handling methods, pneumatic conveying systems operate in a closed environment, preventing dust from escaping into the workplace. This not only improves air quality but also protects the health of operators and maintains a clean working environment.
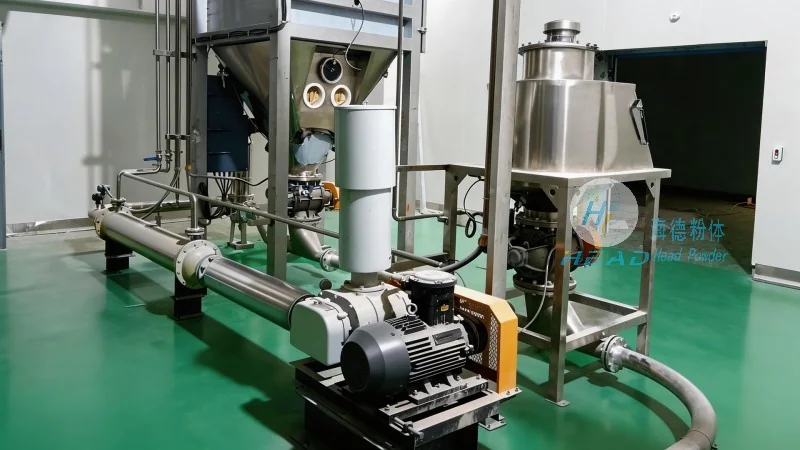
3. **Adaptability to Particle Size and Density**: The systems are engineered to handle a wide range of particle sizes and densities, making them suitable for various grades of micro silica powder. The adjustable air flow and pressure settings allow for customization to match the specific characteristics of the material being transported.
4. **Low Maintenance and Easy Cleaning**: The components are designed for easy access and maintenance, with features such as quick-release fittings and removable filter elements. This reduces downtime and operational costs, ensuring long-term reliability.
5. **Environmental Compliance**: By minimizing dust emissions and utilizing recycled air, the systems help companies meet environmental regulations and reduce their carbon footprint. This is particularly important in industries where sustainability is a key concern.
Technical Specifications and Application Scenarios
The pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is available in various configurations to suit different production scales and operational requirements. Typical technical specifications include:
- **Conveying Capacity**: Ranging from a few kilograms per hour to several tons per hour, depending on the system size.
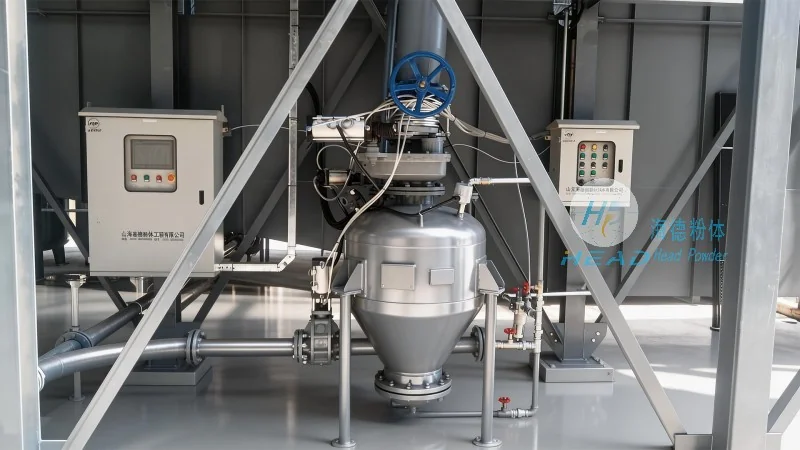
- **Air Flow Rate**: Adjustable to optimize the air-powder ratio, typically between 0.5 to 2 cubic meters per minute.
- **Pressure Range**: Vacuum systems operate at pressures up to -0.8 bar, while pressure systems can reach up to 6 bar.
- **Material Compatibility**: Stainless steel (304 or 316) and food-grade materials are used to prevent contamination, making the equipment suitable for pharmaceutical and food industries.
These systems are widely used in the production of micro silica powder for applications such as concrete additives, rubber reinforcement, and electronic components. The equipment is also suitable for handling other fine powders, making it a versatile solution for various industrial processes.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the brand under Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer of pneumatic conveying equipment and related systems. With its headquarters in Shandong, China, the company has established itself as a trusted partner for businesses seeking reliable and efficient solutions for powder handling. HeadPowder's team of engineers and technicians brings extensive experience in designing and implementing custom pneumatic conveying systems, ensuring that each project is tailored to meet the unique needs of the client.
The company's commitment to quality and innovation has enabled it to deliver products that meet international standards and customer expectations. By leveraging advanced technology and rigorous testing procedures, HeadPowder ensures that its equipment operates at peak performance, providing long-term value to its clients. With a focus on customer satisfaction and sustainable operations, Shandong HeadPowder Engineering Co., Ltd. continues to be a key player in the global market for powder handling solutions.




