Clay ash powder pneumatic conveying equipment is a specialized system designed for the efficient and safe transportation of fine powder materials, such as clay ash, in industrial applications. This equipment plays a crucial role in various industries, including cement production, mining, and chemical processing, where the handling of bulk powders is essential for operational efficiency and product quality. The technology behind these systems combines pneumatic principles with mechanical components to achieve reliable material transport without the need for traditional bulk handling methods like conveyor belts or trucks.
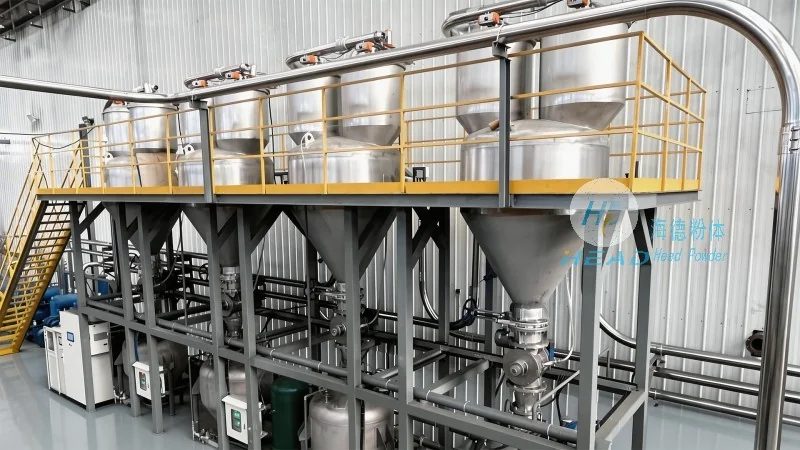
Working Principle of the Pneumatic Conveying System
The core of clay ash powder pneumatic conveying equipment lies in its pneumatic transport mechanism. The system operates by using compressed air to create a flow that moves the powder particles through a network of pipes. There are two primary modes of operation: suction and pressure. In suction mode, the system draws the powder from a source (like a hopper or storage silo) using a vacuum created by a fan or blower. The powder is then carried along the pipeline to the destination point, where it is discharged. In pressure mode, compressed air is introduced at the discharge end, pushing the powder forward through the pipeline. Both modes rely on the same fundamental principle: the air flow creates a pressure differential that propels the powder particles, allowing them to be transported over long distances with minimal loss and high efficiency.
The equipment typically consists of several key components, including a hopper or feed hopper to store and meter the powder, a fan or blower to generate the necessary air pressure, a pipeline system for transporting the powder-air mixture, a separation or collection unit to separate the powder from the air at the end of the line, and a control system to regulate the flow and pressure. The hopper is designed to maintain a consistent feed rate, preventing blockages or uneven flow. The fan or blower provides the required air volume and pressure, which is critical for maintaining the flow rate and preventing material degradation. The pipeline system is usually made of materials like stainless steel or plastic, chosen for their resistance to corrosion and wear from the powder particles. The separation unit, often a cyclone or bag filter, captures the powder from the air stream, allowing the clean air to be discharged back into the environment or recirculated. The control system ensures that the equipment operates within safe and efficient parameters, adjusting the air flow and feed rate as needed to match the process requirements.
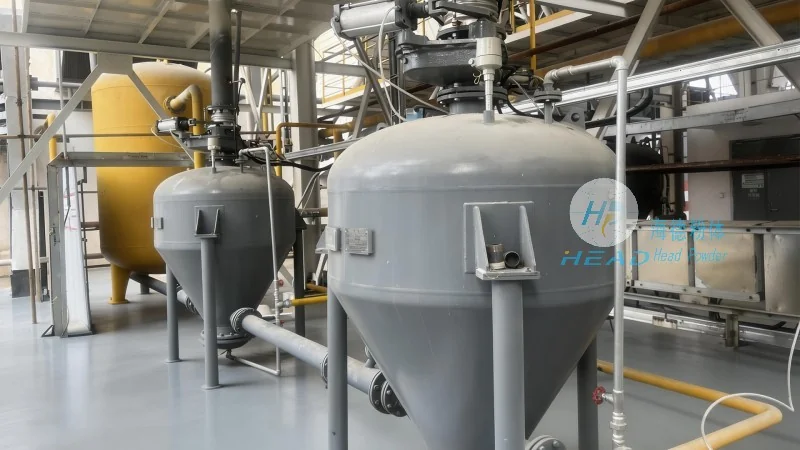
Key Features and Advantages of Clay Ash Powder Pneumatic Conveying Equipment
Clay ash powder pneumatic conveying equipment offers several distinct advantages that make it a preferred choice for industrial applications. One of the most significant benefits is its ability to handle fine, dusty powders without the need for mechanical contact, which reduces the risk of material degradation, contamination, or caking. Unlike traditional methods like screw conveyors or belt conveyors, pneumatic systems do not involve moving parts that come into direct contact with the powder, minimizing wear and tear and extending the equipment's lifespan. This also reduces the likelihood of cross-contamination between different materials, which is crucial in industries where product purity is paramount.
Another key advantage is the system's flexibility and adaptability. Pneumatic conveying can be configured for both short and long-distance transport, with the ability to change the direction of flow by adjusting the pipeline layout. This makes it suitable for complex layouts in industrial facilities, where materials need to be moved from one location to another with minimal disruption. The equipment can also handle a wide range of powder characteristics, including varying particle sizes, moisture content, and bulk density, making it versatile for different applications. Additionally, pneumatic systems are generally more energy-efficient than other bulk handling methods, as they use compressed air to move the material, which can be more cost-effective in the long run, especially when considering the reduction in maintenance and replacement of parts.
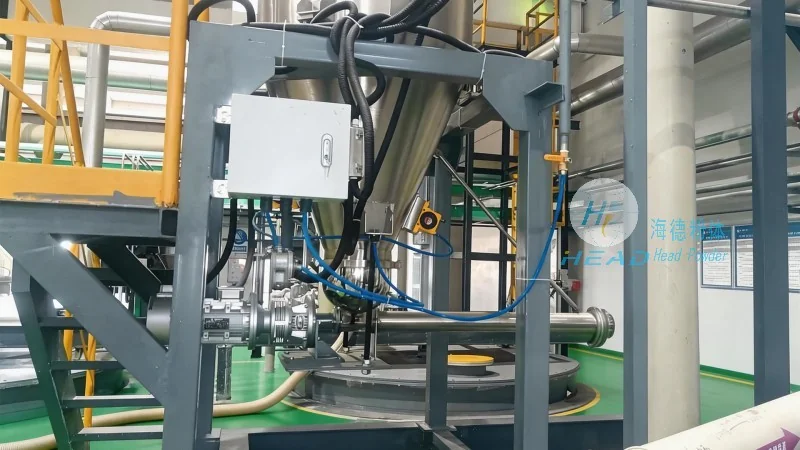
The environmental benefits of clay ash powder pneumatic conveying equipment are also notable. By containing the powder within a closed system, the equipment minimizes dust emissions and prevents airborne contamination, which is a major concern in industries dealing with fine powders. This not only improves workplace safety but also complies with environmental regulations, reducing the risk of fines or operational disruptions. The closed system design also helps in maintaining the quality of the powder, as it is protected from moisture, air, and other contaminants that could affect its properties. Furthermore, the ability to recycle the air in some systems reduces energy consumption and further enhances the environmental performance of the equipment.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling equipment, including clay ash powder pneumatic conveying systems. HeadPowder is headquartered in Shandong, China, and has established itself as a trusted partner for industries requiring reliable and efficient bulk material transport solutions. The company specializes in designing, manufacturing, and installing customized pneumatic conveying systems tailored to the specific needs of its clients, ensuring optimal performance and durability. With a strong commitment to quality and innovation, HeadPowder employs a team of experienced engineers and technicians who work closely with customers to understand their operational challenges and provide tailored solutions. The company's products are known for their high efficiency, low maintenance requirements, and compliance with international standards, making them suitable for a wide range of industrial applications. HeadPowder's facilities in Shandong are equipped with state-of-the-art technology and quality control measures to ensure that every piece of equipment meets the highest standards before delivery. The company also provides comprehensive after-sales support, including installation, training, and maintenance services, to ensure that clients can maximize the performance and lifespan of their equipment. By leveraging its expertise and experience, HeadPowder continues to be a key player in the powder handling industry, helping businesses improve their operational efficiency and reduce costs through advanced pneumatic conveying technology.




