Efficient and reliable material handling is a critical aspect of modern industrial operations, especially when dealing with bulk powders like baking soda. The pneumatic conveying system, specifically designed for baking soda powder, offers a solution that combines performance, safety, and operational flexibility. This article delves into the working principle and key features of such a system, highlighting how it addresses the unique challenges associated with transporting fine powders while maintaining high standards of efficiency and control.
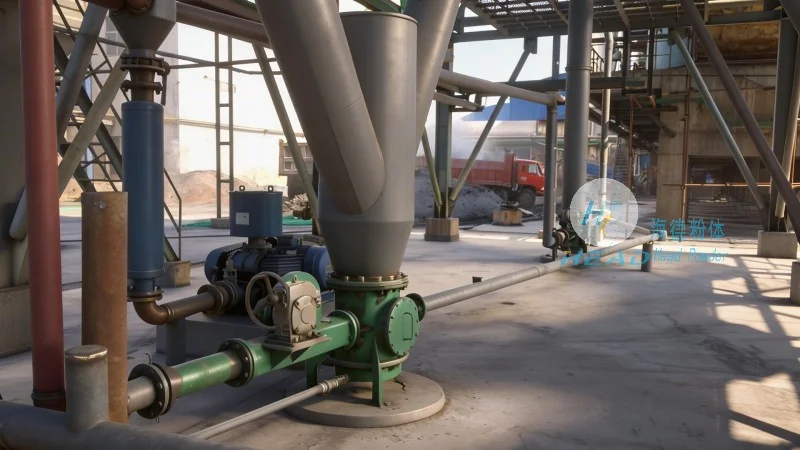
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions. With a strong focus on innovation and customer-centric design, the company specializes in developing customized pneumatic conveying systems tailored to the specific needs of various industries. HeadPowder's commitment to quality and reliability has established it as a trusted partner for businesses requiring efficient and safe powder transportation solutions.
Overview of Baking Soda Powder Pneumatic Conveying System
The baking soda powder pneumatic conveying system is a sophisticated piece of equipment designed to transport fine powders like sodium bicarbonate (baking soda) from one location to another within an industrial facility. This system operates by using compressed air or other gas to create a flow that moves the powder through a network of pipes and components. The design of the system is optimized to handle the specific properties of baking soda, including its fine particle size, low bulk density, and potential for dust generation, ensuring a smooth and efficient transfer process.
Working Principle of the System
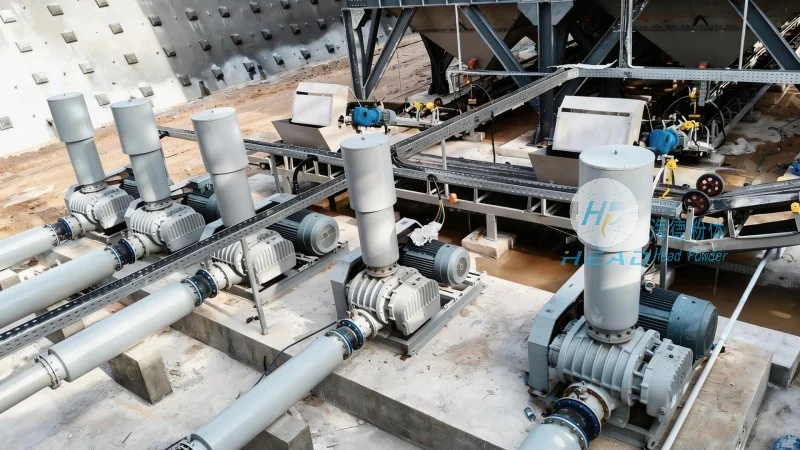
The core of the pneumatic conveying system lies in its ability to use air as the conveying medium. The process begins with the powder being introduced into a hopper or feeder, where it is then drawn into a pipeline by the pressure differential created by the air flow. The compressed air, typically supplied by a blower or compressor, generates a high-velocity stream that entrains the powder particles, forming a dense phase or dilute phase flow depending on the system design. The system can operate in either positive pressure or negative pressure modes, with positive pressure being more common for systems that transport powder over longer distances or to multiple destinations. The key components involved in the working principle include the air supply unit, the conveying line, the dust collection system, and the receiving hopper. Each component plays a crucial role in ensuring the efficient and safe transport of baking soda powder.
Key Features and Advantages
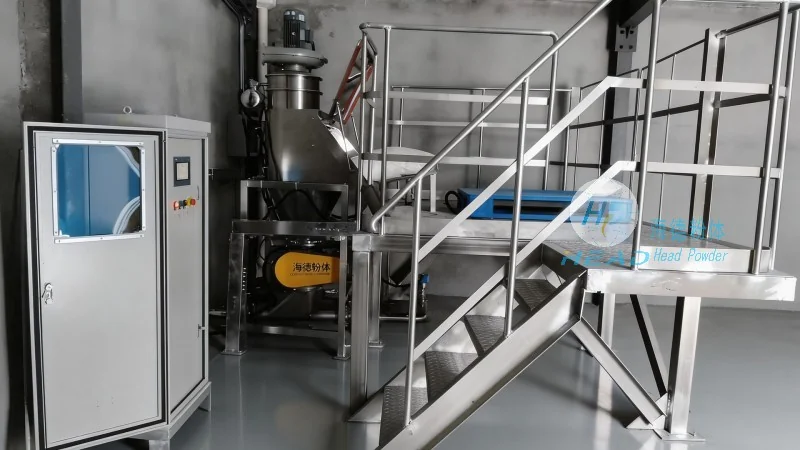
The baking soda powder pneumatic conveying system offers several distinct features and advantages that make it an ideal choice for industrial applications. Firstly, it provides a dust-free and enclosed transport environment, which is essential for maintaining product quality and ensuring workplace safety. Unlike traditional belt or bucket elevators, the pneumatic system eliminates the risk of dust exposure and cross-contamination, making it suitable for food-grade and pharmaceutical applications where hygiene is paramount. Secondly, the system offers high flexibility in terms of layout and integration. It can be easily adapted to existing facility layouts, allowing for the transportation of powder to multiple points or back to the original source. This flexibility is particularly beneficial in plants where space is limited or where the production process requires frequent changes in material flow. Thirdly, the system is highly efficient in terms of energy consumption and operational costs. By using compressed air as the primary energy source, the system minimizes the need for mechanical components like belts or chains, reducing maintenance requirements and extending the lifespan of the equipment. Additionally, the system can be equipped with advanced control systems that allow for real-time monitoring and adjustment of the conveying parameters, ensuring optimal performance and preventing system failures. Finally, the system is designed with safety in mind, incorporating features such as pressure relief valves, explosion-proof components, and emergency shut-off mechanisms to protect both the equipment and personnel from potential hazards.
Applications and Industries
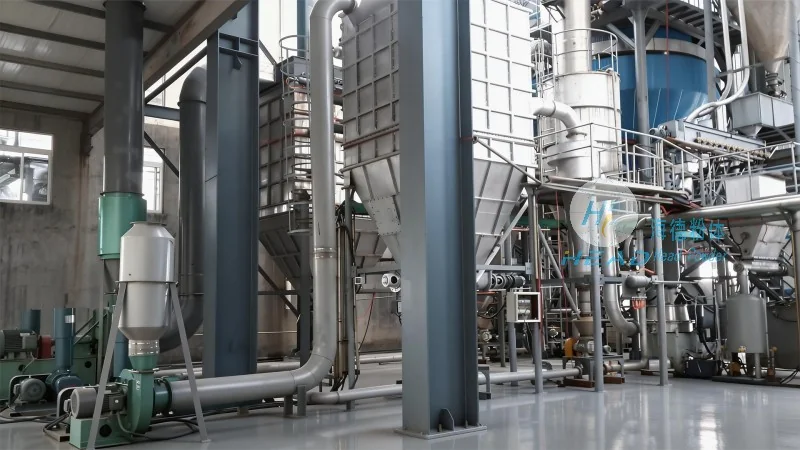
The baking soda powder pneumatic conveying system is widely used in various industries that require the handling of fine powders. Some of the key applications include the food and beverage industry, where baking soda is used as a leavening agent and a pH adjuster. The system ensures that the powder is transported safely and hygienically to production lines, bakeries, and storage areas. In the pharmaceutical industry, the system is used to transport baking soda for use in drug formulations and as a raw material in the production of various medications. The system's ability to maintain a sterile and dust-free environment is crucial in this sector. Additionally, the system is used in the chemical industry for the transportation of baking soda as a raw material in the production of other chemicals. The system's flexibility and efficiency make it suitable for a wide range of industrial applications, from small-scale production facilities to large-scale manufacturing plants.
Conclusion
In conclusion, the baking soda powder pneumatic conveying system is a highly effective and reliable solution for the transportation of fine powders in industrial settings. By leveraging the principles of pneumatic conveying, the system offers a dust-free, flexible, and energy-efficient method of handling baking soda powder. The working principle, which involves the use of compressed air to entrain and transport the powder, is designed to address the unique challenges associated with this material. The key features of the system, including its enclosed design, flexibility, and safety features, make it an ideal choice for various industries. With its commitment to quality and innovation, Shandong HeadPowder Engineering Co., Ltd. continues to provide advanced material handling solutions that meet the evolving needs of modern industry. The pneumatic conveying system not only improves operational efficiency but also enhances workplace safety and product quality, making it a valuable asset for any business dealing with baking soda powder.




