Desulfurizer powder conveying systems are critical components in industrial processes, particularly in power plants and chemical facilities where the efficient handling of powdered desulfurization agents is essential. This article explores the working principle and key features of such systems, highlighting how they contribute to operational efficiency and environmental compliance.
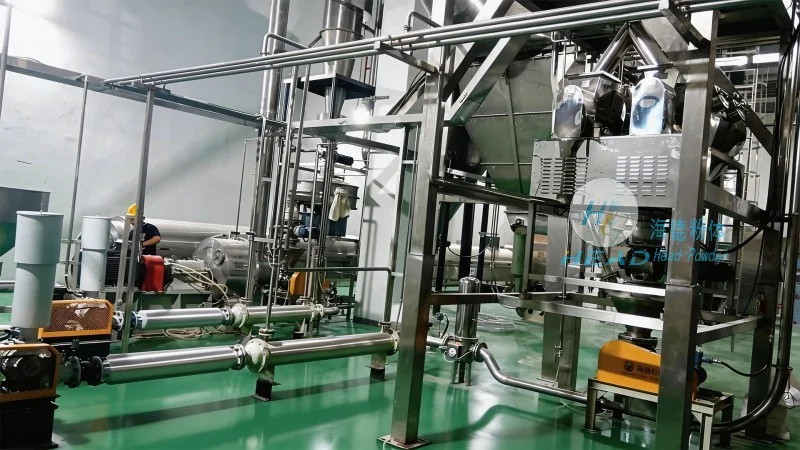
Understanding the Working Principle of Desulfurizer Powder Conveying Systems
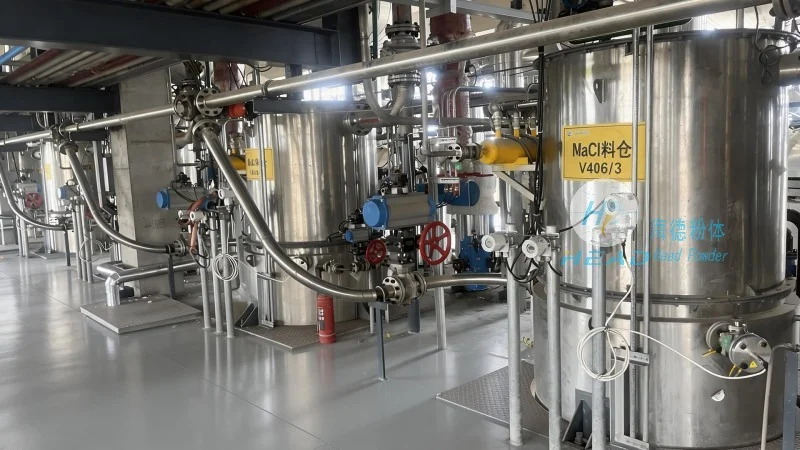
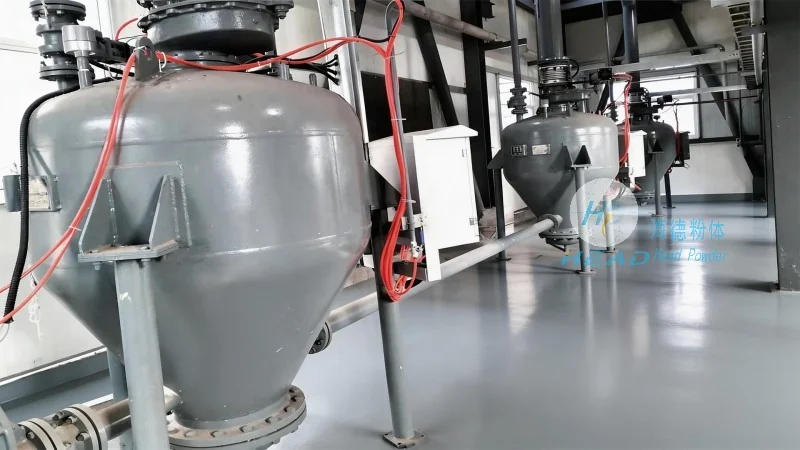
The desulfurizer powder conveying system typically operates through a combination of mechanical and pneumatic components designed to transport powdered desulfurization reagents from storage to the application point. The core mechanism involves the use of air or gas to create a flow of particles, often utilizing devices such as rotary valves, pneumatic conveying lines, and dust collectors. The system begins with the storage of desulfurizer powder in a silo or hopper, where it is then fed into a conveyor line. A blower or compressor generates the necessary air pressure to move the powder through the pipeline, ensuring a consistent and controlled flow. The conveying process may involve different stages, including primary and secondary conveying, to cover longer distances or handle varying particle sizes. At the destination, the powder is deposited into a reactor or absorber, where it reacts with flue gases to remove sulfur compounds. The system also incorporates dust collection and filtration components to ensure minimal air pollution and compliance with environmental regulations.
Key Features of Desulfurizer Powder Conveying Systems
Modern desulfurizer powder conveying systems are characterized by several advanced features that enhance performance and reliability. One of the primary features is the ability to handle a wide range of powder properties, including varying particle sizes, moisture content, and bulk density. This adaptability is achieved through adjustable air flow rates and specialized feeding mechanisms, such as screw feeders or vibratory feeders, which ensure consistent material flow. Another critical feature is the system's efficiency in energy consumption, as optimized air pressure and flow control reduce operational costs while maintaining performance. The design also emphasizes safety and maintenance, with components like explosion-proof motors, dust-proof seals, and easy-to-access maintenance points. Additionally, advanced monitoring systems, including pressure sensors and flow meters, provide real-time data on system performance, enabling proactive maintenance and troubleshooting. The integration of dust collection and filtration systems ensures that the process meets stringent environmental standards, minimizing particulate emissions and protecting worker health.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of these advanced desulfurizer powder conveying systems, is a leading engineering company based in Shandong, China. With years of experience in the chemical and power industries, HeadPowder specializes in designing and manufacturing customized conveying solutions tailored to specific industrial needs. The company's commitment to quality and innovation has made it a trusted partner for clients seeking reliable and efficient powder handling systems. HeadPowder's products are engineered to meet international standards and are supported by comprehensive after-sales services, including installation, training, and technical support. The company's facilities in Shandong are equipped with state-of-the-art technology and skilled personnel, ensuring that each system is built to the highest specifications and delivered on time.
Applications and Benefits of Desulfurizer Powder Conveying Systems
Desulfurizer powder conveying systems are widely used in power generation, petrochemical, and industrial manufacturing sectors where flue gas desulfurization is required. The primary benefit of these systems is the ability to transport desulfurizer powder efficiently and safely, reducing downtime and operational costs. By automating the powder handling process, the systems minimize human intervention, improving safety and reducing the risk of accidents. The consistent flow of powder also ensures stable operation of the desulfurization process, leading to higher removal efficiency of sulfur compounds from flue gases. Furthermore, the advanced features of these systems, such as energy efficiency and environmental compliance, help companies meet regulatory requirements and reduce their environmental footprint. The reliability of the system is crucial in continuous operation, as any interruption in powder supply can impact the performance of the desulfurization unit. HeadPowder's systems are designed to provide long-term reliability, with durable components and robust construction that can withstand harsh industrial conditions.
Conclusion
In conclusion, desulfurizer powder conveying systems are essential for the efficient operation of flue gas desulfurization processes. The working principle, which combines mechanical and pneumatic components, ensures the reliable transport of powdered desulfurization agents. Key features such as adaptability, energy efficiency, and safety make these systems ideal for various industrial applications. HeadPowder, with its expertise and commitment to quality, provides reliable and customized solutions that meet the specific needs of clients. By investing in advanced powder conveying systems, industrial facilities can enhance operational efficiency, reduce costs, and comply with environmental regulations, contributing to a more sustainable and environmentally friendly operation.




