Wet nitrate ammonium, a critical raw material in the fertilizer industry, requires efficient and reliable handling solutions to ensure safe and effective processing. The gas-pneumatic conveying system is a specialized technology designed to transport this material, especially when it contains moisture, with precision and minimal loss. This article provides a detailed introduction to the wet nitrate ammonium gas-pneumatic conveying system, focusing on its structural design and operational principles.
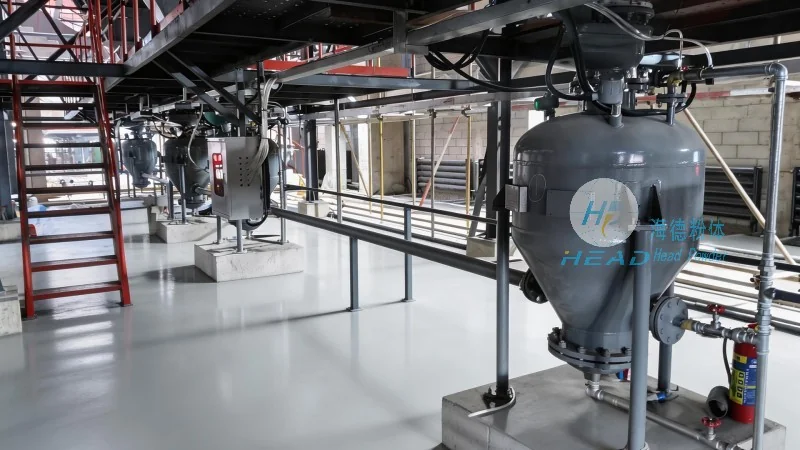
System Overview and Key Components
The wet nitrate ammonium gas-pneumatic conveying system is engineered to handle the unique challenges posed by this material, which often includes moisture content that can affect flow characteristics and equipment performance. The system typically consists of several core components that work in tandem to achieve efficient material transport. These components include a feed hopper, a rotary airlock valve, a conveying pipeline, a separator, and a dust collection system. Each component plays a crucial role in the overall operation, ensuring that the material is moved safely and efficiently from the source to the destination.
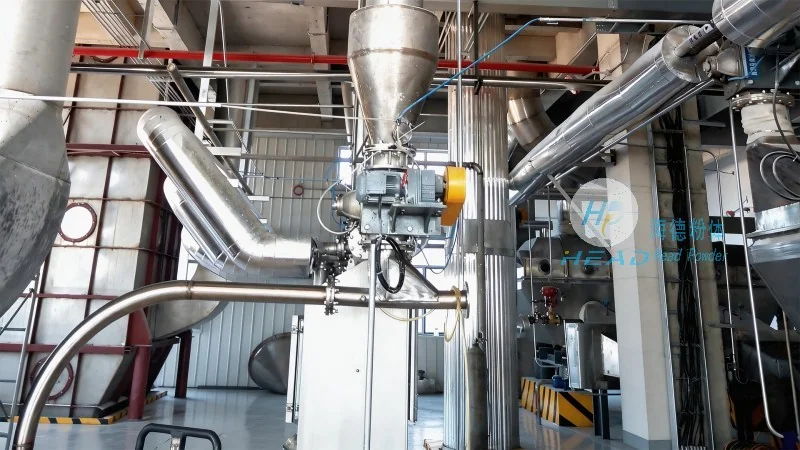
Structural Design and Working Principle
The structural design of the wet nitrate ammonium gas-pneumatic conveying system is optimized for the specific properties of the material. The feed hopper is designed to accommodate the bulk storage of wet nitrate ammonium, providing a stable feed source. The rotary airlock valve, positioned at the discharge end of the hopper, controls the flow of material into the conveying pipeline, preventing backflow and ensuring a consistent feed rate. The conveying pipeline, usually made of corrosion-resistant materials such as stainless steel or special alloys, is designed to withstand the chemical properties of the material and the effects of moisture. The separator, located at the receiving end, separates the conveyed material from the air stream, allowing the material to be collected while the air is discharged through a dust collection system. The dust collection system, often equipped with filters or cyclones, ensures that any airborne particles are captured, maintaining environmental compliance and operational safety.
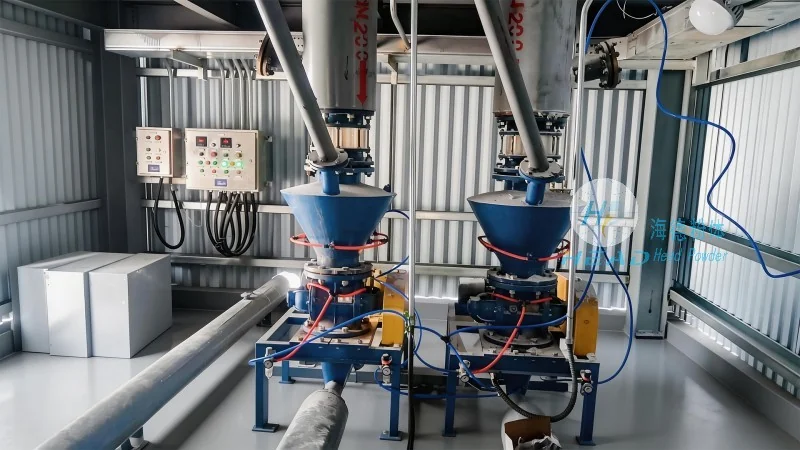
Advantages of the Gas-Pneumatic Conveying System
Compared to traditional mechanical conveying methods, the gas-pneumatic conveying system offers several advantages for handling wet nitrate ammonium. Firstly, it provides a closed system, which minimizes dust exposure and reduces the risk of material contamination or loss. This is particularly important for nitrate ammonium, which can be sensitive to moisture and air exposure. Secondly, the system allows for precise control over the flow rate and pressure, enabling operators to adjust the conveying parameters according to the material's characteristics and the system's requirements. Thirdly, the system is relatively low in maintenance, as it has fewer moving parts compared to mechanical conveyors, reducing downtime and operational costs. Additionally, the gas-pneumatic system can handle materials with varying moisture content and particle sizes, making it versatile for different applications in the fertilizer industry.
Application and Operational Considerations
The wet nitrate ammonium gas-pneumatic conveying system is widely used in the fertilizer production process, particularly in the stages where the material is transferred between storage, processing, and packaging units. The system's ability to handle wet materials with high efficiency makes it suitable for continuous production lines, where consistent material flow is essential. Operational considerations include maintaining proper moisture levels in the material to ensure optimal flow characteristics, regular inspection of the conveying pipeline and components for corrosion or wear, and ensuring that the dust collection system is functioning effectively to prevent air pollution. Proper training of operators on the system's controls and safety protocols is also crucial to ensure safe and efficient operation.
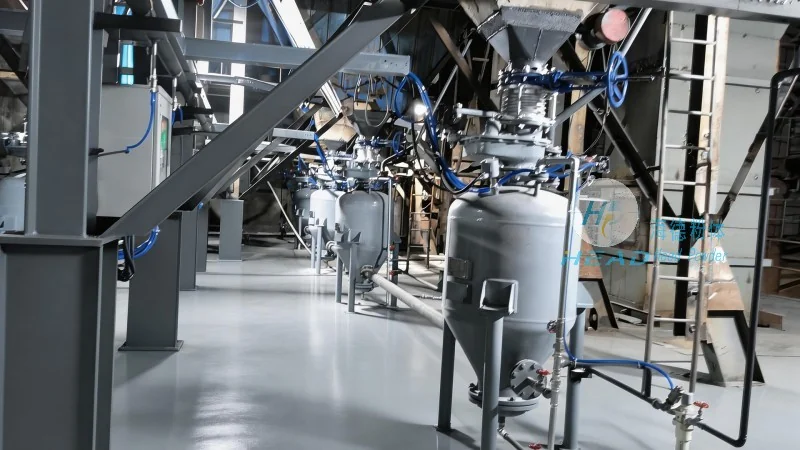
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of specialized conveying systems for the chemical and fertilizer industries. With a strong focus on innovation and quality, the company has developed advanced solutions for handling challenging materials like wet nitrate ammonium. The company's expertise lies in designing and manufacturing systems that meet the specific needs of clients, ensuring reliability, efficiency, and safety in material handling operations. Headpowder's commitment to customer satisfaction and technological advancement has established it as a trusted partner in the industry, providing comprehensive solutions for various conveying requirements.




