Desulfurization fly ash, a byproduct of flue gas desulfurization in power plants, presents unique challenges in handling and transportation due to its fine particle size and potential for dust generation. The development of specialized conveying equipment is crucial for efficient and safe management of this material. This article explores the working principle and key features of the desulfurization fly ash powder conveying equipment, highlighting its role in modern industrial applications.
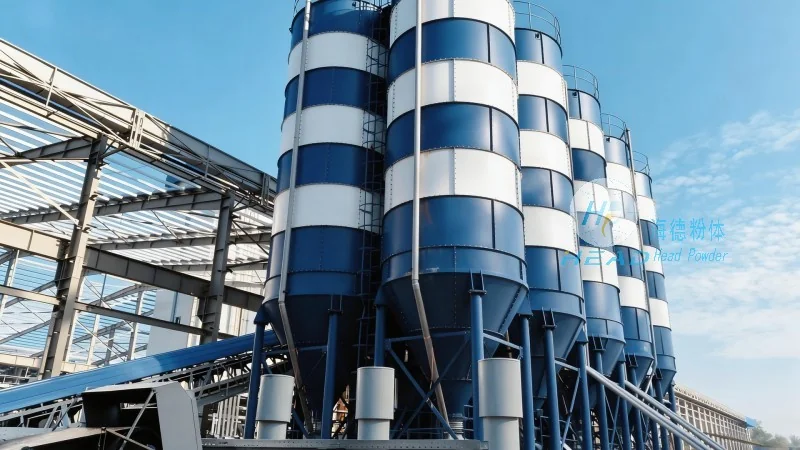
Introduction to Desulfurization Fly Ash Powder Conveying Equipment
Desulfurization fly ash, commonly referred to as FGD fly ash, is a fine powder generated during the removal of sulfur dioxide from flue gases. Its handling requires equipment designed to manage high volumes of fine particles while minimizing dust emissions and ensuring operational efficiency. The conveying equipment for this material must address challenges such as particle agglomeration, corrosion resistance, and the need for low maintenance. The equipment from Shandong HeadPowder Engineering Co., Ltd. is engineered to meet these demands, providing reliable solutions for industrial facilities.
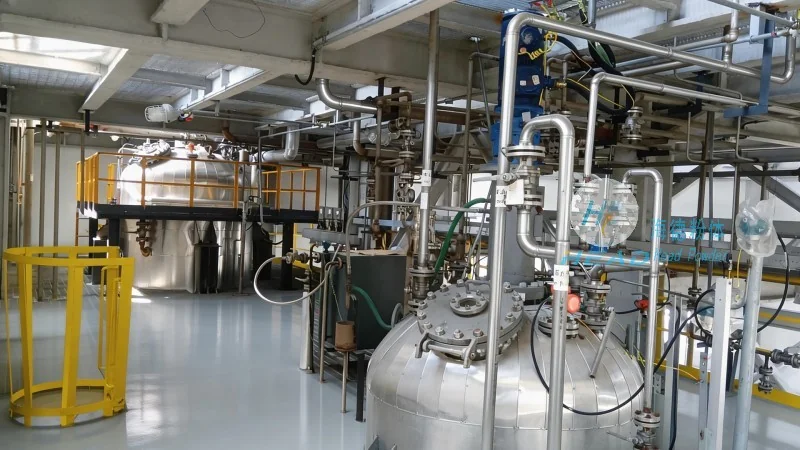
Working Principle of the Desulfurization Fly Ash Powder Conveying Equipment
The core working principle of the desulfurization fly ash powder conveying equipment involves the use of advanced powder handling technologies, typically combining mechanical and pneumatic systems. The process begins with the collection of fly ash from storage silos or hoppers. The equipment utilizes a combination of positive pressure or negative pressure air flow to transport the fine particles through pipelines. The system includes components such as feeders, ducts, and control valves that regulate the flow rate and pressure, ensuring consistent and controlled delivery. The design incorporates features like dust suppression and filtration to maintain air quality and prevent environmental contamination. The equipment operates by creating a stable flow of air and material, preventing blockages and ensuring smooth transportation from the source to the disposal or utilization point. Specifically, the positive pressure system uses a blower to generate air pressure, which forces the fly ash through the pipeline. The negative pressure system, on the other hand, uses a vacuum pump to create a suction effect, drawing the material into the duct. Both systems are equipped with rotary valves or star feeders at the inlet to control the material flow and prevent backflow. The pipelines are often made of corrosion-resistant materials like stainless steel or special alloys to withstand the acidic properties of the fly ash. The control system monitors pressure, flow rate, and temperature, adjusting parameters in real-time to maintain optimal performance. This dynamic control ensures that the conveying process is efficient and safe, minimizing energy consumption and operational risks.
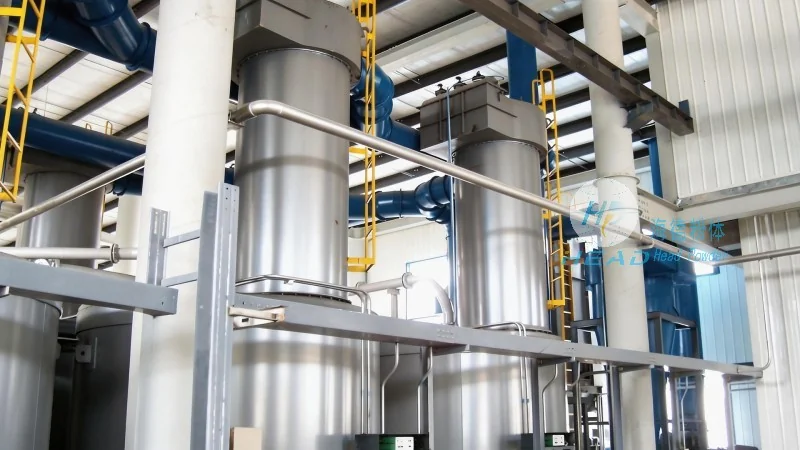
Key Features of the Equipment
The desulfurization fly ash powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is characterized by several key features that enhance its performance and reliability. One of the primary features is its high efficiency in handling large volumes of fine particles, with the ability to transport material over long distances without significant loss or degradation. The equipment is designed with corrosion-resistant materials to withstand the acidic and abrasive nature of fly ash, ensuring long service life and minimal maintenance. Another important feature is the integration of dust control mechanisms, which include sealed systems and filtration units to comply with environmental regulations and maintain workplace safety. The system also offers adjustable flow rates and pressure controls, allowing operators to optimize performance based on specific application requirements. Additionally, the equipment is equipped with monitoring and alarm systems to detect any operational issues, providing early warnings and preventing system failures. The equipment's design also includes features such as self-cleaning mechanisms to prevent material buildup and blockages, ensuring continuous operation. The use of high-quality seals and gaskets minimizes air leakage, reducing energy waste and maintaining consistent pressure levels. The equipment is also designed for easy maintenance, with accessible components that can be serviced without extensive downtime. This reduces maintenance costs and ensures the equipment remains operational for extended periods.
Technical Advantages and Applications
The desulfurization fly ash powder conveying equipment offers several technical advantages that make it suitable for various industrial applications. Its ability to handle high moisture content and fine particle sizes makes it ideal for power plants, cement factories, and construction material producers. The equipment's low energy consumption and reduced maintenance requirements contribute to cost savings and operational efficiency. The system's adaptability allows it to be integrated into existing infrastructure, minimizing installation time and disruption. The equipment is also designed for scalability, enabling it to be expanded as production needs grow. In addition to its industrial applications, the equipment plays a vital role in environmental management by ensuring the safe and efficient disposal of fly ash, reducing the risk of contamination and promoting sustainable practices. The equipment's performance is further enhanced by its compatibility with various downstream processes, such as fly ash utilization in cement production or land reclamation projects. This versatility makes it a valuable asset for facilities aiming to optimize resource recovery and minimize waste.
Company Profile and Service
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading manufacturer specializing in powder handling and conveying solutions. The company has extensive experience in developing and supplying equipment for various industrial sectors, including power generation, cement, and chemical industries. With a focus on innovation and customer satisfaction, HeadPowder provides customized solutions tailored to the specific needs of each client. The company's commitment to quality and reliability is reflected in its adherence to international standards and rigorous testing protocols. HeadPowder's team of engineers and technicians work closely with clients to understand their requirements and deliver equipment that meets or exceeds expectations. The company also offers comprehensive after-sales support, including maintenance services and technical assistance, ensuring long-term performance and customer satisfaction. HeadPowder's research and development efforts continuously improve the technology and efficiency of its products, staying ahead of industry trends and client needs. The company's reputation for excellence is built on its ability to deliver durable, high-performance equipment that enhances operational efficiency and supports environmental compliance. By partnering with HeadPowder, industrial facilities gain access to reliable and innovative solutions for their powder handling challenges, contributing to overall operational success and sustainability.




