For industrial applications involving the handling of paper chips and other powdery materials, efficient and reliable conveying systems are crucial. The paper chip powder conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., offers a robust solution tailored to meet the demands of modern material processing. This article explores the working principle and key features of this system, providing insights into its design and operational capabilities.
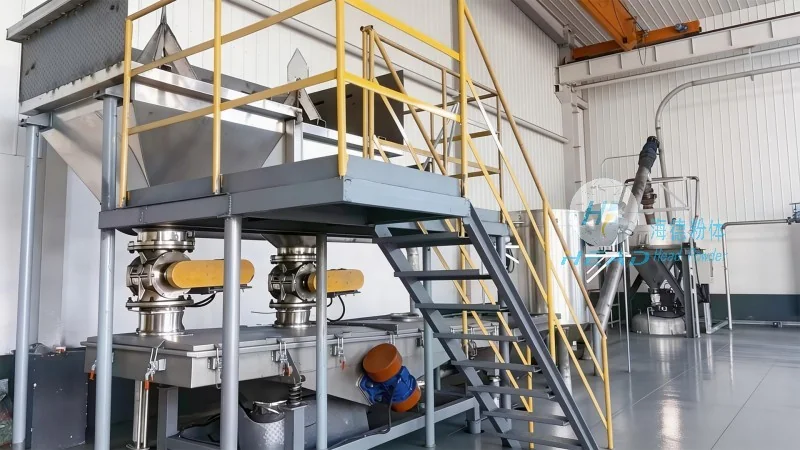
Understanding the Working Principle of the Paper Chip Powder Conveying System
The paper chip powder conveying system operates on a principle of continuous material transport, leveraging advanced engineering to ensure smooth and consistent movement of powders. At its core, the system consists of several interconnected components that work in tandem to achieve efficient conveying. The process typically begins with the feeding of paper chips into the system, where they are then drawn into a conveying pipeline. Within the pipeline, the material is propelled forward through a combination of air pressure, mechanical forces, or a combination of both, depending on the specific design. The system may incorporate features such as air locks, cyclones, or rotary valves to control the flow and prevent backflow, ensuring that the material moves in a single direction without loss or contamination. The control mechanisms, often integrated with sensors and automation, allow for precise regulation of the conveying rate, adapting to varying material volumes and processing requirements. This intelligent control system enhances operational efficiency and reduces downtime, making it suitable for high-volume production environments.
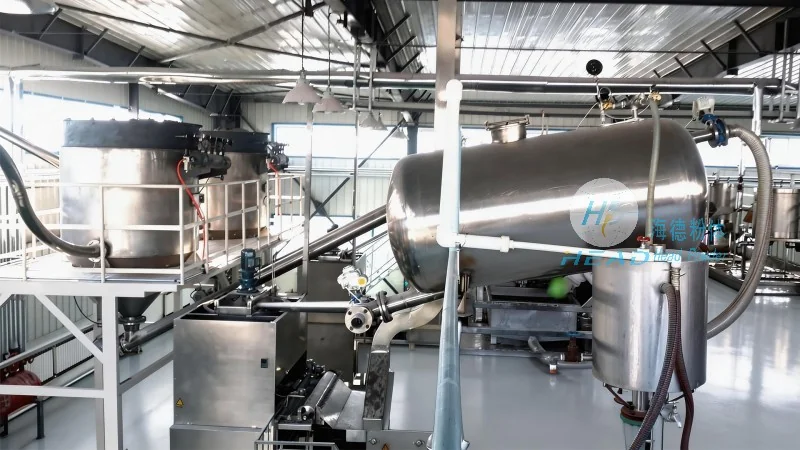
Key Features of the Paper Chip Powder Conveying System
Shandong HeadPowder Engineering Co., Ltd. has engineered the paper chip powder conveying system with several distinct features that set it apart in the industry. One of the primary advantages is its high conveying efficiency, which allows for the rapid transport of large quantities of paper chips over considerable distances. The system is designed to handle a wide range of particle sizes and moisture contents, making it versatile for various applications, from recycling to manufacturing processes. Another notable feature is its low maintenance requirements, thanks to the use of durable materials and robust construction. The components are built to withstand the rigors of continuous operation, reducing the need for frequent repairs and extending the system's lifespan. Additionally, the system incorporates safety features, such as pressure relief valves and emergency shut-off mechanisms, to protect both personnel and equipment during operation. The integration of advanced monitoring technology enables real-time tracking of system performance, allowing for proactive maintenance and troubleshooting. This proactive approach minimizes operational disruptions and ensures consistent performance over time.
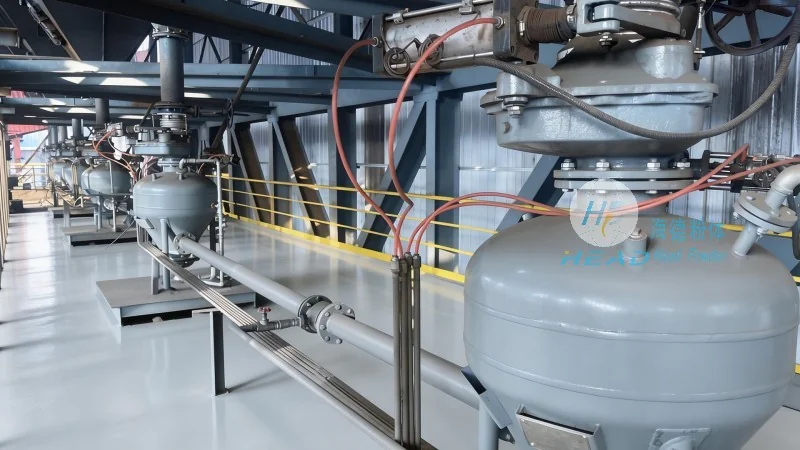
Application and Operational Benefits
The paper chip powder conveying system is widely used in industries where the handling of paper chips and powders is essential, such as the paper and pulp industry, recycling facilities, and manufacturing plants. Its ability to handle abrasive materials without significant wear and tear makes it ideal for applications involving high-volume material transport. The system's adaptability to different production scales allows it to be customized to meet the specific needs of each client, whether for small-scale operations or large industrial facilities. The operational benefits extend beyond efficiency; the system also contributes to improved safety and environmental compliance. By reducing dust emissions and minimizing material loss, it helps maintain a cleaner working environment and adheres to regulatory standards. The system's reliability ensures consistent output, which is critical for maintaining production schedules and meeting quality standards. Overall, the paper chip powder conveying system from Shandong HeadPowder Engineering Co., Ltd. represents a reliable and efficient solution for the transportation of paper chips and powders, supporting the smooth operation of industrial processes.




