Working Principle and Features of Chocolate Powder Conveying
Release time:2026-09-17 09:01:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Chocolate powder conveying is a critical process in the chocolate manufacturing industry, ensuring efficient and reliable transport of chocolate powders from storage to processing equipment. Understanding the working principle and key characteristics of these systems is essential for optimizing production efficiency and maintaining product quality. This article explores the fundamental mechanisms behind chocolate powder conveying and highlights the distinctive features that make such systems effective in industrial settings.
Working Principle of Chocolate Powder Conveying Systems
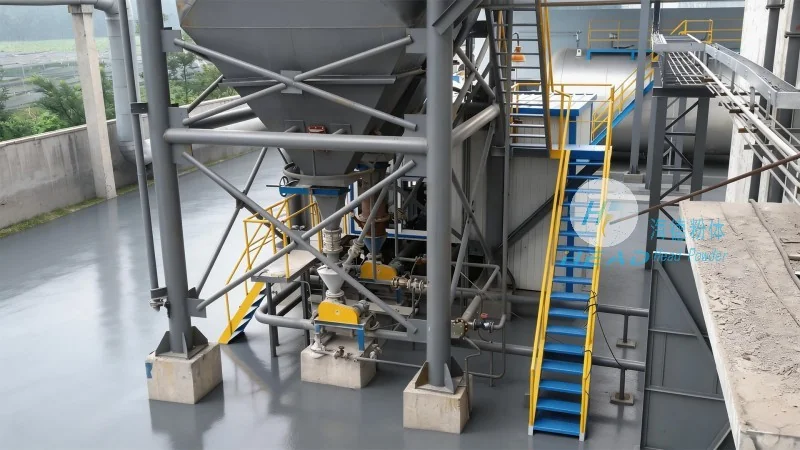
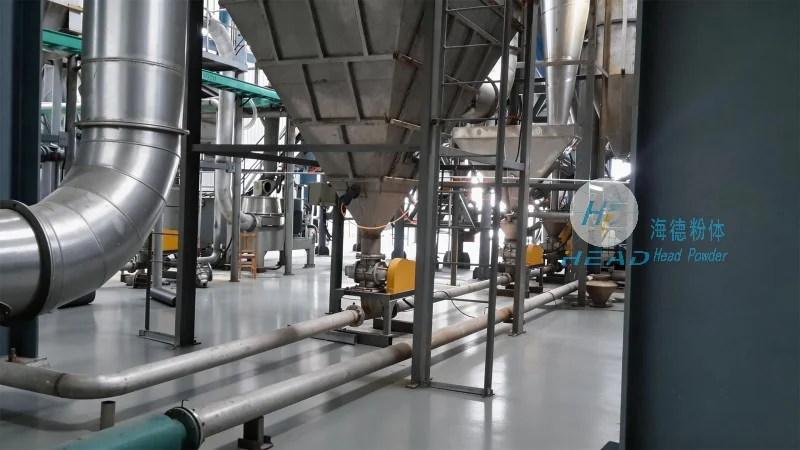
Chocolate powder conveying systems typically operate based on pneumatic or mechanical principles, designed to handle the unique properties of chocolate powders. The core working principle involves the use of air or mechanical force to move the powder through a pipeline or conveyor system. In pneumatic conveying, a vacuum or pressure differential is created to draw or push the powder particles through the system. This method is particularly effective for handling fine powders like chocolate, as it minimizes product degradation and contamination. The process begins with the chocolate powder being fed into a hopper or storage bin. From there, the powder is transported through a series of pipes, often using a combination of positive and negative pressure to maintain flow. The system may include components such as rotary valves, airlocks, and filters to ensure consistent and controlled movement of the powder. The working principle also emphasizes the importance of maintaining proper air-to-powder ratios to prevent blockages and ensure smooth operation. By controlling the pressure and flow rates, operators can optimize the conveying process to meet production demands while preserving the quality of the chocolate powder.
Key Characteristics of Chocolate Powder Conveying Systems
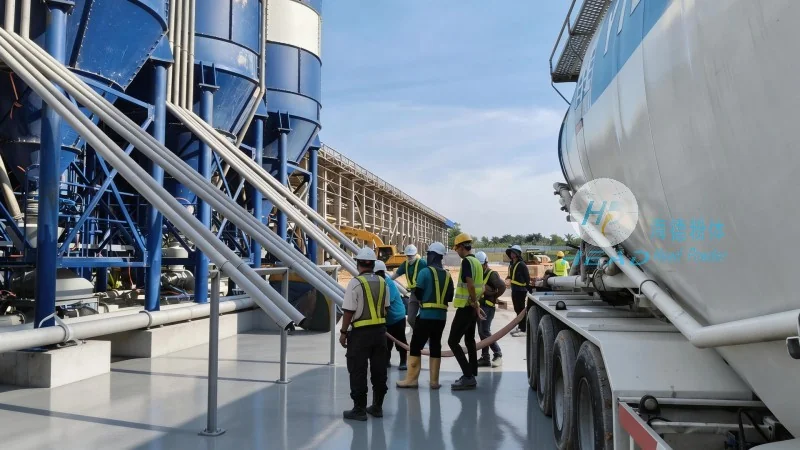
Effective chocolate powder conveying systems exhibit several key characteristics that distinguish them from other powder handling solutions. Firstly, they are designed to handle the hygroscopic nature of chocolate powders, which can absorb moisture from the air and affect product quality. The systems incorporate features such as moisture-proof seals and enclosed pipelines to prevent moisture ingress and maintain the powder's integrity. Secondly, these systems are built to handle the fine particle size of chocolate powders, which can lead to caking or agglomeration if not managed properly. The design includes components like agitators and vibration systems to break up clumps and ensure uniform flow. Thirdly, the systems prioritize hygiene and cleanliness, as chocolate products are often subject to strict food safety regulations. Stainless steel construction, easy-to-clean surfaces, and sanitary fittings are standard features to prevent contamination and ensure compliance with industry standards. Additionally, the conveying systems are engineered for durability and low maintenance, with robust materials and components that can withstand the abrasive nature of chocolate powders over extended periods. The ability to handle varying powder flow rates and volumes is another critical characteristic, allowing the system to adapt to different production stages, from batch processing to continuous production. By combining these features, chocolate powder conveying systems provide reliable, efficient, and safe transport of chocolate powders, supporting the overall productivity and quality of chocolate manufacturing operations.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
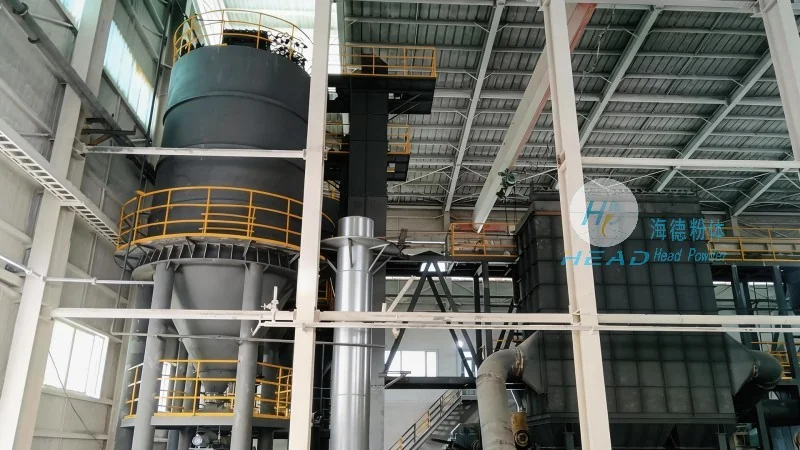
HeadPowder, a leading manufacturer in the powder handling industry, specializes in providing advanced conveying solutions for various industries, including chocolate manufacturing. With a strong commitment to innovation and quality, HeadPowder has developed state-of-the-art chocolate powder conveying systems that meet the highest standards of performance and reliability. The company's products are designed to address the unique challenges of handling chocolate powders, such as their fine particle size, hygroscopic properties, and strict hygiene requirements. HeadPowder's team of experts works closely with clients to understand their specific production needs and tailor conveying solutions that optimize efficiency and product quality. The company's facilities are equipped with advanced manufacturing and testing capabilities, ensuring that each system is built to withstand the demands of industrial use. HeadPowder's dedication to customer satisfaction and continuous improvement has earned it a reputation as a trusted partner in the powder handling sector. By leveraging its expertise and experience, HeadPowder continues to deliver cutting-edge solutions that enhance the productivity and success of its clients in the chocolate industry and beyond.




