

What is a Tonne Bag Unloading Powder Pneumatic Conveying System? And What Are Its Design Principles?
For industrial operations that handle bulk powders, efficient and reliable material handling is crucial. A tonne bag unloading powder pneumatic conveying system is a specialized solution designed to streamline the process of transferring large quantities of dry powders from bulk bags (also known as FIBCs or flexible intermediate bulk containers) into processing equipment or storage tanks. This system combines the principles of pneumatic conveying with automated tonne bag unloading, offering a seamless and cost-effective method for material transfer.
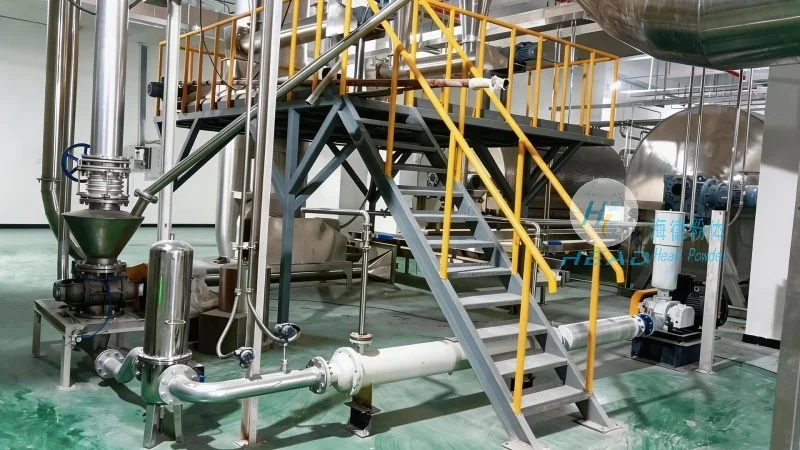
HeadPowder, a leading provider of engineering solutions for powder handling, specializes in designing and manufacturing advanced pneumatic conveying systems. With a focus on innovation and customer-centric design, HeadPowder's systems are engineered to meet the diverse needs of industries such as food, pharmaceuticals, chemicals, and minerals. The company's headquarters is located in Shandong, China, where a team of experienced engineers and technicians develops cutting-edge solutions tailored to specific operational requirements.
Design Principles of the Tonne Bag Unloading Powder Pneumatic Conveying System
The core design of a tonne bag unloading powder pneumatic conveying system revolves around the integration of several key components working in harmony. The system typically includes a tonne bag unloader, a hopper for collecting the discharged material, a pneumatic conveying line, and a receiver or storage vessel. The unloader is equipped with a valve mechanism that allows for controlled opening and closing of the bag, ensuring that the material is released in a controlled manner to prevent spillage and maintain product integrity.
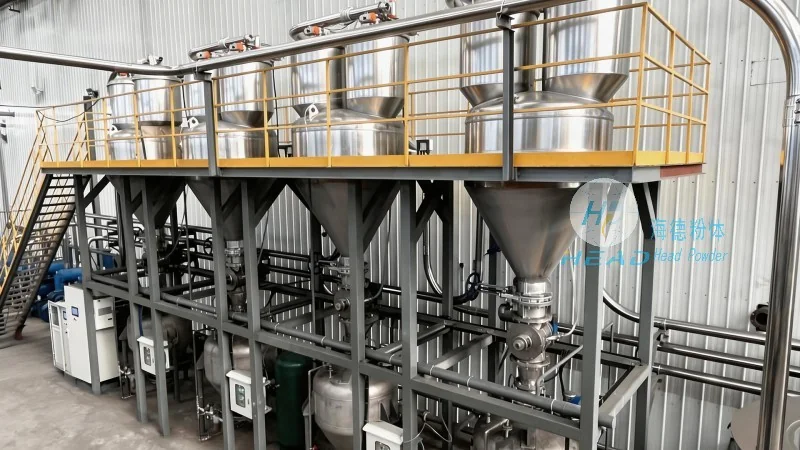
Once the tonne bag is opened, the material is drawn into the hopper by a vacuum or pressure source, depending on the system configuration. The hopper then feeds the material into the pneumatic conveying line, which uses compressed air or a vacuum to transport the powder through the system. The conveying line may include components such as elbows, bends, and filters to ensure smooth and efficient material movement while maintaining air quality and preventing dust contamination.
Key design considerations include the selection of appropriate air flow rates, the use of suitable materials for the conveying line and components to resist corrosion or abrasion, and the implementation of dust collection systems to comply with environmental regulations. The system is also designed to handle a wide range of powder characteristics, including varying particle sizes, densities, and flowability, ensuring consistent performance across different applications.
Advantages of the Tonne Bag Unloading Powder Pneumatic Conveying System
Implementing a tonne bag unloading powder pneumatic conveying system offers numerous benefits for industrial operations. One of the primary advantages is the significant reduction in labor costs, as the system automates the entire unloading process, eliminating the need for manual handling of heavy bulk bags. This not only improves safety by reducing the risk of back injuries and other accidents but also increases operational efficiency by allowing workers to focus on other critical tasks.
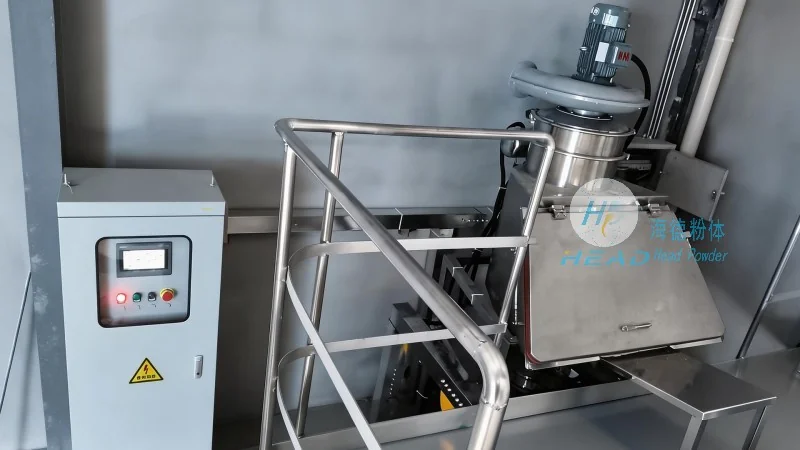
Another key benefit is the improvement in product quality and consistency. By controlling the unloading and conveying process, the system minimizes material degradation, moisture absorption, and contamination, which are common issues with manual handling. This ensures that the material reaches the processing stage in optimal condition, leading to higher product quality and reduced waste.
The system also enhances operational flexibility and scalability. HeadPowder's solutions can be customized to handle varying tonne bag sizes and material types, making them suitable for both small-scale and large-scale production environments. Additionally, the modular design allows for easy integration with existing processing lines, minimizing downtime during installation and ensuring a smooth transition to automated material handling.
Applications and Industries
The tonne bag unloading powder pneumatic conveying system is widely used across various industries that rely on bulk powder handling. In the food and beverage industry, it is used for processing ingredients such as flour, sugar, and spices, ensuring that the material is handled hygienically and efficiently. In the pharmaceutical industry, the system is critical for handling active pharmaceutical ingredients (APIs) and excipients, where strict contamination control and product purity are paramount.
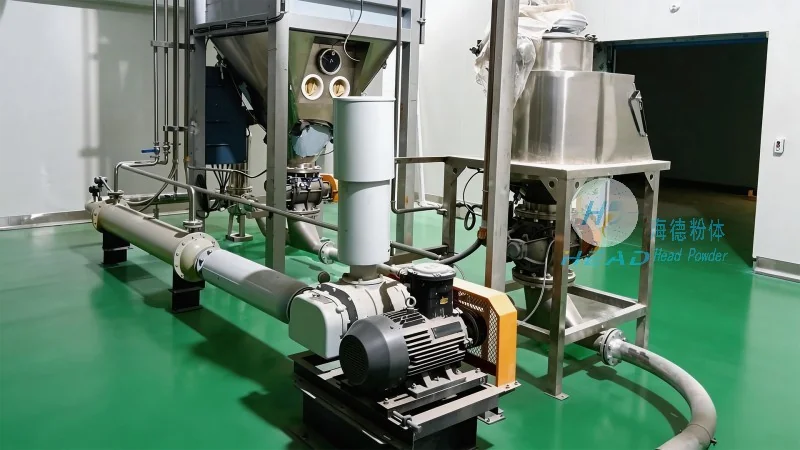
In the chemical industry, the system is used for transferring powders such as fertilizers, pigments, and specialty chemicals, where the need for precise control and minimal material loss is essential. Similarly, in the minerals and mining sector, the system is employed to handle raw materials like ores and minerals, improving the efficiency of the material transfer process from bulk bags to processing equipment.
Conclusion
For businesses seeking to optimize their powder handling operations, a tonne bag unloading powder pneumatic conveying system from HeadPowder offers a reliable and efficient solution. By combining advanced engineering with customer-focused design, the system addresses the challenges of manual tonne bag handling while ensuring product integrity and operational efficiency. With headquarters in Shandong, China, HeadPowder continues to lead the industry in providing innovative solutions that meet the evolving needs of modern industrial processes.