The automatic bulk bag unloading and powder conveying system is a specialized industrial solution designed to streamline the handling, transfer, and processing of bulk powders from flexible containers. As a key component in material handling operations, this system integrates advanced technologies to enhance efficiency, reduce labor costs, and improve safety in powder handling processes. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, this system represents a sophisticated approach to modern powder processing, catering to industries such as pharmaceuticals, food, chemicals, and more.
Key Components and Functionality of the System
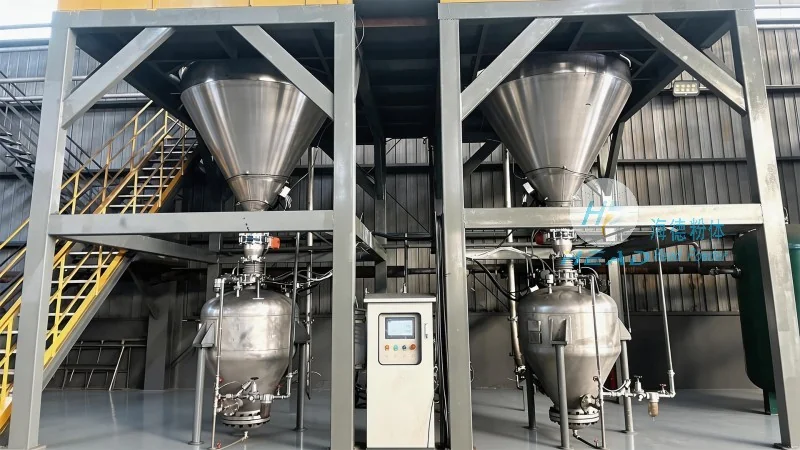
The system typically consists of several core components that work in tandem to achieve seamless operation. The primary function is the automatic unloading of bulk bags (also known as FIBCs or super sacks), which involves the controlled release of powder from the bag into a receiving hopper or container. This is often achieved through mechanisms like bottom discharge valves, which can be electrically or pneumatically operated. Once the bag is emptied, the system may include features for bag cleaning or repositioning to prepare for the next load. The conveying portion of the system uses various technologies, such as screw conveyors, pneumatic conveying systems, or bucket elevators, to transport the powder from the receiving hopper to the processing equipment. Additionally, the system may incorporate dust collection and filtration systems to ensure a clean and safe working environment, as well as level sensors and control panels to monitor and regulate the flow of material.
Design Principles Underpinning the System
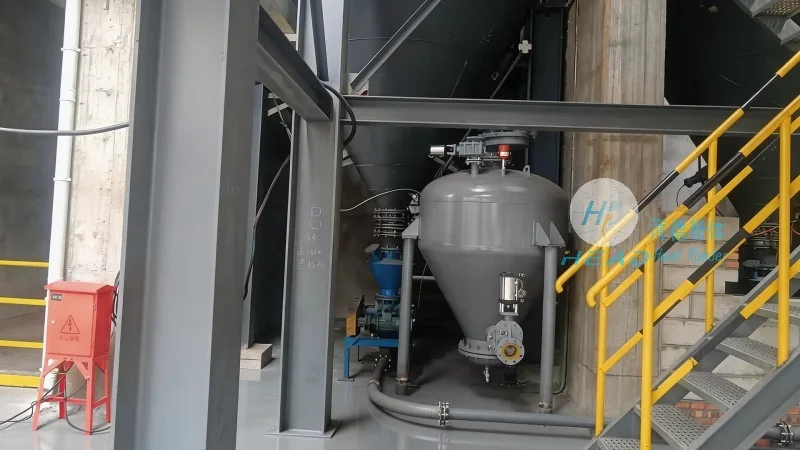
The design of the automatic bulk bag unloading and powder conveying system is guided by several critical principles aimed at optimizing performance, reliability, and user safety. First, the system prioritizes efficiency by minimizing downtime and maximizing throughput. This is achieved through automated processes that reduce the need for manual intervention, allowing for continuous operation. Second, the design emphasizes safety, incorporating features such as enclosed systems to contain dust, emergency stop buttons, and interlocks to prevent accidental exposure to moving parts. Third, the system is built for durability and ease of maintenance, with components that are resistant to corrosion and wear, and modular designs that allow for easy replacement or upgrades. Fourth, the design considers material compatibility, ensuring that the system can handle a wide range of powder types, from fine powders to bulkier granules, without causing clogging or degradation. Finally, the system adheres to industrial standards and regulations, such as those related to occupational health and safety, to ensure compliance and reliability in various applications.
Benefits and Applications of the System
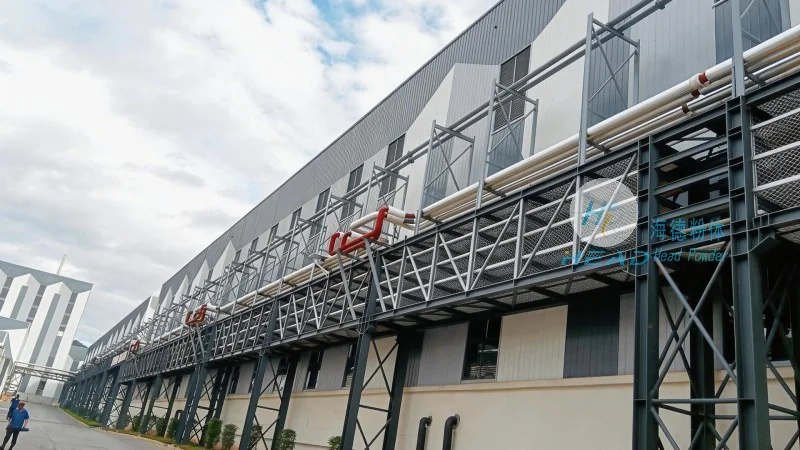
The automatic bulk bag unloading and powder conveying system offers numerous benefits to industries that rely on bulk powder handling. For manufacturers, it reduces labor costs by automating the unloading process, which can be time-consuming and hazardous when done manually. It also improves product quality by minimizing contamination and ensuring consistent material flow. In addition, the system enhances safety by reducing exposure to dust and preventing accidents related to manual handling. The system is particularly well-suited for applications where large quantities of powder need to be processed, such as in pharmaceutical production, where precision and cleanliness are paramount, or in food processing, where hygiene and safety are critical. Furthermore, the system can be customized to meet specific operational requirements, such as varying conveyor speeds, bag sizes, or material types, making it a versatile solution for diverse industrial needs.




