High-pressure dilute-phase pneumatic conveying systems are advanced industrial equipment designed to transport bulk materials through a pipeline using compressed air. This technology is widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining, due to its efficiency and ability to handle a wide range of materials. The system operates by creating a low-density mixture of material particles and air, which is then propelled through the pipeline under high pressure. This method offers several advantages over traditional mechanical conveying methods, such as reduced material degradation, lower maintenance costs, and the ability to transport materials over long distances without the need for intermediate storage.
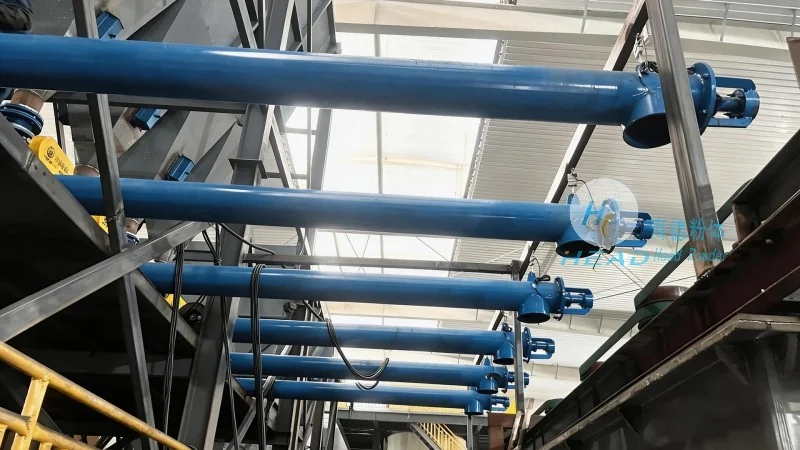
Key Components of a High-Pressure Dilute-Phase Pneumatic Conveying System
The high-pressure dilute-phase pneumatic conveying system consists of several critical components that work together to ensure efficient material transport. These components include the material feeder, which introduces the bulk material into the system; the air compressor, which generates the high-pressure air required for conveying; the conveying line, which is typically made of stainless steel or other corrosion-resistant materials to handle various materials and maintain system integrity; and the control system, which regulates the flow of material and air to optimize performance. Additionally, the system may include a filter or separator to remove any fine particles from the air before it is released back into the environment, ensuring compliance with environmental regulations.
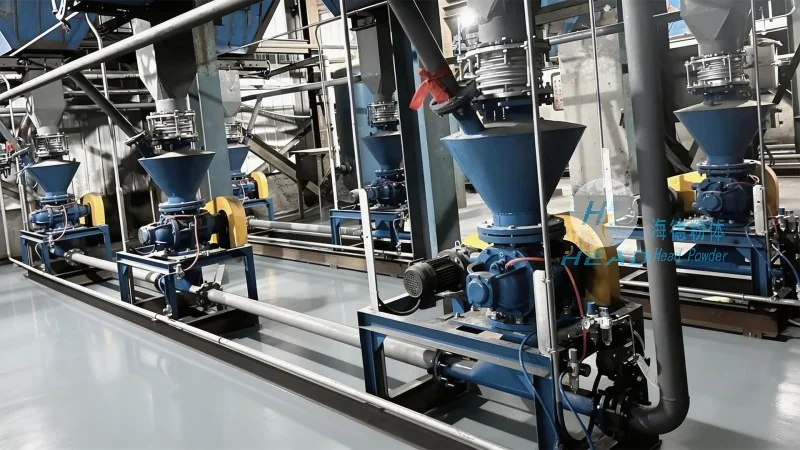
Design Principles of High-Pressure Dilute-Phase Pneumatic Conveying Systems
The design of a high-pressure dilute-phase pneumatic conveying system is based on several fundamental principles to ensure optimal performance and reliability. The first principle is the selection of the appropriate air velocity, which must be sufficient to keep the material particles suspended in the air stream while minimizing energy consumption. The air velocity is typically determined by the particle size, density, and flow rate of the material being conveyed. The second principle is the calculation of the required air pressure, which is influenced by the length of the conveying line, the number of bends or fittings, and the elevation changes in the system. Proper pressure calculations are crucial to prevent material deposition or blockages in the pipeline. The third principle is the consideration of material properties, such as moisture content, abrasiveness, and dust generation, which can affect the system's performance and require specific design adjustments, such as the use of special materials or additional filtration.
Applications and Benefits of High-Pressure Dilute-Phase Pneumatic Conveying Systems
High-pressure dilute-phase pneumatic conveying systems are versatile and can be applied to a wide range of applications. In the food industry, for example, they are used to transport powders like flour, sugar, and spices, ensuring hygienic and efficient handling. In the pharmaceutical industry, these systems are employed to convey active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining product purity and preventing contamination. In the chemical industry, they are used to transport various chemicals, including powders and granules, while minimizing the risk of chemical reactions or explosions. The benefits of these systems include improved process efficiency, reduced labor costs, and enhanced safety compared to traditional conveying methods. Additionally, the systems are designed to be flexible, allowing for easy integration into existing production lines and adaptation to changing production needs.
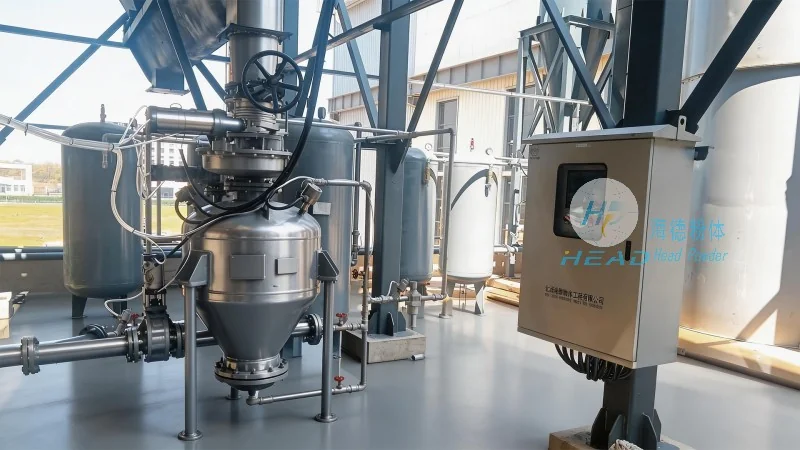
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-pressure dilute-phase pneumatic conveying systems and related equipment. The company is headquartered in Shandong, China, and has established a strong reputation for its innovative designs, high-quality products, and excellent customer service. HeadPowder specializes in customizing systems to meet the specific needs of its clients, ensuring that each system is optimized for the material being conveyed and the operational requirements of the facility. The company's team of engineers and technicians has extensive experience in the field and is committed to providing solutions that enhance productivity and reduce operational costs for its customers. With a focus on research and development, HeadPowder continuously improves its products to meet the evolving demands of the industry and maintain its position as a leader in the market.




