Pneumatic conveying technology has emerged as a pivotal solution for the efficient and reliable transport of bulk materials, particularly in the construction and mining sectors. When dealing with materials like stone debris or aggregate, traditional methods such as belt conveyors or trucks often face challenges related to material handling, dust control, and operational flexibility. Pneumatic conveying systems, which utilize air pressure to move particles through pipelines, offer a modern alternative that addresses these issues while enhancing overall productivity. This article explores the practical application of pneumatic conveying in the bulk transport of stone aggregate, highlighting its benefits, operational principles, and real-world implementation by Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder).
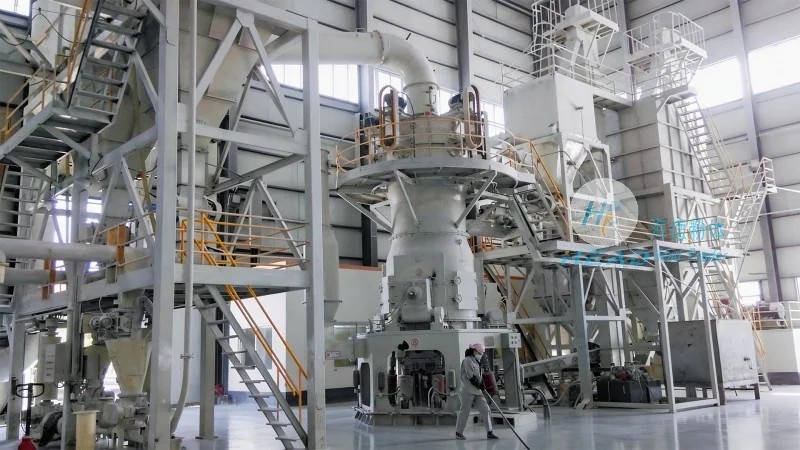
Understanding Pneumatic Conveying Systems for Stone Aggregate Transport
Pneumatic conveying systems operate on the principle of transporting solid particles through a pipeline using compressed air. There are two primary types: dilute-phase and dense-phase systems. Dilute-phase systems use high-velocity air to suspend particles, allowing for long-distance transport with minimal pressure drop. Dense-phase systems, on the other hand, use lower air velocities and higher particle concentrations, which are ideal for transporting sensitive or abrasive materials like stone aggregate. The choice between these systems depends on factors such as material characteristics, distance, and required flow rates. HeadPowder specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of stone aggregate transport, ensuring optimal performance and efficiency.
Key Advantages of Pneumatic Conveying for Stone Aggregate
Implementing pneumatic conveying for stone aggregate transport offers several distinct advantages over conventional methods. First, it eliminates the need for multiple transfer points and equipment, reducing operational complexity and maintenance costs. The enclosed pipeline system also minimizes dust emissions, improving workplace safety and compliance with environmental regulations. Additionally, pneumatic conveying systems provide greater flexibility in layout design, allowing for vertical and horizontal transport in a single pipeline, which is particularly beneficial in confined or multi-level construction sites. Another significant benefit is the ability to transport materials at high speeds, enabling faster material turnover and increased productivity. HeadPowder’s expertise in system design ensures that these advantages are fully realized, with customized solutions that match the specific requirements of each project.
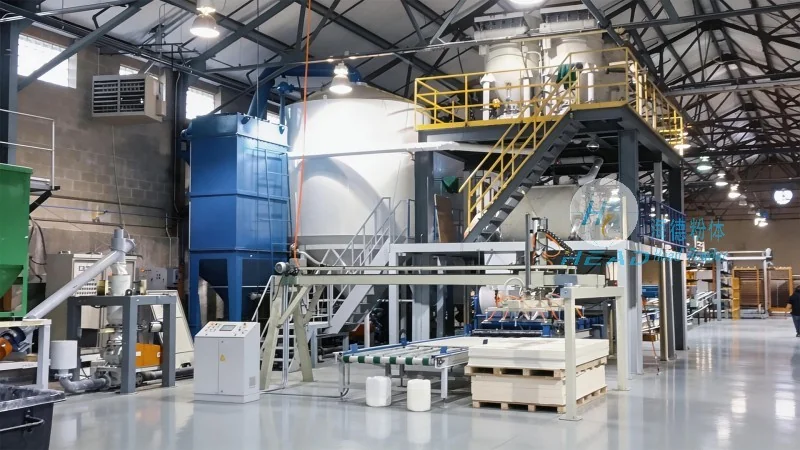
Operational Efficiency and Cost Savings
From an operational perspective, pneumatic conveying systems contribute to substantial cost savings and improved efficiency. By automating the material transport process, companies can reduce labor costs associated with manual handling and loading/unloading. The enclosed system also minimizes material loss, as compared to open conveyors where spillage is common. Furthermore, the ability to integrate with existing infrastructure, such as silos and storage facilities, allows for seamless material flow from extraction to processing. HeadPowder’s engineers work closely with clients to optimize system performance, ensuring that energy consumption is minimized while maintaining high flow rates. This focus on efficiency translates into long-term cost reductions and increased profitability for businesses in the stone aggregate industry.
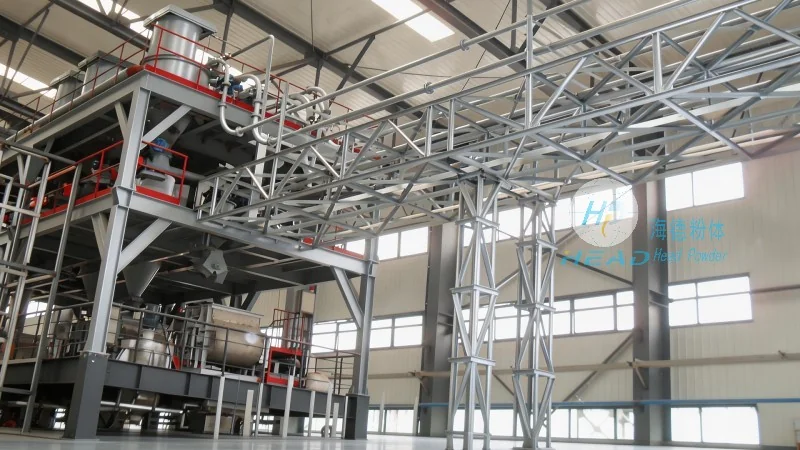
Customized Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying systems, offers comprehensive solutions for bulk transport of stone aggregate. The company, operating under the brand name HeadPowder, leverages decades of experience in material handling technology to design, manufacture, and install customized systems that meet the unique demands of each client. HeadPowder’s team of engineers and technicians conducts thorough site assessments to understand the material characteristics, transport distances, and operational requirements, ensuring that the final system is optimized for performance and reliability. The company’s product line includes a range of components, such as air compressors, cyclone separators, and material feeders, all designed to work in harmony to deliver efficient and reliable transport. HeadPowder’s commitment to quality and customer satisfaction is evident in its ability to deliver systems that not only meet but exceed industry standards.
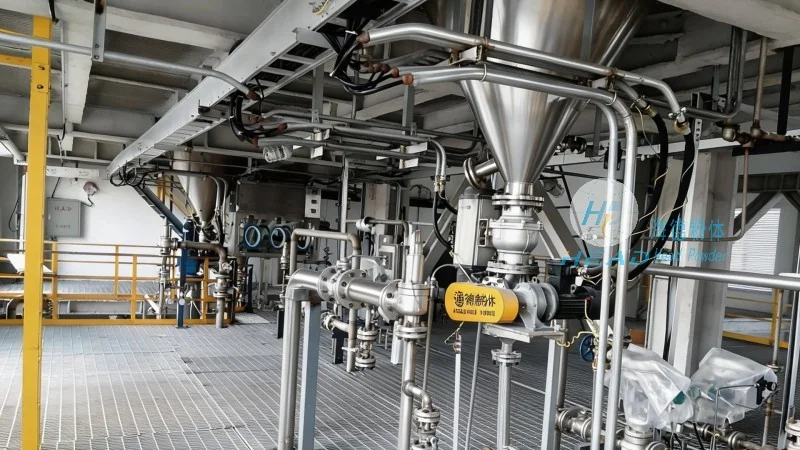
Application Examples and Case Studies
The effectiveness of pneumatic conveying in stone aggregate transport is demonstrated through various real-world applications. For instance, in a large-scale quarry operation, HeadPowder installed a dilute-phase pneumatic conveying system to transport crushed stone from the extraction site to a processing plant over a distance of 2 kilometers. The system successfully handled a flow rate of 50 tons per hour, with minimal pressure drop and low energy consumption. Similarly, in a construction project, the company provided a dense-phase system to transport fine aggregate from a storage silo to a concrete batching plant, ensuring consistent material quality and reducing downtime. These case studies highlight the versatility and reliability of pneumatic conveying systems, making them an ideal choice for both industrial and construction applications. HeadPowder’s expertise in system integration and troubleshooting ensures that clients can rely on their equipment for continuous operation, even in challenging environments.
Future Trends and Technological Advancements
As the demand for efficient material handling continues to grow, pneumatic conveying technology is evolving to meet new challenges. Modern systems now incorporate advanced controls, such as variable frequency drives and real-time monitoring, which allow for precise control of flow rates and energy usage. Additionally, the integration of automation and robotics is enhancing the efficiency of material transport, reducing human intervention and improving safety. HeadPowder remains at the forefront of these technological advancements, continuously investing in research and development to enhance its product offerings. The company’s focus on sustainability is also reflected in its energy-efficient designs, which help clients reduce their carbon footprint while maintaining high performance. As the industry moves towards more sustainable and efficient practices, pneumatic conveying systems will play an increasingly important role in the bulk transport of stone aggregate.




