Pneumatic conveying systems have become a cornerstone technology in the pharmaceutical industry, particularly for the efficient and safe handling of powdered medicines. These systems utilize air or other gases to transport powders through a closed pipeline, offering significant advantages over traditional mechanical conveying methods, including minimal product contamination, reduced risk of cross-contamination, and enhanced process control. Understanding the various types of pneumatic conveying systems and their practical applications is essential for pharmaceutical manufacturers seeking to optimize their powder handling processes and maintain regulatory compliance.
Types of Pneumatic Conveying Systems
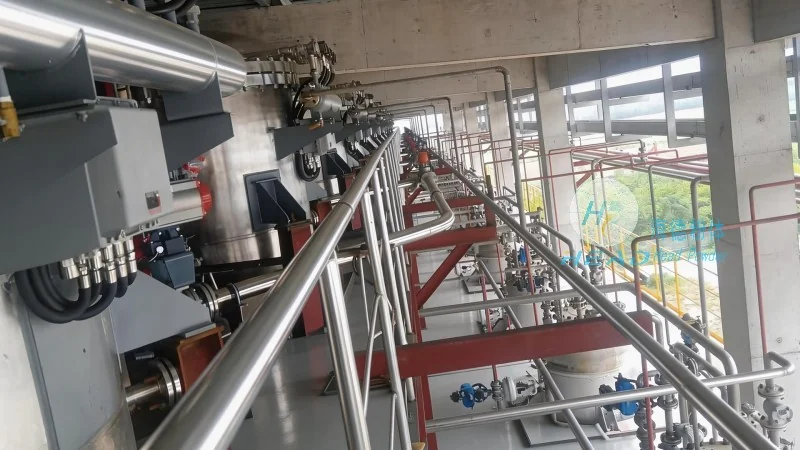
Two primary categories of pneumatic conveying systems are widely used in pharmaceutical applications: aspirating (suction) systems and blowing (pressure) systems. The choice between these systems depends on factors such as the powder source location, elevation changes, and the required flow rate.
Aspirating systems operate by creating a negative pressure at the inlet, drawing powder from a hopper or storage container into the conveying line. This method is ideal for applications where the powder source is at a higher elevation than the destination, as it leverages gravity and pressure differentials to move material. The system typically employs a vacuum pump to generate suction, and the air-powder mixture is separated at the discharge point using a cyclone or filter to recover the powder and return air to the system.
Conversely, blowing systems generate positive pressure at the discharge end, pushing the powder through the pipeline. These systems are commonly used when the powder source is at a lower level than the destination, as they can effectively lift and transport material against gravity. Blowing systems often utilize a positive displacement blower or a rotary lobe pump to provide the necessary pressure, ensuring consistent and reliable material transport. The design of the system, including the type of pump and pipeline configuration, is critical to achieving optimal performance.
Practical Applications in Pharmaceutical Manufacturing
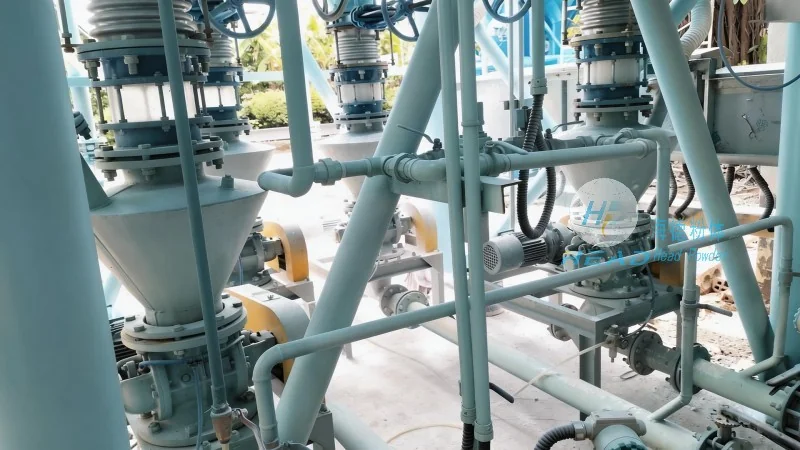
The practical applications of pneumatic conveying systems in pharmaceutical manufacturing are diverse and critical for maintaining product quality and safety standards. One of the most common uses is in the transfer of active pharmaceutical ingredients (APIs) and other fine powders from bulk storage to processing equipment, such as mixers, granulators, or tablet presses. This closed-system approach minimizes exposure to environmental contaminants and ensures that the powders remain within a controlled environment throughout the transfer process.
Another key application is in the handling of excipients, including fillers, binders, and coatings, which are essential components in the formulation of pharmaceutical products. Pneumatic conveying allows for precise and controlled addition of these excipients during the manufacturing process, ensuring uniform mixing and consistent product quality. The ability to handle these materials in a closed system also helps maintain the required cleanliness levels, which is particularly important for products that require sterile or aseptic processing.
Furthermore, pneumatic conveying systems are widely used in the cleanroom environments of pharmaceutical facilities. The enclosed nature of these systems helps maintain the required cleanliness levels, as the air and powder are contained within the pipeline and processing equipment. This is crucial for preventing contamination and ensuring that the final product meets regulatory standards for purity and safety.
Advantages and Considerations
While pneumatic conveying systems offer numerous benefits, such as improved safety, reduced labor costs, and enhanced process efficiency, there are also considerations to be made. The choice of system type depends on factors like the powder characteristics (e.g., particle size, moisture content, flowability), the distance and elevation changes between the source and destination, and the required flow rate. For example, cohesive or sticky powders may require specialized equipment, such as a rotary valve or a vibratory feeder, to ensure smooth and consistent transport.
Additionally, the design and maintenance of pneumatic conveying systems must adhere to strict regulatory standards, particularly in the pharmaceutical industry. This includes ensuring that the system is constructed from materials that are compatible with the powders being handled and that the air filtration and separation systems are effective in preventing product loss and cross-contamination. Regular maintenance and cleaning are also essential to prevent buildup and ensure long-term system performance.
About HeadPowder: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of pneumatic conveying solutions tailored for the pharmaceutical industry. With operations based in Shandong, China, the company specializes in designing, manufacturing, and installing customized conveying systems that meet the stringent requirements of pharmaceutical manufacturing. HeadPowder's expertise lies in understanding the unique challenges of powder handling in the industry and providing innovative solutions that enhance process efficiency, product quality, and regulatory compliance.
The company's team of engineers and technicians work closely with clients to assess their specific powder handling needs and develop tailored solutions. Whether it's a new facility setup or an upgrade to an existing system, HeadPowder offers comprehensive services, including system design, equipment selection, installation, and maintenance. By leveraging advanced technology and a deep understanding of pharmaceutical processes, HeadPowder helps pharmaceutical manufacturers optimize their powder handling operations and achieve their production goals.
HeadPowder's commitment to quality and customer satisfaction is reflected in its adherence to industry standards and continuous improvement initiatives. The company invests in research and development to stay at the forefront of technological advancements in pneumatic conveying systems, ensuring that its clients receive the most effective and reliable solutions for their powder handling needs. Through its expertise and dedication to excellence, HeadPowder plays a vital role in supporting the pharmaceutical industry's pursuit of safe, efficient, and high-quality manufacturing processes.




