HeadPowder, a prominent engineering firm headquartered in Shandong, China, is dedicated to providing cutting-edge pneumatic conveying solutions for the mineral and sand sectors. This technology represents a sophisticated approach to bulk material transport, offering advantages such as flexibility, reliability, and the ability to handle a wide range of materials. The following exploration covers the foundational principles, practical applications, and evolving trends of pneumatic conveying, highlighting how it enhances operational efficiency and safety in industrial settings.
Principles of Pneumatic Conveying
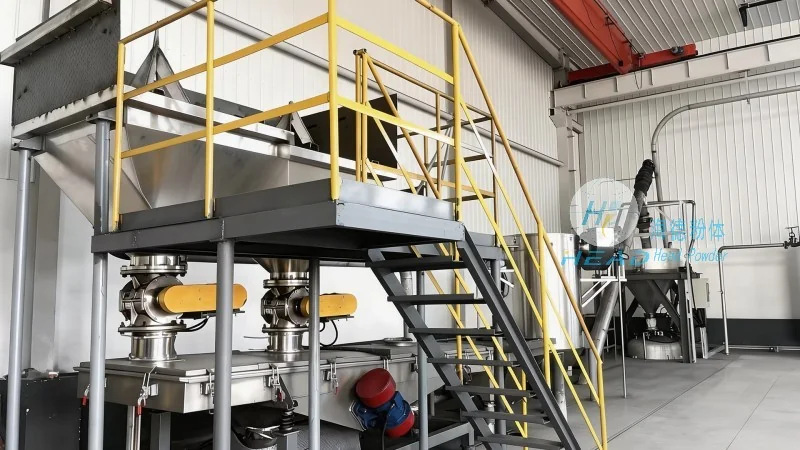
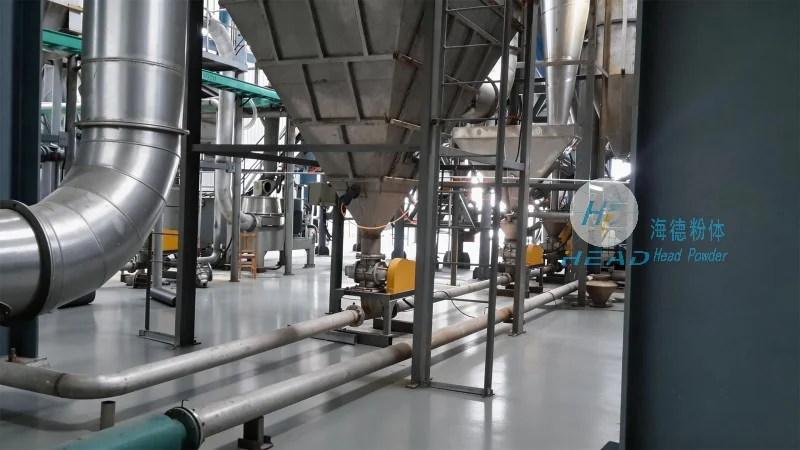
The fundamental principle of pneumatic conveying involves utilizing a gas stream, predominantly air, to transport solid materials through a pipeline network. This process relies on creating a pressure differential that propels the material along the conveying line. Two primary system types are widely used: dilute-phase and dense-phase. Dilute-phase systems operate at lower pressures, moving materials in a suspended state, making them suitable for short to medium distances and lower material loads. Dense-phase systems, conversely, use higher pressures and lower air-to-material ratios, transporting materials in a more compacted form, which is ideal for longer distances and higher material densities. The selection of a system type depends on factors like material characteristics, conveying distance, and operational requirements. HeadPowder's engineering expertise enables the design and implementation of both system types, ensuring that each solution is optimized for the specific needs of the client, whether it involves handling abrasive ores, fine sand, or other bulk materials.
Applications in the Mineral and Sand Industry
In the mineral and sand industry, pneumatic conveying plays a critical role in various processing stages. In mining operations, it is commonly employed to transport crushed ores from processing plants to storage facilities or for further refinement. This method offers significant advantages over traditional mechanical conveyors, such as reduced mechanical wear and the ability to handle abrasive materials without degradation. The technology also minimizes the risk of material contamination and dust exposure, enhancing workplace safety. In the sand and gravel sector, pneumatic conveying is essential for moving sand from quarries to manufacturing plants, construction sites, or for use in concrete production. It effectively reduces dust generation and ensures the sand remains free from contaminants, which is crucial for maintaining product quality and meeting environmental regulations. Furthermore, in the chemical and pharmaceutical industries, where fine powders are involved, pneumatic conveying ensures precise and hygienic material handling, preventing cross-contamination and preserving product purity. HeadPowder's customized solutions address these diverse applications, ensuring that the conveying process is both efficient and compliant with industry standards.
Advancements and Development Trends
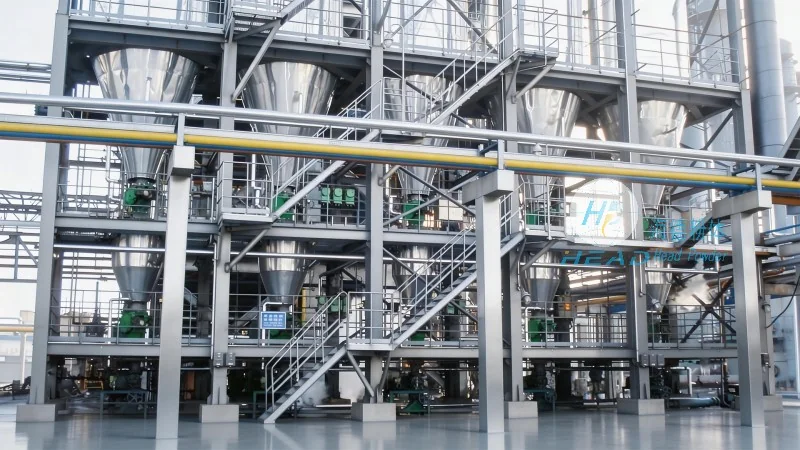
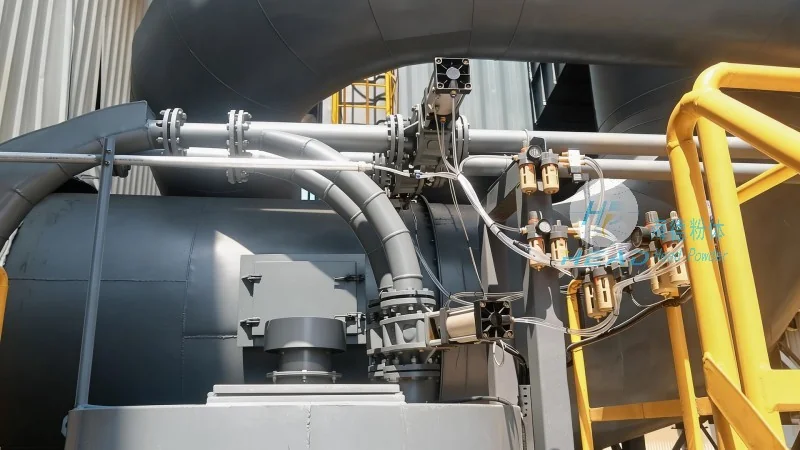
The pneumatic conveying technology landscape is continuously advancing, driven by the demand for higher efficiency, lower energy consumption, and improved material handling capabilities. Recent innovations focus on enhancing system performance through advanced control and monitoring systems. The integration of sensors and automated control mechanisms allows for real-time tracking of conveying parameters, enabling immediate adjustments to maintain optimal operation. This not only boosts efficiency but also reduces downtime and maintenance costs. Another key trend is the development of more energy-efficient systems, including compressed air recovery and recycling technologies. These advancements help minimize operational costs and environmental impact by reducing energy waste. Additionally, the adoption of sustainable materials and eco-friendly practices in system construction is becoming increasingly important, aligning with global environmental regulations and corporate sustainability objectives. HeadPowder remains committed to these advancements, investing in research and development to integrate the latest technologies into their solutions. By doing so, they ensure their clients benefit from the most advanced and effective pneumatic conveying systems, supporting their operational goals and contributing to a more sustainable industrial future.




