Shandong HeadPowder Engineering Co., Ltd., a leading enterprise based in Shandong, China, specializes in the design, manufacturing, and installation of advanced dust removal and material conveying systems. With a strong commitment to technological innovation and customer satisfaction, the company has established itself as a trusted partner in the field of industrial air filtration and material handling solutions.
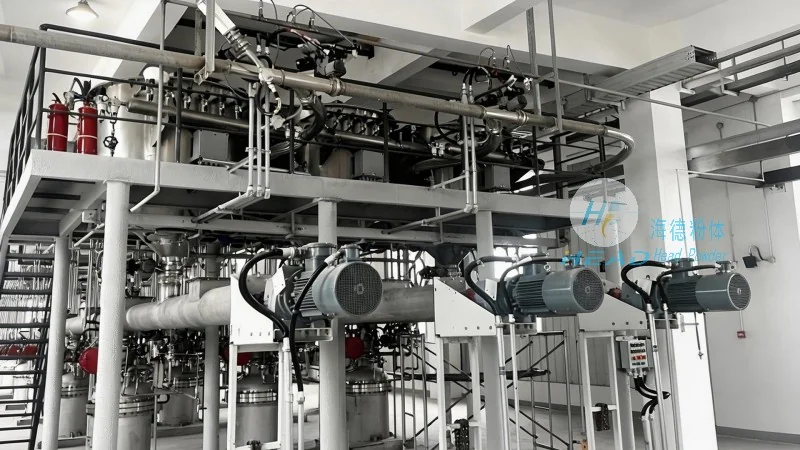
At the core of HeadPowder's product portfolio is the gravity dust removal and ash conveying system, a sophisticated solution engineered to efficiently handle the challenges of industrial dust and ash management. This system combines the principles of gravity separation with pneumatic conveying technology, offering a reliable and cost-effective approach to transporting fine particles and ash from various industrial processes.
Understanding the Gravity Dust Removal and Ash Conveying System
The gravity dust removal system operates by utilizing the natural settling velocity of particles under the influence of gravity. As contaminated air passes through the system, larger and heavier particles are separated from the air stream due to their higher mass, while finer particles remain suspended. This separation process is typically achieved through a series of chambers or chambers with varying cross-sectional areas, allowing for effective particle classification based on size and density.
Following the dust removal stage, the ash and fine particles are then transferred to the pneumatic conveying section. This part of the system employs a low-pressure air stream to transport the collected material through a network of pipes to the designated disposal or processing location. The gravity ash conveying system is designed to handle a wide range of ash types, including fly ash, bottom ash, and other industrial residues, with minimal energy consumption and operational complexity.
Key Advantages and Features of Gravity Ash Pneumatic Conveying
One of the primary advantages of the gravity dust removal and ash conveying system is its energy efficiency. By leveraging gravity for the initial separation of particles, the system reduces the need for high-pressure air or mechanical pumps, resulting in lower operational costs and reduced energy consumption compared to traditional conveying methods. This makes it an ideal solution for industries seeking to minimize their environmental footprint and operational expenses.
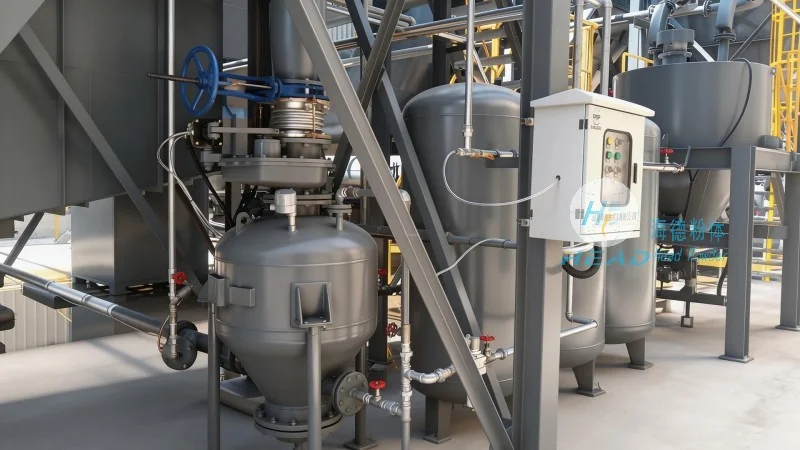
Another significant feature is the system's ability to handle a wide variety of particle sizes and densities. The gravity separation mechanism effectively separates coarse particles from fine dust, ensuring that the conveyed material is free from oversized debris that could cause blockages or damage to downstream equipment. This capability enhances the overall reliability and longevity of the conveying system, reducing maintenance requirements and downtime.
The pneumatic conveying component of the system also offers flexibility in terms of layout and integration with existing industrial facilities. The low-pressure air system can be easily adapted to various pipe configurations and distances, allowing for customized solutions that fit the specific requirements of each application. This adaptability makes the gravity ash conveying system suitable for a wide range of industrial settings, from power plants and cement factories to metal processing and chemical production facilities.
Applications and Benefits in Industrial Settings
The gravity dust removal and ash conveying system is widely used in industries where the efficient handling of dust and ash is critical to operational efficiency and environmental compliance. In power generation, for example, the system is employed to transport fly ash from boiler systems to storage silos or disposal sites, ensuring that the ash is managed in a controlled and environmentally responsible manner.
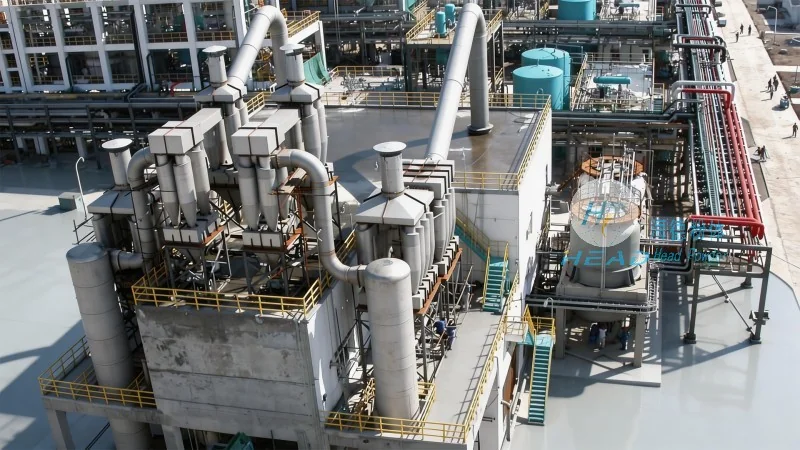
In cement manufacturing, the system helps to remove and convey ash from the kiln and other processing stages, contributing to a cleaner production environment and reduced emissions. Similarly, in metal processing and chemical industries, the system is utilized to handle various industrial residues, improving the overall safety and sustainability of material handling operations.
By integrating the gravity separation and pneumatic conveying technologies, the system provides a comprehensive solution that addresses both the removal of dust and the efficient transport of ash. This dual functionality not only enhances operational efficiency but also contributes to improved workplace safety by reducing the exposure of personnel to airborne particles and dust.
Conclusion and Company Commitment
Shandong HeadPowder Engineering Co., Ltd. continues to innovate and refine its gravity dust removal and ash conveying systems to meet the evolving needs of modern industrial applications. With a focus on quality, reliability, and customer-centric solutions, the company remains dedicated to providing advanced material handling technologies that enhance operational performance while minimizing environmental impact.
For industries seeking a reliable and efficient solution for dust and ash management, the gravity ash pneumatic conveying system from HeadPowder offers a proven and effective approach. By combining the principles of gravity separation with pneumatic conveying, this system delivers superior performance, energy efficiency, and flexibility, making it an ideal choice for a wide range of industrial applications.




