For industries dealing with borax granules, efficient and reliable material handling is crucial to maintaining production efficiency and product quality. The borax granule conveying system, particularly through pneumatic conveying technology, has emerged as a key solution in modern material transport. This article provides an overview of the borax granule conveying system, highlighting its design, operational advantages, and the key benefits of pneumatic conveying for handling borax granules.
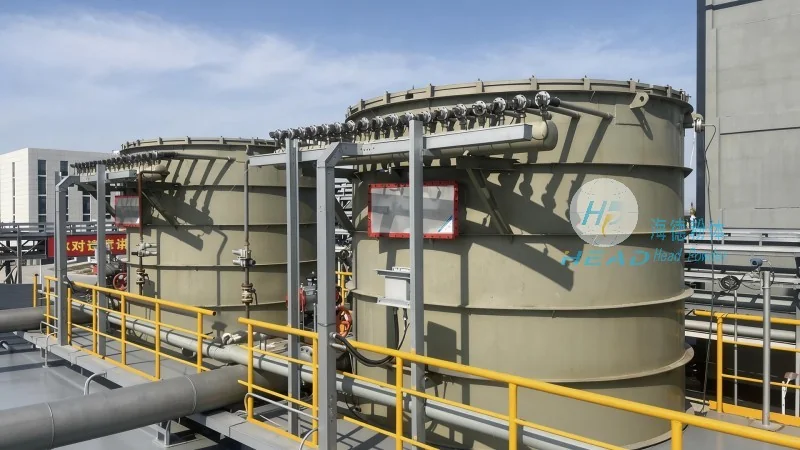
HeadPowder: A Leading Provider of Borax Conveying Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier based in Shandong, China. With years of experience in the field of material handling equipment, HeadPowder specializes in designing and manufacturing advanced borax granule conveying systems tailored to meet the specific needs of various industrial applications. The company's commitment to quality, innovation, and customer satisfaction has established it as a trusted partner for businesses seeking efficient and reliable borax granule transport solutions.
Understanding Borax Granule Conveying Systems
Borax granule conveying systems are engineered to transport borax granules from storage silos or production lines to processing units or packaging areas. These systems typically consist of components such as hoppers, feeders, pneumatic conveying lines, and control systems. The design of the system is tailored to the physical properties of borax granules, including their size, density, and flow characteristics, ensuring optimal performance and minimal material degradation during transport.
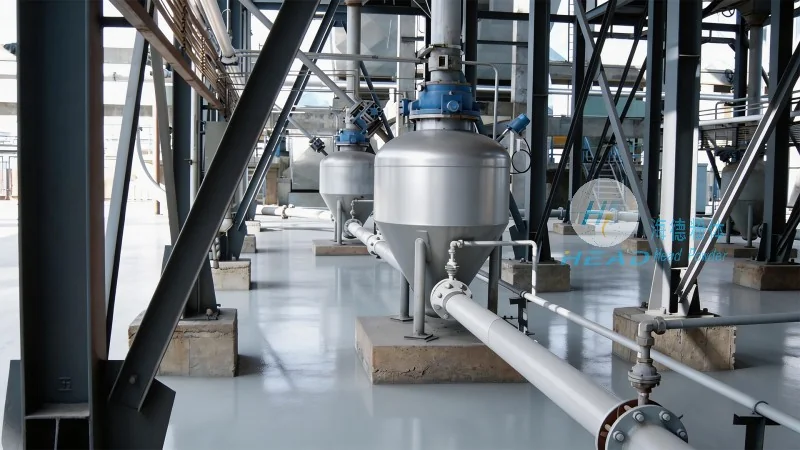
The Advantages of Pneumatic Conveying for Borax Granules
Pneumatic conveying, as a method for transporting borax granules, offers several distinct advantages over traditional mechanical conveying systems. One of the primary benefits is the ability to handle the material in a closed system, which helps to prevent contamination from external sources and reduces dust emissions, thereby improving workplace safety and environmental compliance. Additionally, pneumatic conveying systems can achieve high transport speeds and cover longer distances with minimal energy consumption compared to other methods.
Key Features of the Borax Granule Pneumatic Conveying System
The borax granule pneumatic conveying system developed by HeadPowder incorporates several key features that enhance its performance and reliability. These features include: a) High-capacity feeders that ensure consistent material flow; b) Advanced control systems that monitor and adjust the conveying process in real-time; c) Durable and corrosion-resistant materials used in the construction of the conveying lines and components to withstand the chemical properties of borax; d) Integrated dust collection and filtration systems to maintain air quality and comply with environmental regulations. The system is designed to be flexible, allowing for easy integration with existing production lines and scalable to accommodate varying production volumes.
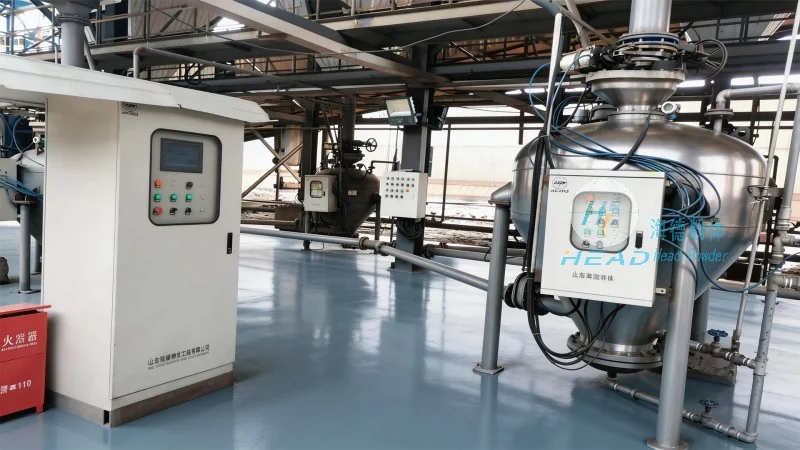
Operational Benefits and Efficiency Improvements
Implementing a borax granule pneumatic conveying system can lead to significant operational benefits for industrial facilities. By reducing material handling time and labor costs, the system enhances overall production efficiency. The closed-loop design minimizes material loss and contamination, leading to higher product purity and quality. Furthermore, the energy-efficient operation of pneumatic conveying systems contributes to lower operational costs and a reduced environmental footprint. These advantages make the system an attractive investment for businesses looking to modernize their material handling processes and improve their competitive edge in the market.
Conclusion
In conclusion, the borax granule conveying system, particularly utilizing pneumatic conveying technology, represents a highly effective solution for the efficient and reliable transport of borax granules. With its ability to handle the material in a closed system, reduce dust emissions, and improve operational efficiency, this technology offers significant benefits for industrial applications. HeadPowder, with its expertise and commitment to quality, provides comprehensive borax conveying solutions that meet the evolving needs of the industry. By investing in advanced borax granule conveying systems, businesses can enhance their production capabilities, ensure product quality, and achieve sustainable operational performance.




