Understanding the fundamental principles and applications of additive pneumatic conveying systems is crucial for industries that rely on efficient material handling. These systems utilize air to transport bulk materials, offering a versatile solution for moving additives and other powders with precision and reliability. The technology has evolved significantly, providing enhanced control over flow rates, particle size distribution, and overall system performance. By leveraging the power of compressed air, these systems enable seamless integration into production workflows, reducing downtime and improving operational efficiency.
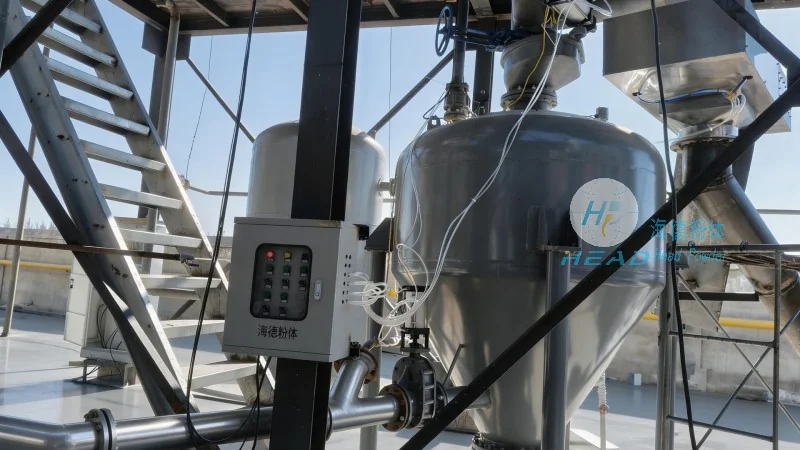
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field, specializes in the design, development, and implementation of advanced pneumatic conveying solutions. With a strong focus on innovation and customer-centric approaches, the company has established itself as a trusted partner for businesses seeking reliable material handling systems. HeadPowder's expertise spans various industries, including pharmaceuticals, food processing, and chemical manufacturing, where the quality and safety of conveyed materials are paramount. The company is headquartered in Shandong, China, and its state-of-the-art facilities enable the production of high-quality equipment that meets international standards.
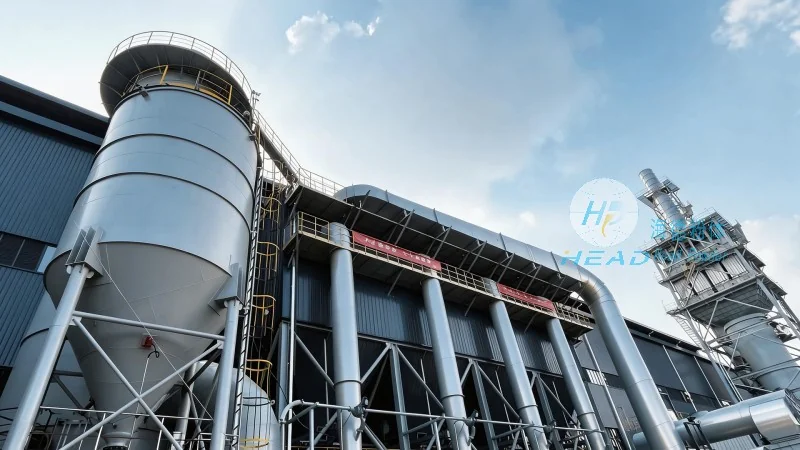
Key Features and Advantages of Additive Pneumatic Conveying Systems
One of the primary advantages of these systems is their ability to handle a wide range of additive types, from fine powders to bulk materials. The technology allows for precise control over the conveying process, ensuring minimal product degradation and consistent quality. Additionally, pneumatic conveying systems are highly flexible, enabling easy integration with existing production lines and the ability to transport materials over long distances without the need for complex infrastructure. The systems also offer improved safety by eliminating the need for manual handling of hazardous materials, reducing the risk of accidents and contamination. Furthermore, the energy efficiency of these systems makes them a cost-effective choice for long-term operation, with lower maintenance costs compared to traditional mechanical conveying methods.
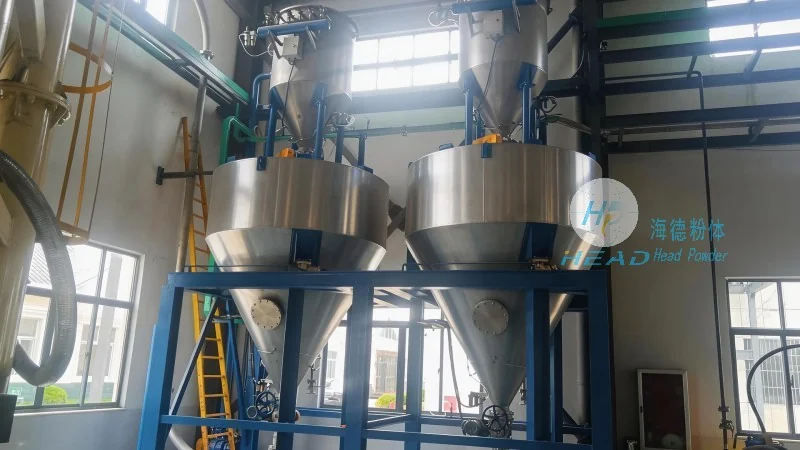
Applications in Various Industries
Additive pneumatic conveying systems are widely used across multiple sectors, each benefiting from the unique capabilities of the technology. In the pharmaceutical industry, for example, these systems are essential for transporting active pharmaceutical ingredients (APIs) and excipients with strict purity standards. The gentle handling and low contamination risk make them ideal for maintaining product integrity, ensuring that final products meet regulatory requirements. Similarly, in the food processing sector, the systems are used to convey ingredients like spices, vitamins, and flavorings, providing a hygienic and efficient method for material transport. Chemical manufacturers also rely on these systems to handle reactive or corrosive additives, offering a safe and reliable solution for material handling. The versatility of the technology also makes it suitable for other industries, such as cosmetics and agricultural products, where precise control over additive distribution is critical.
System Components and Operational Principles
The core components of an additive pneumatic conveying system typically include a material feed hopper, a conveyor line (often with a series of ducts and valves), a blower or compressor to generate airflow, and a collection bin or processing unit. The system operates by drawing air through the conveyor line and using it to lift and transport the additive particles. The airflow velocity is carefully controlled to ensure that the particles are carried efficiently without causing excessive wear on the system components. The design of the system, including the size and shape of the ducts and the placement of valves, plays a critical role in optimizing the conveying process and minimizing energy consumption. Modern systems may also incorporate sensors and control systems to monitor and adjust the airflow in real-time, ensuring optimal performance under varying conditions.
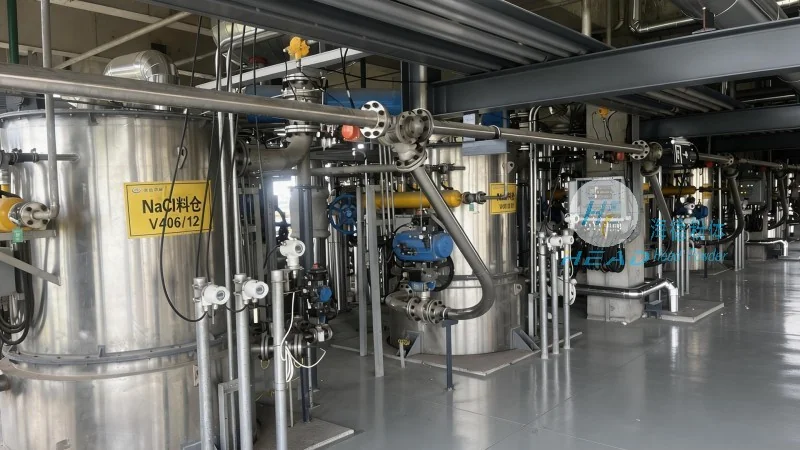
Customized Solutions for Diverse Needs
HeadPowder understands that each client has unique requirements, and the company offers tailored solutions to meet these needs. Whether it's a small-scale system for a laboratory or a large-scale system for an industrial plant, HeadPowder's engineers work closely with clients to design systems that are efficient, cost-effective, and compliant with industry standards. The company's commitment to quality is evident in its use of high-grade materials and rigorous testing procedures, ensuring that each system performs reliably over its service life. With a strong focus on customer support, HeadPowder provides comprehensive after-sales services, including maintenance, repair, and technical assistance, to ensure that clients can maximize the performance and lifespan of their equipment. The company also offers training programs for operators and maintenance staff, helping to ensure that the systems are used correctly and efficiently.




