For coffee processing facilities, efficient and reliable material handling is crucial to maintaining production efficiency and product quality. The coffee bean material pneumatic conveying line is a specialized system designed to transport coffee beans and other related materials with precision and minimal loss. This article will explore the operation process and working principles of such a system, highlighting its key components, operational workflow, and the benefits it offers to coffee processing operations.
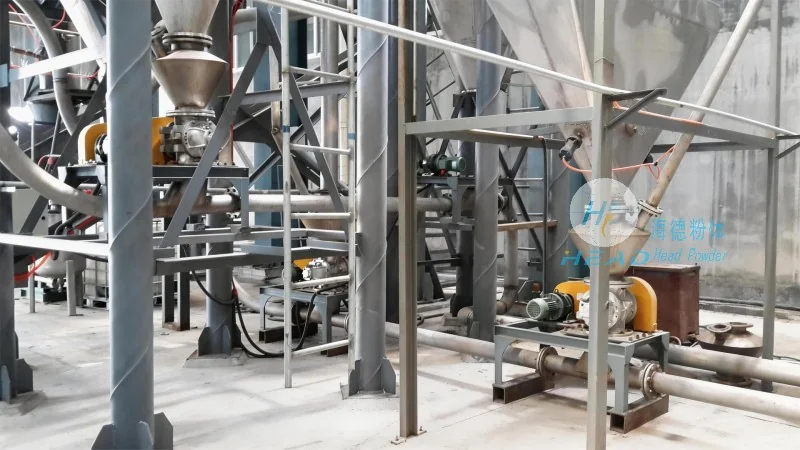
Key Components of the Coffee Bean Pneumatic Conveying Line
The coffee bean pneumatic conveying line typically consists of several essential components that work in tandem to ensure smooth material transport. These components include the material hopper, which serves as the storage and feeding unit; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying pipeline, which forms the transport path; and the control system, which regulates the flow and pressure. Additionally, accessories like check valves, filters, and dust collectors may be integrated to enhance system performance and safety.
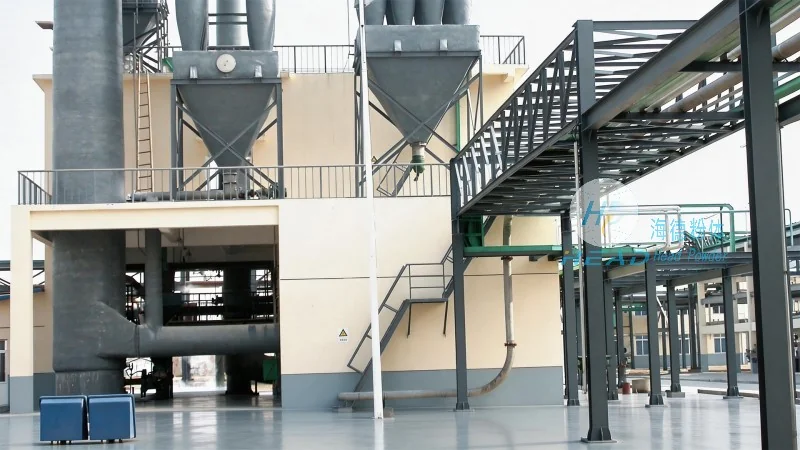
Working Principle of the Pneumatic Conveying System
The operation of the coffee bean pneumatic conveying line is based on the principle of air flow and pressure differential. When the system is activated, the air compressor draws in ambient air and compresses it to a specific pressure. This pressurized air is then introduced into the conveying pipeline, creating a flow that propels the coffee beans forward. The material hopper feeds the coffee beans into the pipeline at a controlled rate, ensuring a consistent flow. As the air and coffee beans move through the pipeline, the system maintains a stable pressure to prevent material backflow and ensure efficient transport. The control system monitors parameters such as pressure, flow rate, and material level, adjusting the operation as needed to maintain optimal performance.
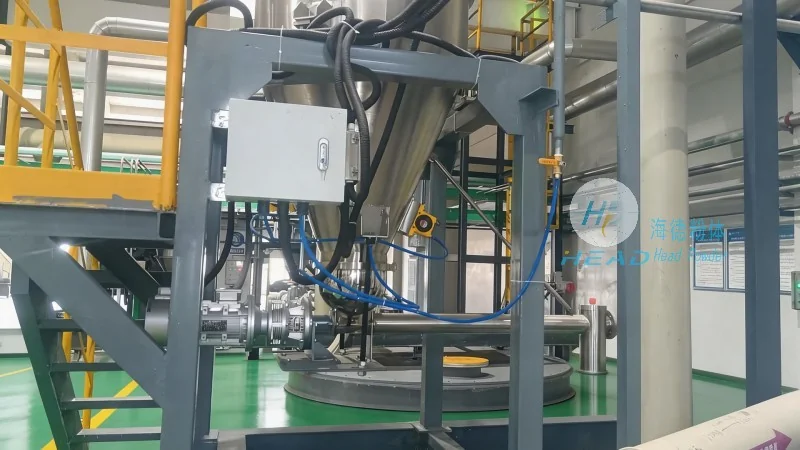
Operation Process: From Hopper to Destination
The operation process of the coffee bean pneumatic conveying line involves several sequential steps that ensure the smooth transfer of coffee beans from the source to the destination. The process begins with the loading of coffee beans into the material hopper. The hopper is equipped with a feeding mechanism, such as a rotary valve or a screw feeder, which regulates the amount of material released into the pipeline. As the air compressor starts, the pressurized air is introduced into the pipeline, creating a vacuum or pressure differential that moves the coffee beans forward. The coffee beans travel through the pipeline, which may include bends, elbows, or vertical sections, all designed to accommodate the flow without causing blockages or damage to the beans. At the destination, the coffee beans are discharged into a receiving hopper or storage silo. The system may also include a dust collection system to capture any airborne particles, ensuring a clean and safe working environment.
Benefits and Advantages of the Coffee Bean Pneumatic Conveying Line
Implementing a coffee bean pneumatic conveying line offers numerous benefits for coffee processing operations. Firstly, it provides a dust-free and hygienic method of material transport, which is essential for maintaining product quality and compliance with food safety standards. The system minimizes material handling and reduces the risk of contamination, as the beans are transported in a closed pipeline. Secondly, the pneumatic conveying line offers high efficiency and speed, allowing for rapid transfer of large quantities of coffee beans. This improves overall production throughput and reduces downtime. Additionally, the system is flexible and can be easily integrated with existing processing equipment, adapting to various production requirements. The low maintenance requirements and long service life of the components also contribute to cost savings over time.
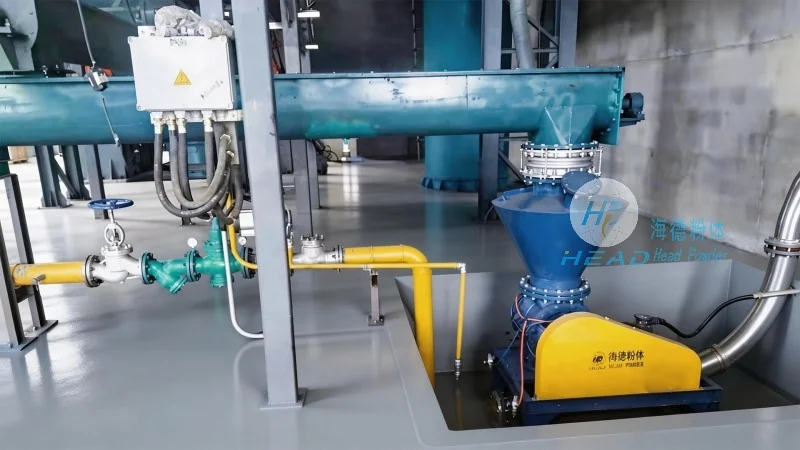
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of advanced material handling systems, including coffee bean pneumatic conveying lines. With a focus on innovation and quality, the company specializes in designing and manufacturing customized solutions tailored to the specific needs of coffee processing facilities. HeadPowder's team of experienced engineers and technicians utilizes cutting-edge technology and rigorous testing to ensure that each system meets the highest standards of performance and reliability. The company's facilities are located in Shandong, China, where it leverages local expertise and resources to deliver superior products and services to clients worldwide. By choosing headpowder, coffee processing operations can benefit from reliable, efficient, and cost-effective material handling solutions that enhance their productivity and product quality.




