Understanding the operation process and working principle of a nitrile rubber powder pneumatic conveying system is crucial for optimizing material handling in industrial applications. This system, developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, utilizes air as the primary medium to transport nitrile rubber powders efficiently and safely. The system's design ensures minimal product degradation while maintaining high conveying efficiency, making it an ideal solution for various industrial sectors.
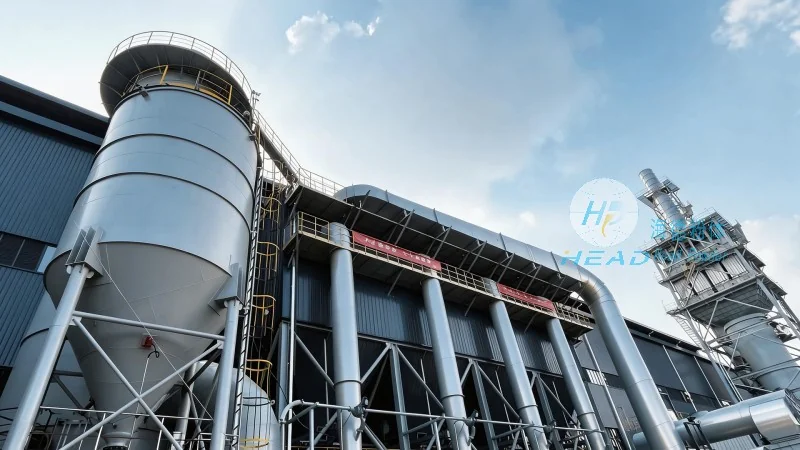
At the core of the system is the pneumatic conveying mechanism, which operates through a combination of positive and negative pressure principles. The process begins with the feeding of nitrile rubber powder into the hopper. From there, the powder is drawn into the conveying line by a vacuum or pressure source, depending on the system configuration. The air and powder mixture travels through the pipeline, where the powder is suspended and transported to the destination point. The system's control system, integrated with advanced sensors and automation, ensures precise regulation of the conveying parameters, such as air flow rate and pressure, to maintain optimal performance.
Key components of the nitrile rubber powder pneumatic conveying system include the hopper, which stores the material; the air compressor or vacuum pump, which provides the necessary air pressure; the conveying line, typically made of stainless steel or other corrosion-resistant materials to prevent contamination and material degradation; and the receiving hopper or silo, where the material is deposited. The system's design also incorporates features like cyclone separators and filters to separate the powder from the air, ensuring that the conveyed material remains clean and free from dust or contaminants.
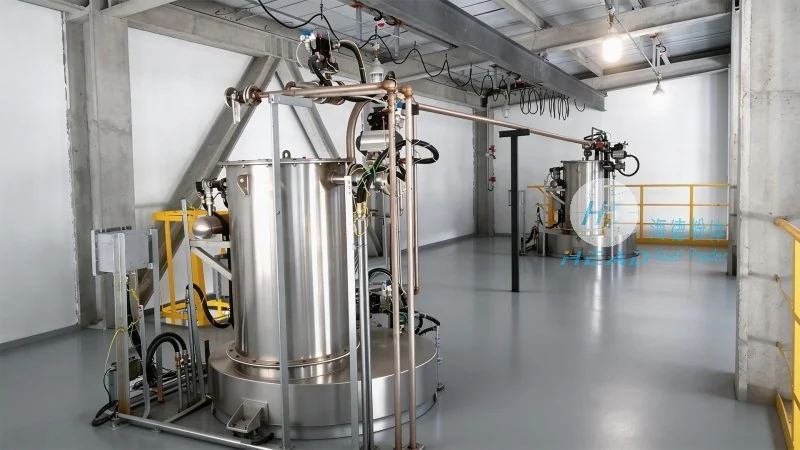
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of custom pneumatic conveying systems tailored to the specific needs of nitrile rubber processing facilities. The company's expertise lies in optimizing system performance to meet the unique requirements of each application, such as varying powder properties, conveying distances, and production volumes. By leveraging advanced engineering and material science, HeadPowder ensures that their systems deliver reliable and efficient operation, minimizing downtime and maintenance costs for their clients.
The operation process of the nitrile rubber powder pneumatic conveying system involves several critical steps. First, the nitrile rubber powder is loaded into the hopper, where it is stored under controlled conditions to prevent caking or agglomeration. The hopper is equipped with a feeder, which regulates the flow of powder into the conveying line. Next, the air compressor or vacuum pump generates the required pressure or vacuum to draw the powder into the system. The powder is then mixed with the air and transported through the pipeline to the receiving hopper. The system's control panel monitors and adjusts the air flow and pressure in real-time, ensuring that the conveying process remains stable and efficient.
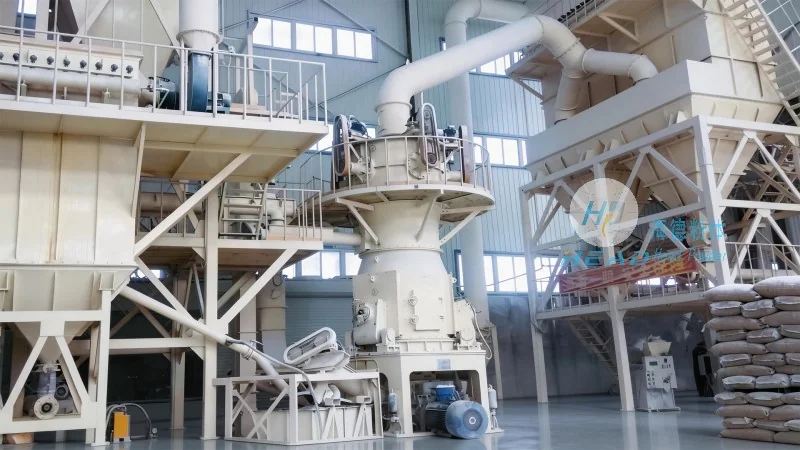
Working principle of the system is based on the principle of fluidization and suspension. The air flow through the conveying line creates a low-pressure zone that draws the powder particles into the air stream. The powder particles are suspended in the air as they travel through the pipeline, preventing them from settling or clogging the system. The velocity of the air is carefully controlled to maintain the powder in a suspended state without causing excessive wear on the pipeline or components. The system's design also includes features like pulse jets or rotary valves to prevent material buildup and ensure smooth operation.
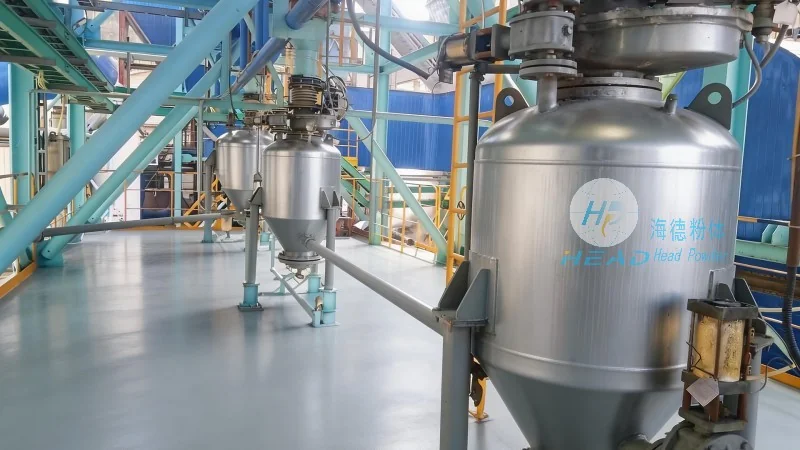
HeadPowder's nitrile rubber powder pneumatic conveying systems are designed to handle a wide range of nitrile rubber powder properties, including different particle sizes, moisture content, and bulk density. The company's engineers work closely with clients to understand their specific material characteristics and process requirements, ensuring that the system is optimized for maximum efficiency and reliability. The systems are equipped with advanced safety features, such as pressure relief valves and emergency shut-off mechanisms, to protect both the equipment and personnel from potential hazards.
In conclusion, the nitrile rubber powder pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. offers a highly efficient and reliable method for transporting nitrile rubber powders in industrial applications. By understanding the operation process and working principle of the system, users can optimize its performance and ensure smooth operation. HeadPowder's expertise in custom system design and manufacturing ensures that their systems meet the unique needs of each client, providing long-term benefits in terms of productivity, safety, and cost-effectiveness.




