

Operation Process and Working Principle of Gravity Dust Removal Powder Conveying System
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced gravity dust removal and powder conveying systems. This article provides a detailed overview of the operation process and working principles of such systems, highlighting their efficiency and reliability in industrial applications.
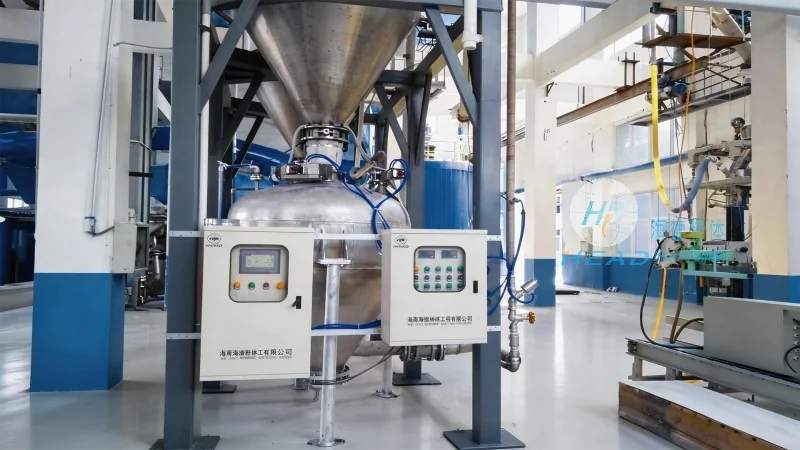
System Overview and Core Components
The gravity dust removal powder conveying system is engineered to efficiently collect and transport fine powders and dust particles from industrial processes. The system typically consists of several key components, including a dust collection hopper, a gravity separator, a conveying pipeline, and a discharge outlet. Each component plays a critical role in ensuring the smooth operation of the entire system.
Working Principle of Gravity Dust Removal
The core of the system lies in the gravity dust removal mechanism. As contaminated air enters the dust collection hopper, the larger dust particles are separated from the air stream due to their higher density. These particles settle under the influence of gravity and are collected in the hopper. The remaining air, now relatively clean, continues to flow through the system. This separation process effectively reduces the load on subsequent filtration or cleaning stages, enhancing overall system efficiency.
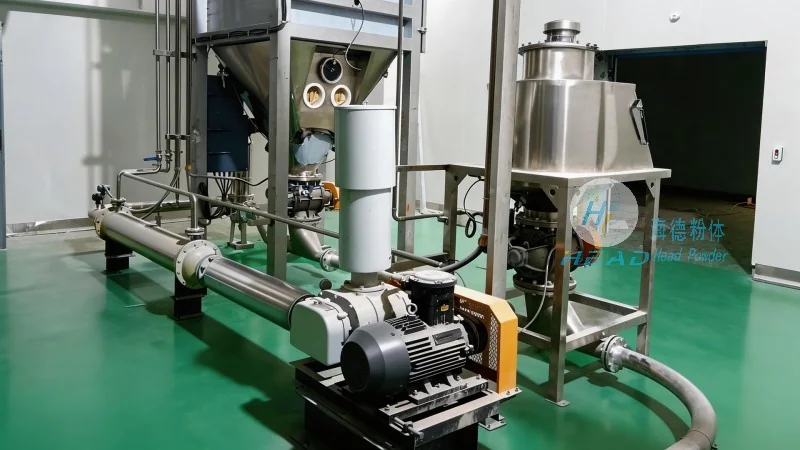
Working Principle of Powder Conveying
Following the dust removal stage, the clean air is directed into the conveying pipeline. The system utilizes a combination of low-pressure air and gravity to transport the remaining fine powders. The air flow creates a slight negative pressure in the pipeline, which draws the powders along with the air stream. The gravity component helps maintain the flow of powders, especially in horizontal or slightly inclined sections of the pipeline. This method ensures a continuous and stable powder conveying process without the need for high-pressure or mechanical pumps.
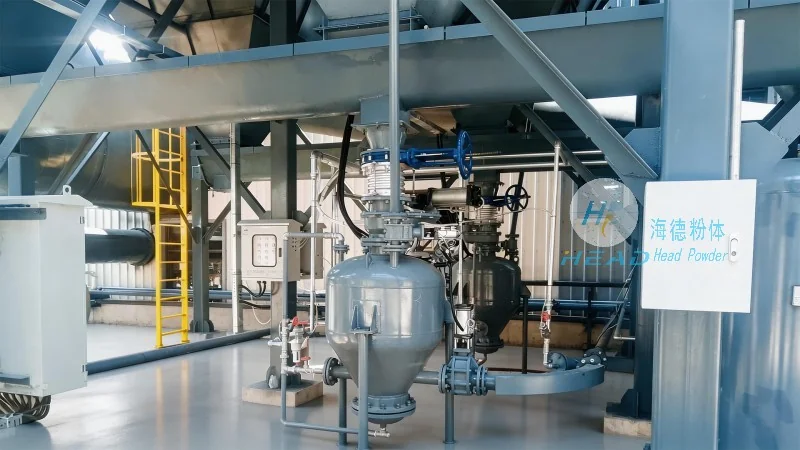
Operation Process: Step-by-Step Guide
The operation of the gravity dust removal powder conveying system follows a systematic process to ensure optimal performance. The steps are as follows:
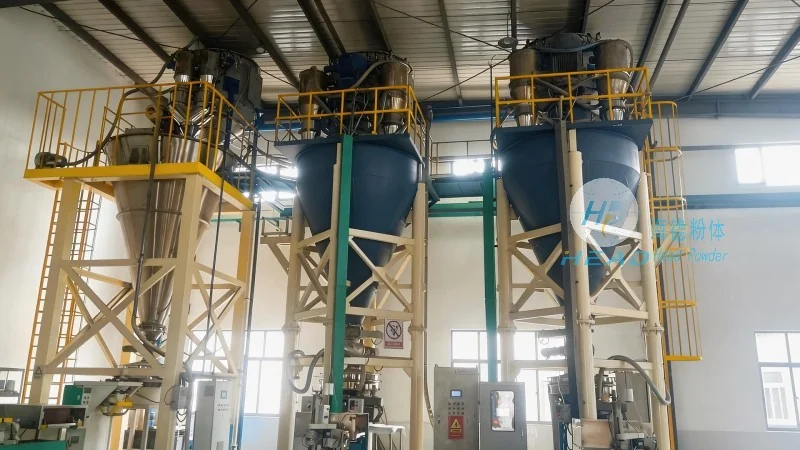
- System Preparation: Before startup, all components are inspected for proper alignment, tight connections, and the absence of obstructions. The dust collection hopper is checked for any accumulated debris, and the conveying pipeline is cleared of any blockages.
- Startup Sequence: The system is started by activating the air supply to the conveying pipeline. The dust collection hopper begins to collect larger particles as the air flow is established. The gravity separator starts functioning as the air stream passes through, separating fine dust from the air.
- Normal Operation: During normal operation, the system continuously removes dust from the air stream and conveys the remaining powders to the designated discharge point. The air flow rate and pressure are maintained at optimal levels to ensure efficient transport. The dust collection hopper is periodically monitored to prevent overflow, and the system's performance is checked regularly to ensure it meets the required standards.
- Shutdown Procedure: When the system is to be shut down, the air supply is first turned off to prevent the backflow of powders. The dust collection hopper is emptied, and any remaining powders are discharged safely. The system is then cleaned and maintained as per the manufacturer's guidelines to ensure it is ready for the next operational cycle.
Key Advantages and Applications
Gravity dust removal powder conveying systems offer several advantages in industrial settings. These include low energy consumption, minimal maintenance requirements, and the ability to handle a wide range of powder types and particle sizes. The system is particularly suitable for applications in cement, chemical, food, and pharmaceutical industries, where the removal of fine dust and the efficient transport of powders are critical to process efficiency and environmental compliance.
Conclusion
HeadPowder's gravity dust removal powder conveying systems are designed to provide reliable and efficient solutions for industrial dust and powder management. By understanding the operation process and working principles, users can optimize the system's performance and ensure its longevity. With a strong presence in Shandong, China, HeadPowder continues to deliver high-quality engineering solutions that meet the evolving needs of the industry.