Efficient and reliable material handling is a critical component in industrial processes, particularly in the management of fly ash—a byproduct of coal combustion. The transportation of fly ash requires specialized systems to ensure safety, efficiency, and environmental compliance. This article explores the principles underlying the purification and transport of fly ash, along with key working scene characteristics that define its application in industrial settings.
Core Principles of Fly Ash Material Handling
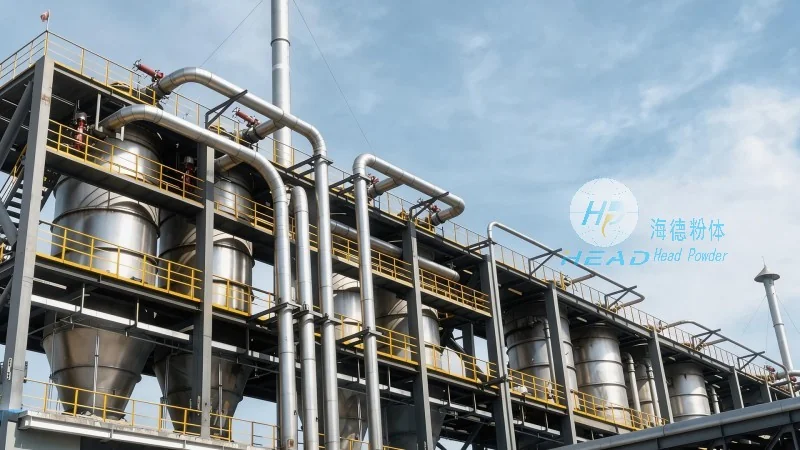
The process of purified fly ash material handling involves several fundamental principles designed to optimize performance and minimize risks. First, the system must ensure the separation of impurities from the fly ash stream, which is crucial for maintaining the quality of the material and preventing equipment damage. Advanced filtration and separation technologies are employed to achieve this, such as cyclone separators, electrostatic precipitators, and bag filters. These technologies effectively remove particulate matter and other contaminants, resulting in a cleaner, more consistent fly ash product.
Second, the handling system must prioritize safety and environmental protection. Fly ash, while generally non-toxic, can pose health risks if not handled properly, particularly due to its fine particle size. The design of the handling system includes features like enclosed conveying lines, dust collection systems, and explosion-proof components to mitigate these risks. Additionally, the system is engineered to minimize emissions and comply with environmental regulations, ensuring that the operation is sustainable and responsible.
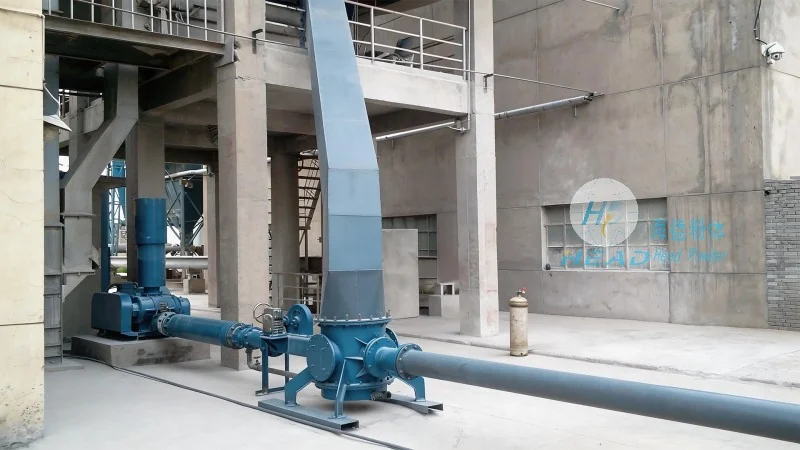
Third, efficiency and cost-effectiveness are key considerations in material handling. The system must balance performance with operational costs, including energy consumption, maintenance requirements, and downtime. Advanced control systems and automation are integrated to optimize the flow of material, reduce energy usage, and extend the lifespan of equipment. This approach ensures that the handling process is both economical and sustainable over the long term.
Working Scene Characteristics of Fly Ash Material Handling
The working scene characteristics of fly ash material handling vary significantly based on the specific industrial application and the scale of operation. In power plants, for example, the handling system is typically integrated with the boiler and ash handling infrastructure, requiring high-capacity conveying lines to transport large volumes of fly ash from the boiler to storage or disposal facilities. The system must be designed to handle high temperatures and abrasive materials, as fly ash can be hot and contain hard particles that can wear down equipment.
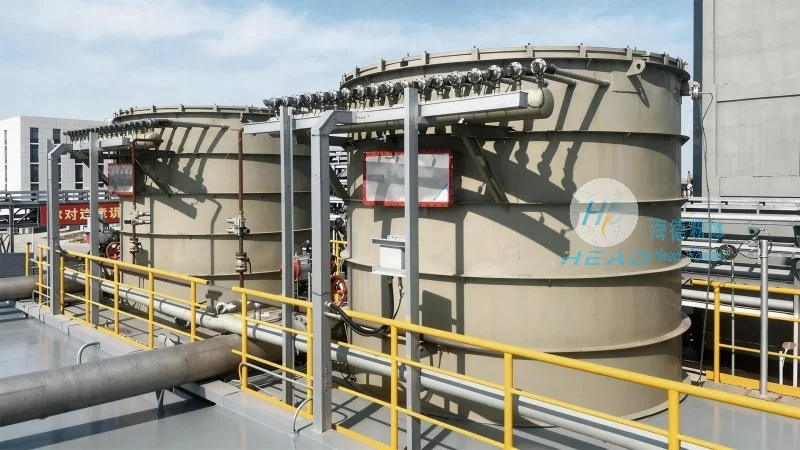
In cement and concrete production, fly ash is often used as a supplementary cementitious material (SCM), and the handling system must ensure that the material is delivered to the mixing plant in a consistent and controlled manner. This may involve blending the fly ash with other raw materials or storing it in silos before use. The system must also maintain the quality of the fly ash, as variations in composition can affect the performance of the final product.
In waste management and recycling facilities, the handling of fly ash may involve processing it for reuse or disposal. The system may include sorting and separation equipment to extract valuable components from the ash, such as metals or glass. This requires a more complex handling process, with multiple stages of material processing and transportation. The working scene in these facilities is often characterized by high volumes of material and the need for precise control to prevent contamination or loss of valuable resources.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of specialized engineering solutions for fly ash material handling and purification. With a focus on innovation and customer-centric design, the company has developed advanced systems that meet the diverse needs of industrial clients. HeadPowder's expertise lies in integrating cutting-edge technologies, such as high-efficiency filtration, automated control systems, and robust conveying equipment, to deliver reliable and efficient fly ash handling solutions.
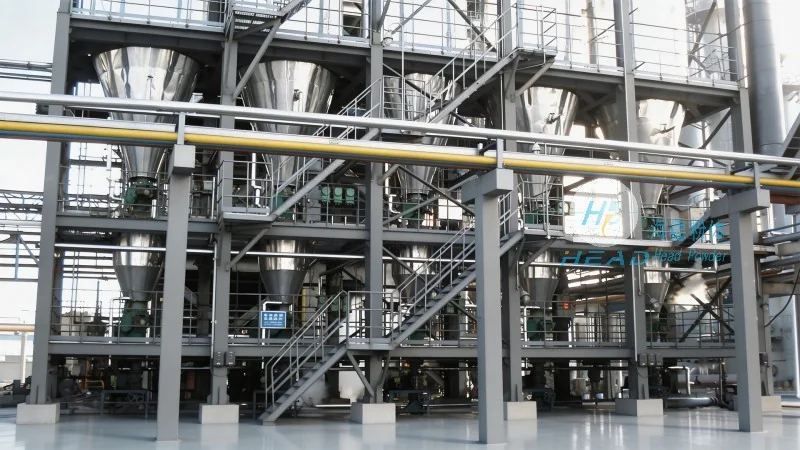
HeadPowder operates from its headquarters in Shandong, China, and serves clients across various industries, including power generation, cement production, and waste management. The company's commitment to quality and sustainability is reflected in its products, which are designed to minimize environmental impact while maximizing operational efficiency. By leveraging years of experience and continuous research, HeadPowder provides tailored solutions that address the unique challenges of each client's application.
The company's team of engineers and technicians work closely with clients to understand their specific requirements and develop customized systems that meet their needs. This collaborative approach ensures that the final solution is not only effective but also cost-effective and sustainable. HeadPowder's reputation for excellence in the industry is built on its ability to deliver high-quality products and services that enhance the performance and reliability of fly ash handling operations.




