For industries dealing with corn cob material handling, efficient and reliable transportation is crucial. The corn cob pneumatic conveying system offers a modern solution that enhances productivity while ensuring safety and minimal maintenance. This system is designed to handle the unique characteristics of corn cob, such as its bulk density and abrasive properties, making it an ideal choice for various processing applications.
HeadPowder Engineering: Your Trusted Partner in Material Handling
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized material handling solutions. With years of experience in the industry, HeadPowder has established itself as a trusted name in designing and implementing efficient conveying systems. The company’s expertise lies in understanding the specific needs of clients and tailoring solutions that meet their operational requirements. Based in Shandong, China, HeadPowder leverages local manufacturing capabilities and global technical expertise to deliver high-quality equipment and services.
Pneumatic Conveying Technology for Corn Cob Handling
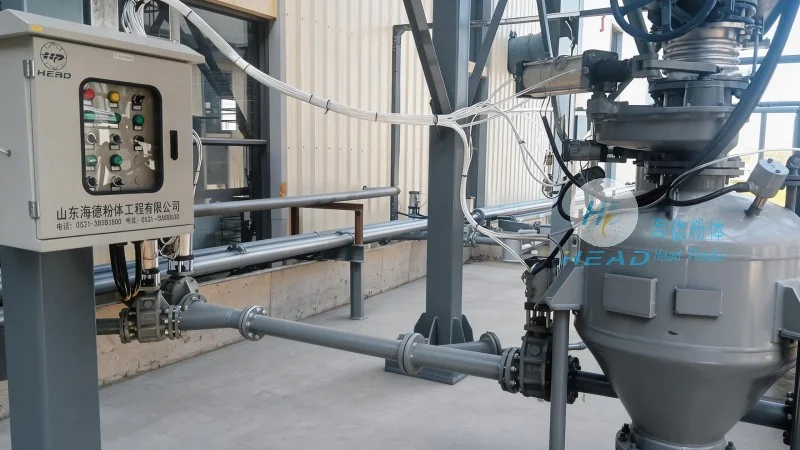
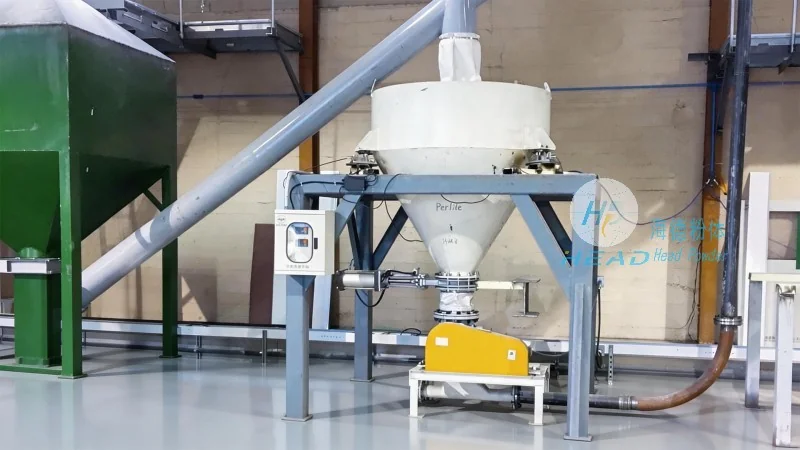
The core of the corn cob pneumatic conveying system is the use of air to transport material through a pipeline network. This technology eliminates the need for traditional mechanical conveyors, reducing wear and tear on equipment and minimizing the risk of material contamination. The system operates by creating a pressure differential that propels the corn cob particles through the pipeline. Key components include the hopper, air compressor, and conveying line, each designed to work in harmony to ensure smooth and continuous material flow. The system is capable of handling large volumes of corn cob while maintaining consistent flow rates, making it suitable for both small-scale and large-scale operations.
Advantages of Implementing a Corn Cob Pneumatic Conveying System
Adopting a corn cob pneumatic conveying system brings numerous benefits to industrial operations. First, it significantly improves operational efficiency by reducing downtime caused by maintenance and equipment failure. The system’s ability to handle abrasive materials without excessive wear extends the lifespan of components, leading to lower long-term costs. Additionally, the enclosed pipeline design minimizes dust emissions, contributing to a safer working environment and compliance with environmental regulations. Another advantage is the flexibility of the system, which can be easily scaled or modified to accommodate changes in production volume or material characteristics. This adaptability makes it a cost-effective solution for evolving business needs.
Customization and Integration Services by HeadPowder
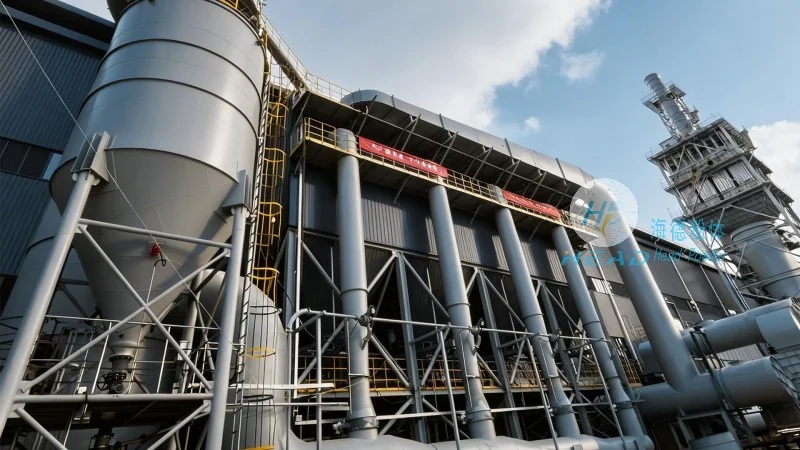
HeadPowder understands that each corn cob processing facility has unique requirements. Therefore, the company offers comprehensive customization and integration services to ensure the system meets specific operational needs. From initial consultation and system design to installation and commissioning, HeadPowder’s team of experts works closely with clients to develop tailored solutions. The company’s engineers use advanced simulation tools to model the conveying system, optimizing parameters such as air pressure, pipeline diameter, and material flow rate before implementation. This approach ensures that the final system is efficient, reliable, and cost-effective. Furthermore, HeadPowder provides ongoing support and maintenance services to keep the system operating at peak performance, minimizing disruptions and maximizing productivity.
Conclusion: Enhancing Efficiency with Corn Cob Pneumatic Conveying
For businesses in the corn processing industry, investing in a corn cob pneumatic conveying system from HeadPowder Engineering is a strategic decision that enhances operational efficiency and reduces costs. The system’s advanced technology and robust design ensure reliable material handling, while HeadPowder’s expertise guarantees a customized solution that meets specific needs. By choosing HeadPowder, companies can improve their overall productivity, maintain a safe working environment, and stay competitive in the market. With a strong presence in Shandong, China, HeadPowder continues to deliver high-quality material handling solutions that meet the evolving demands of the industry.




